


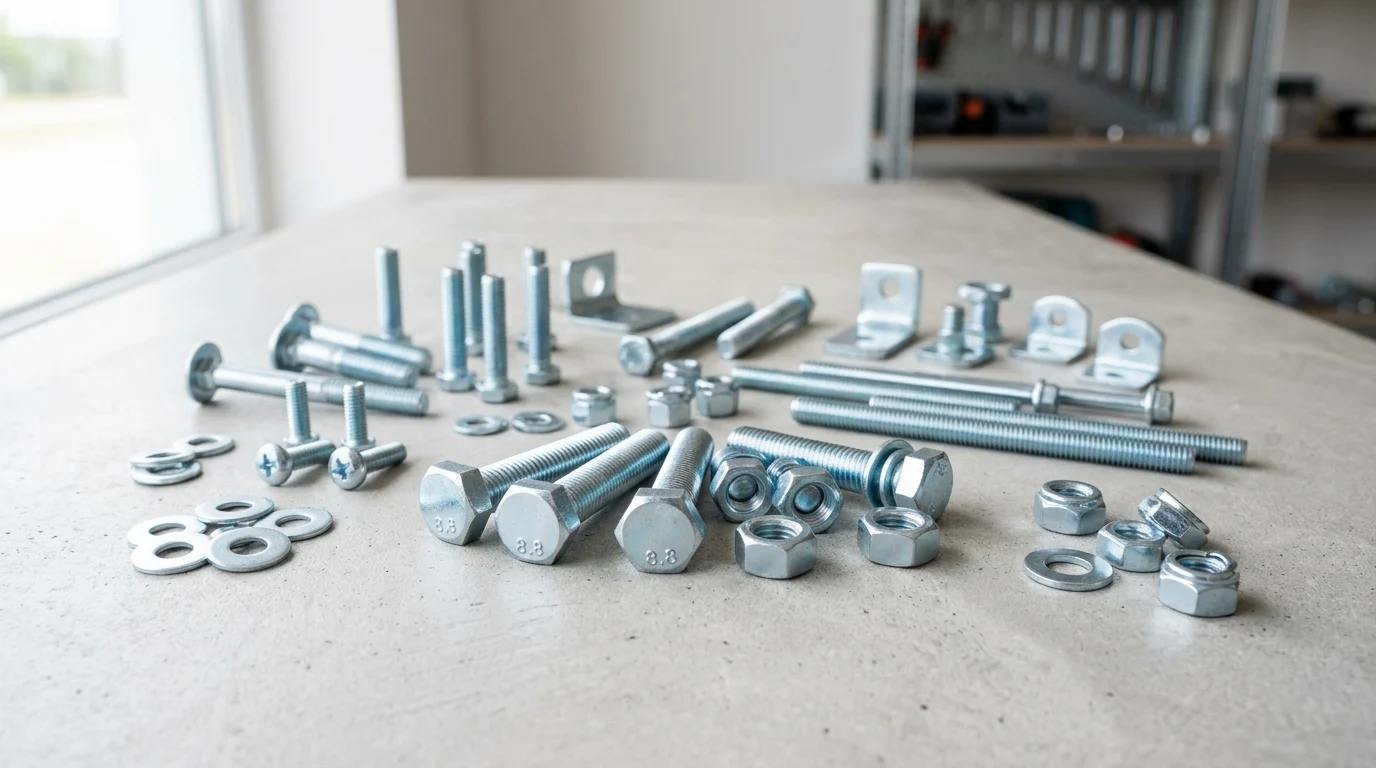
Industrial fasteners and metal components often fail long before the machine or structure they support, especially when moisture, chemicals, and temperature swings accelerate corrosion. Zinc-plated hardware gives engineers a practical way to protect carbon steel parts without the cost of stainless steel or specialized alloys. By combining a thin electroplated zinc layer with chromate conversion coatings, these parts can improve service life, maintain assembly integrity, and meet modern compliance expectations. This article explains how zinc plating works, why coating thickness and salt spray results matter, and what design teams should specify to avoid thread-fit issues, hydrogen embrittlement, and premature corrosion in demanding industrial applications.
How Zinc Plated Hardware Improves Corrosion Resistance
Industrial applications expose mechanical assemblies to moisture, chemicals, and varying temperatures, making corrosion mitigation a critical engineering priority. Utilizing zinc-plated fasteners and components provides a highly effective, cost-efficient barrier against environmental degradation. By applying a protective zinc layer to susceptible carbon steel substrates, manufacturers can significantly extend the lifecycle of machinery, construction components, and electrical enclosures. This approach balances performance and affordability, ensuring structural integrity across diverse industrial environments.
Zinc Plating Basics for Fasteners
The process of zinc plating involves electrodepositing a thin, uniform layer of zinc onto a metal substrate. For industrial fasteners and components manufactured from globally recognized materials like 1045/C45 steel or Q235/A36 steel, this coating typically ranges from 5 to 25 microns in thickness. The electroplating method ensures excellent adhesion and a consistent surface finish across complex geometries, including threads and recessed drive types. Although the coating is relatively thin, engineers must account for thread-fit allowances; precision assemblies may require oversize taps or thread-forming screws to accommodate the added material and prevent binding during installation.
For high-strength fasteners exceeding 32 HRC (Rockwell Hardness), the electroplating process introduces the risk of hydrogen embrittlement. To prevent catastrophic brittle failure, these components must undergo a time-sensitive post-plating baking process. This baking generally occurs at 190°C to 220°C for 4 to 24 hours and is often required to begin within one hour of plating. However, engineers should note that exact time windows, temperatures, and durations vary by specification (such as ASTM F1941 or ISO 4042) and the specific fastener strength class. Suppliers must be explicitly warned that delayed or improper baking is largely ineffective at outgassing trapped hydrogen before parts are deployed in structural applications.
Key Corrosion Protection Mechanisms
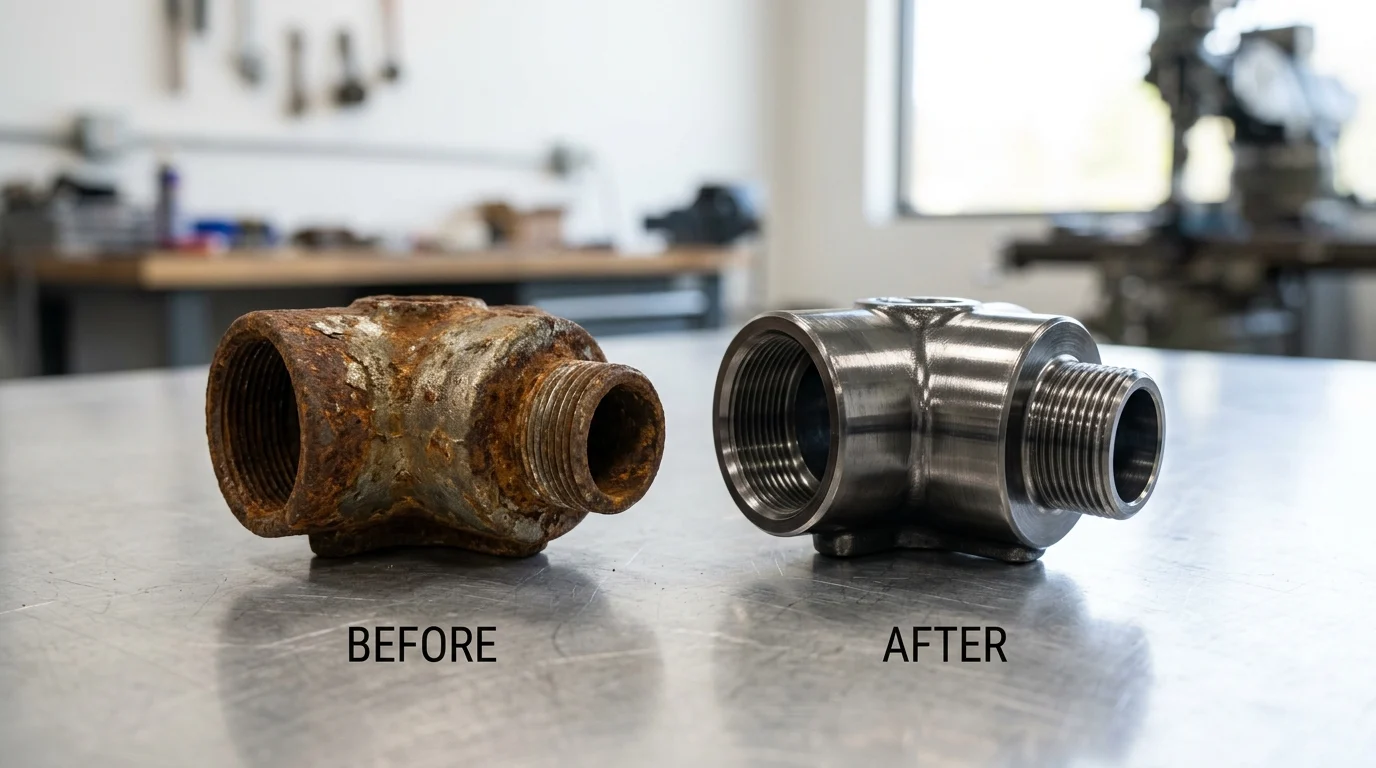
The primary mechanism driving this protection is galvanic corrosion resistance. Zinc acts as a sacrificial anode, meaning it will preferentially oxidize when exposed to corrosive elements, protecting the underlying steel even if the coating is lightly scratched or marred during assembly. Furthermore, zinc plating is almost always paired with a secondary chromate conversion coating, available in clear, yellow, olive drab, or black finishes. Modern industrial buyers must note that RoHS and REACH regulations heavily restrict traditional hexavalent (Cr6+) chromates, making compliant trivalent (Cr3+) finishes the standard for new designs.
A standard clear zinc finish might withstand 24 to 48 hours in a neutral salt spray test before the onset of white rust (zinc corrosion) appears, whereas heavy yellow zinc chromate can push that threshold past 96 hours. Crucially, these figures are not fixed universal benchmarks; results depend heavily on ASTM B117 testing parameters, substrate preparation, and the specific chromate chemistry applied. It is also critical to distinguish white rust from red rust (substrate failure), as specification errors often arise from conflating the two failure modes. This layered approach offers robust anti-corrosion performance tailored to the specific environmental demands of the application.
Comparing Zinc Plated Hardware With Other Options
When specifying fasteners and structural components, engineers must weigh the benefits of zinc-coated components against alternative materials and surface treatments. While plain carbon steel offers high tensile strength, its rapid oxidation makes it unsuitable for exposed applications. Zinc plating strikes an optimal balance between affordability, mechanical strength, and environmental resistance, but it is important to benchmark it against other common industrial options.
Performance and Specification Factors
Evaluating coatings requires looking at coating thickness, cost multipliers, and expected longevity. Zinc electroplating is highly favored because it adds minimal thickness, preserving the thread pitch on precision CNC hardware.
| Material / Coating | Typical Thickness | Salt Spray Resistance | Relative Cost |
|---|---|---|---|
| Zinc Plated Carbon Steel | 5 - 15 microns | 48 - 96 hours (White Rust) | Low |
| Hot-Dip Galvanized Steel | 45 - 85 microns | 500+ hours (Red Rust) | Medium |
| 304 Stainless Steel | N/A (Solid) | 1000+ hours (Red Rust) | High |
| Black Oxide | < 2 microns | < 12 hours (Red Rust) | Low |
Note: The relative costs provided are general rankings; actual costs fluctuate significantly based on production volume, geographic region, and raw-material market volatility.
As the table illustrates, zinc plating offers a massive upgrade over black oxide for a similar price point, though it cannot match the extreme baseline of solid stainless steel. Another critical specification factor is the torque-tension relationship during installation. Zinc plating alters the friction coefficient of the fastener threads compared to bare steel. Without proper lubrication or topcoats, zinc-plated threads typically exhibit a friction coefficient between 0.15 and 0.25. Engineers must adjust their torque specifications accordingly to achieve the correct clamping force and prevent thread galling, especially when automated assembly tools are utilized.
Limitations in Abrasion and Harsh Environments
Despite its versatility, zinc electroplating has distinct operational limits. Because the protective layer is relatively thin, environments with heavy mechanical abrasion will quickly wear down the zinc, exposing the bare steel beneath. Additionally, zinc coatings generally begin to degrade rapidly at continuous operating temperatures exceeding approximately 200°C (392°F), depending on the specific chromate conversion layer used.
In highly acidic environments or marine settings with constant chloride exposure, standard zinc plating will succumb to white rust quickly. In such harsh conditions, engineers must pivot to thicker hot-dip galvanizing, organic zinc-flake coatings, or pure stainless steel alloys to guarantee long-term structural integrity.
How to Specify, Source, and Validate Zinc Plated Hardware
Transitioning from the engineering design phase to mass production requires a rigorous approach to specification and sourcing. Procuring these treated components demands clear communication regarding coating thickness, post-plating treatments, and mechanical tolerances. Instead of relying on generic quality claims, buyers should mandate concrete deliverables: requiring Certificates of Conformance (C of C) to standards like ASTM B633 or ISO 4042, requesting calibrated cross-section thickness reports, and demanding salt-spray test data specific to the applied chromate.
Procurement and Engineering Checklist
A robust procurement checklist should explicitly define the required standards for the
Key Takeaways
- Specify zinc coating thickness in the typical 5 to 25 micron range based on the application’s corrosion exposure and thread-fit tolerance.
- Use zinc plating on carbon steel parts such as 1045/C45 or Q235/A36 when a cost-effective sacrificial corrosion barrier is required.
- Require post-plating baking for high-strength fasteners above about 32 HRC to reduce hydrogen embrittlement risk before structural use.
- Choose trivalent chromate finishes for new designs to support RoHS and REACH compliance instead of restricted hexavalent chromates.
- Differentiate white rust from red rust in salt spray requirements because zinc corrosion and steel substrate failure indicate different performance stages.
- Account for plating buildup on threads and recessed geometries to prevent binding during installation in precision assemblies.
Frequently Asked Questions
What are zinc-plated hardware parts used for?
They are commonly used in industrial machinery, construction components, electrical enclosures, and general assemblies where carbon steel parts need cost-effective protection against moisture, chemicals, and temperature changes.
How thick is the zinc coating on industrial fasteners?
Typical electroplated zinc coatings range from about 5 to 25 microns, depending on the specification, part geometry, corrosion target, and thread-fit requirements.
Why does zinc plating protect steel from rust?
Zinc acts as a sacrificial anode, meaning it corrodes before the underlying steel. This helps protect the base metal even if the plated surface is lightly scratched during handling or assembly.
What is the difference between white rust and red rust?
White rust is corrosion of the zinc coating, while red rust indicates corrosion of the steel substrate. Specifications should clearly state which failure mode is being measured.
Do high-strength zinc-plated fasteners need baking?
Yes. Fasteners above about 32 HRC may require post-plating baking, often at 190°C to 220°C for 4 to 24 hours, to reduce hydrogen embrittlement risk.