


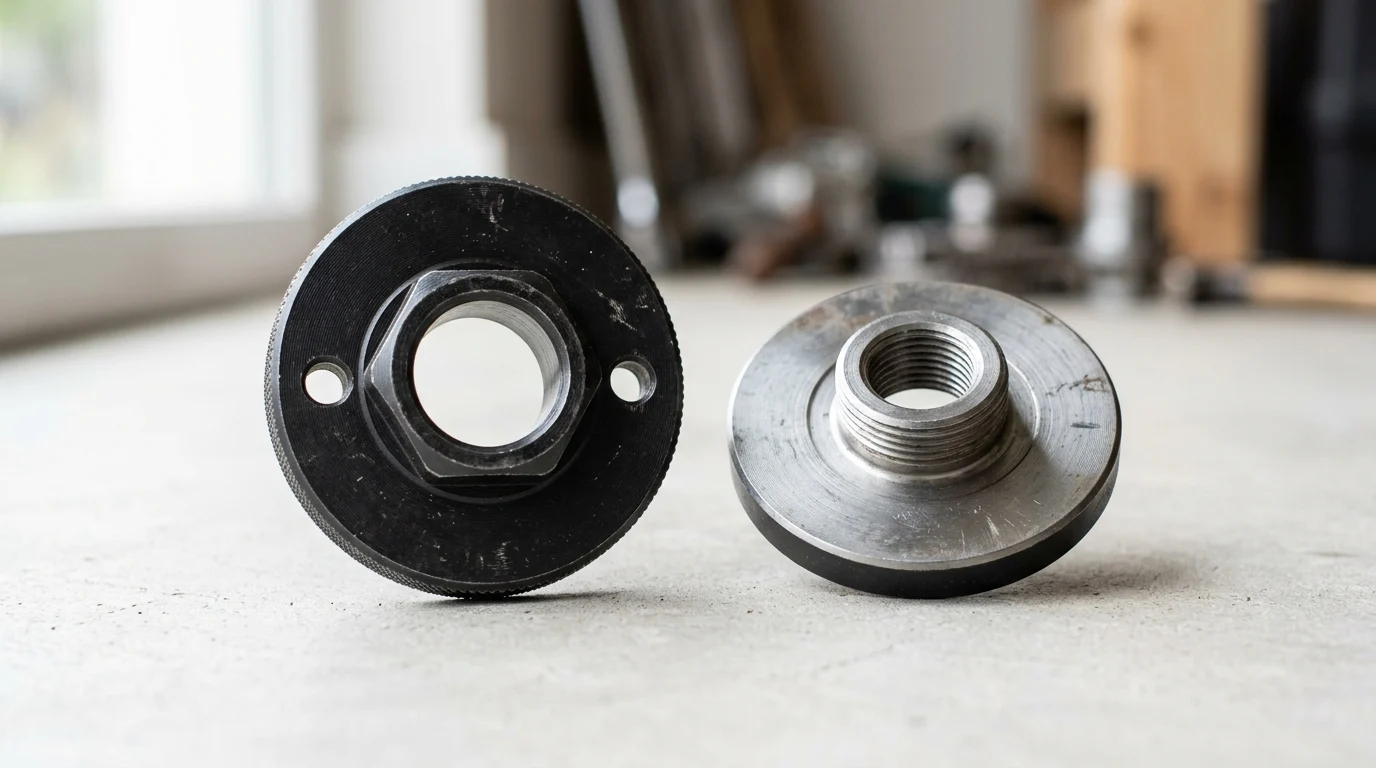
A grinder that feels rough in the hand is not always suffering from a weak motor or worn bearings. At speeds above 10,000 RPM, a small error at the disc interface can multiply into visible wobble, faster abrasive wear, and higher operator fatigue. Upper and lower pressure plates are the clamping components that decide whether the wheel runs true or transfers vibration into the spindle and housing. This article explains how plate geometry, runout tolerance, material quality, and mounting technique affect stability, safety, and tool life. It also outlines a practical diagnostic approach so technicians and buyers can separate flange-related vibration from disc imbalance, spindle wear, and maintenance issues.
Why Angle Grinder Pressure Plates Matter
Power tool manufacturers and heavy-duty fabricators often focus heavily on motor wattage, copper winding density, and bearing quality, overlooking the literal point of contact: the angle grinder upper and lower pressure plates](https://www.glinhardware.com/lower-pressure-plate-flange-outer-diameter-40-m10-slot-14-angle-grinder-model-100-changed-to-125-180m14-product/)s. If a grinder vibrates excessively during a standard cutting operation, these simple-looking flanges are frequently the primary culprits. At rotational speeds exceeding 10,000 RPM, even minor imbalances or microscopic asymmetries in the clamping mechanism amplify into significant hand-arm vibration. This is a critical performance bottleneck that degrades both tool lifespan and operator safety.
What Upper and Lower Pressure Plates Do
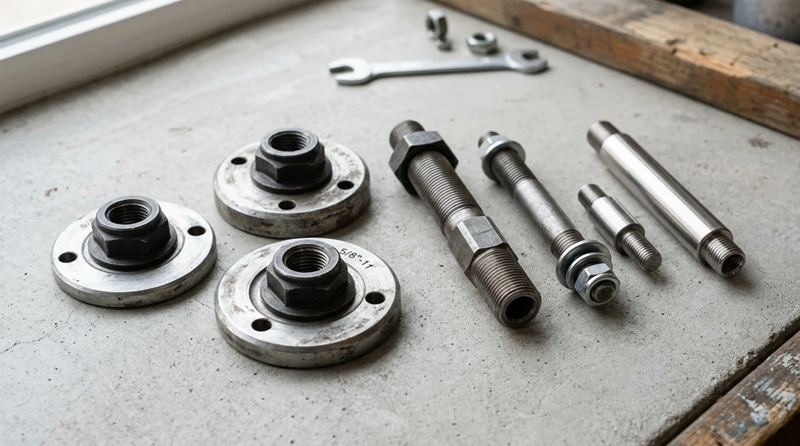
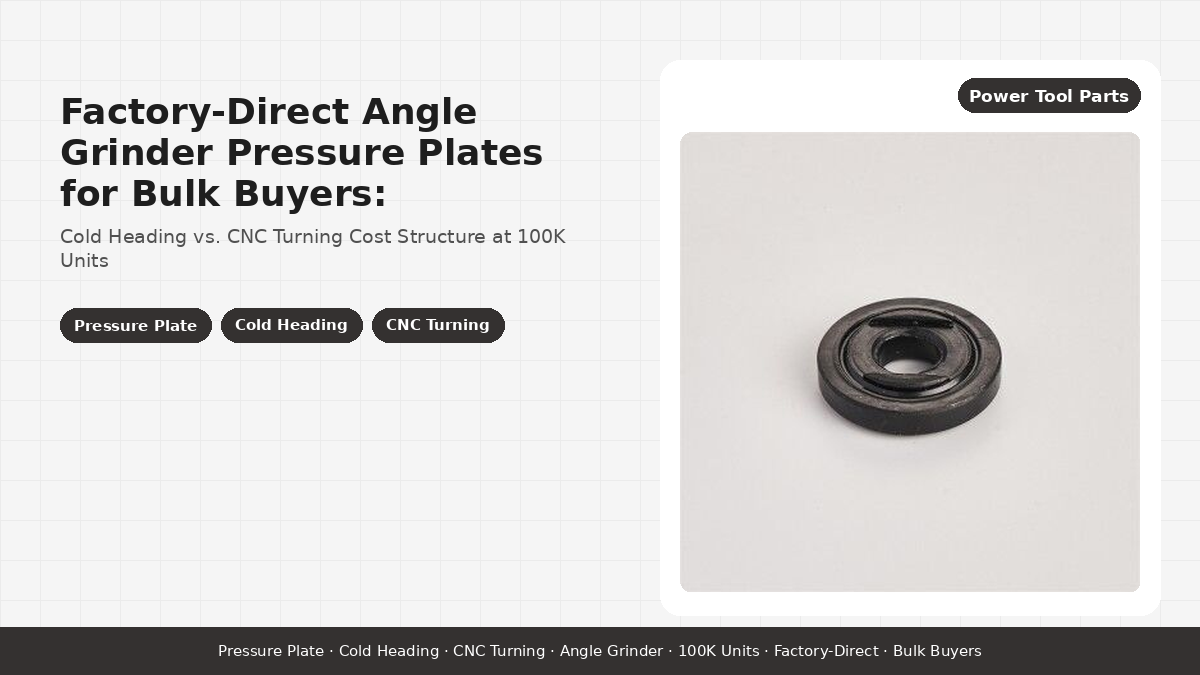
The lower pressure plate, commonly known as the inner flange, sits directly on the grinder's machined spindle. It provides a perfectly perpendicular seating plane relative to the spindle axis. The upper pressure plate—the lock nut—threads onto the spindle to apply uniform, concentric clamping force against the abrasive disc. By maintaining perfectly parallel mating surfaces under high torque, this interaction prevents the disc from deflecting radially or axially, acting as the primary mechanical mechanism to dampen and prevent vibration transfer. When sourcing flange sets, buyers must recognize that these are highly stressed, dynamic power transmission components that dictate the overall stability of the tool.
System Limitations and Dependencies: Precision plates are part of an interdependent mechanical system. It is critical to acknowledge that operator technique (such as overtightening or uneven seating), disc quality variation, and spindle wear are often more significant sources of vibration than plate precision. Upgrading to high-precision flanges cannot compensate for poor maintenance; it will only yield optimal results on well-maintained tools.
How Precision Affects Stability and Safety
Precision in these plates directly impacts operator safety and fatigue, aligning with standards like ISO 28927 for hand-held portable power tools. The vibration transmission path is direct: any irregularity at the plate transfers to the wheel, down the spindle, through the motor housing, and ultimately into the operator's hands. A standard, stamped plate might have a runout of 0.15 mm to 0.20 mm. At 11,000 RPM, this deviation creates a dangerous wobble that can shatter thin cutting discs and contribute to severe hand-arm vibration syndrome over extended shifts. High-precision forged and CNC-machined plates tighten that runout tolerance to strictly below 0.05 mm—an illustrative benchmark for professional-grade components.
Diagnostic Framework: When vibration issues arise, technicians should utilize a coherent troubleshooting process rather than blindly replacing parts. Symptom differentiation is key: spindle bearing wear typically presents as a continuous, high-frequency grinding noise accompanied by heat buildup, while inherent disc imbalance causes a rhythmic, low-frequency thumping. In contrast, plate runout manifests as a high-frequency, directional wobble that worsens immediately upon applying cutting pressure. Before suspecting the plates, operators must:
- Verify that the abrasive disc is undamaged and inherently balanced.
- Inspect the spindle and arbor for worn bearings or bending.
- Ensure proper mounting techniques were followed, including cleaning all mating surfaces of debris.
If these baseline factors are sound, the pressure plates are the likely source of the instability.
Key Specifications Buyers Should Compare
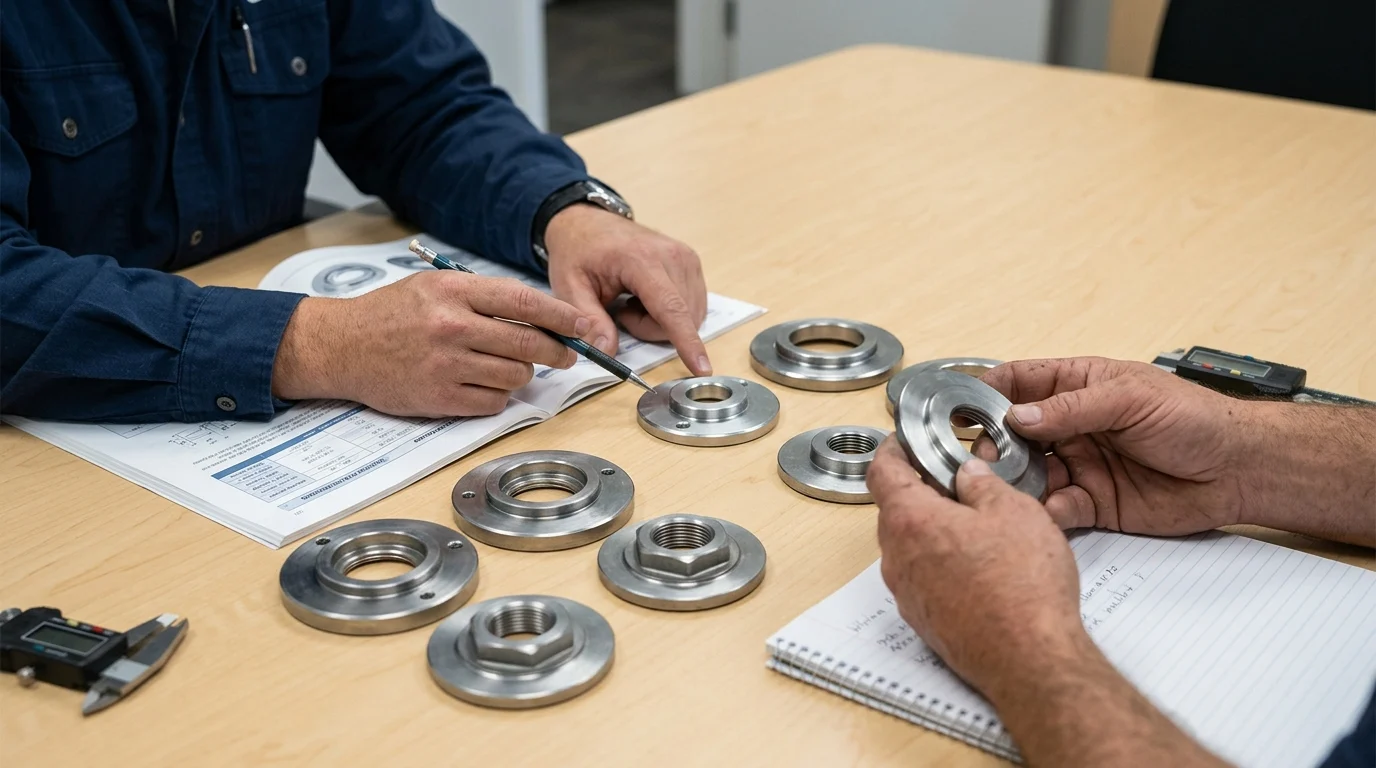
Procurement teams must examine the actual manufacturing specifications that directly influence rotational stability before finalizing a purchase order. When dealing with bulk industrial power tool accessories, understanding the underlying metallurgy, dimensional tolerances, and finishing processes is what separates a reliable, long-term OEM from an inconsistent supplier.
Material, Tolerance, and Surface Finish
Materials and surface finish are critical areas where quality varies. Standard pressure plates are frequently made from basic materials that can be too soft for heavy industrial use, leading to deformation under load, imbalance, and subsequent vibration. Industrial-grade plates utilize harder alloys and are heat-treated to achieve a core hardness that prevents the locking pins on a spanner wrench from stripping or deforming the pin holes prematurely. While specific hardness ranges and runout limits (detailed in the comparison table below) serve as illustrative industry benchmarks rather than universal laws, they provide a reliable baseline for professional applications. Surface finish is equally important; a proper black oxide coating or heavy zinc plating actively prevents rust from seizing the threads after wet cutting applications or exposure to high-humidity job sites.
Fit, Balance, and Compatibility
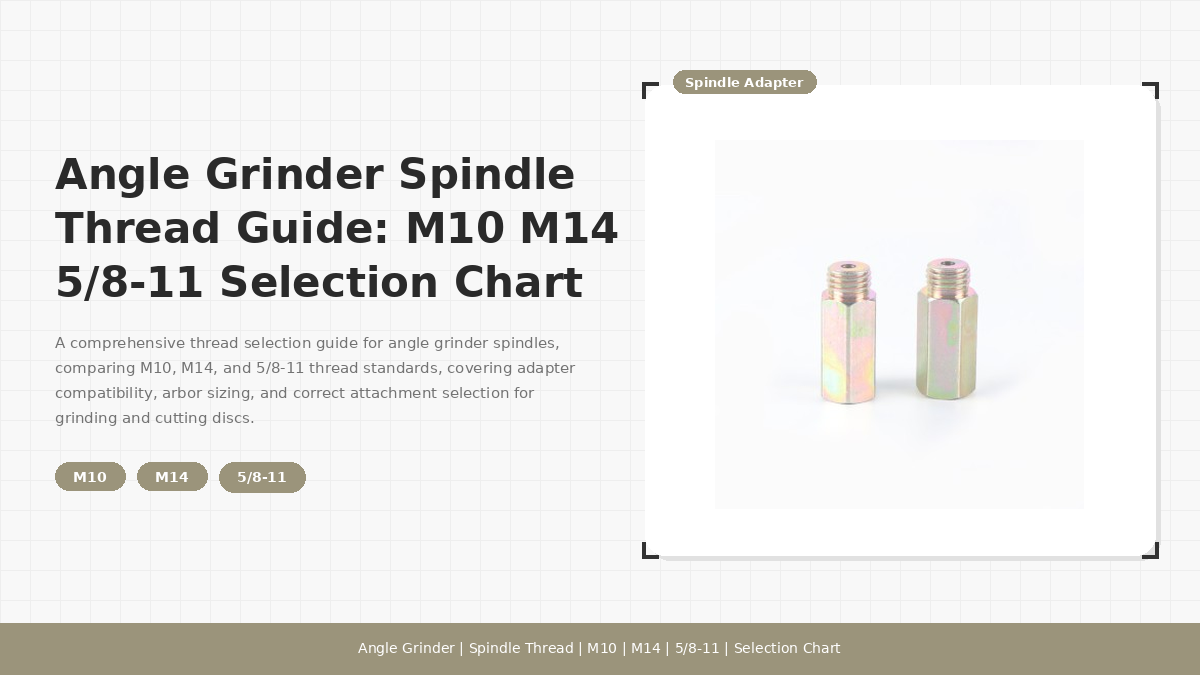
Fit and balance are fundamental to tool manufacturing. Whether matching an M14 thread for the European market or a 5/8"-11 thread for North American tools, the thread engagement must be flawless to prevent cross-threading under load. Proper installation technique is also vital; even precision plates will cause vibration if mounted incorrectly. Operators must ensure proper torque sequences, clean mating surfaces of all debris, and verify correct disc orientation. The following comparison table consolidates the tangible differences between standard and high-precision variants:
| Specification | Standard Pressure Plates | High-Precision CNC Plates |
|---|---|---|
| Base Material | Q235 / Powder Metallurgy | Forged 45# Steel / 40Cr |
| Material Hardness | HRC 20 - 25 | HRC 42 - 48 (Illustrative Benchmark) |
| Runout Tolerance | > 0.15 mm | < 0.05 mm (Illustrative Benchmark) |
| Thread Engagement | Loose / Prone to binding | Class 6H / Precision fit |
If the balance is even slightly off, the entire grinder vibrates. Achieving that critical < 0.05 mm runout requires advanced secondary machining, making specialized OEM sourcing for angle grinder flange nuts a necessary step for brands building professional-grade power tools.
How to Choose and Validate Suppliers
Finding a manufacturing supplier capable of consistently hitting the high-precision specifications necessary for vibration reduction requires careful validation. The difference between a mediocre supplier and a highly capable facility comes down to their capital equipment and quality control processes. When seeking a wholesale partner for heavy-duty grinder lock nuts, buyers must evaluate actual shop floor manufacturing capabilities rather than relying solely on marketing materials.
Quality Checks and Performance Testing
A robust quality management setup is essential during a facility audit. Rather than accepting vague claims of manufacturing excellence, procurement teams should request specific, actionable data.
Key Takeaways
- Inspect the abrasive disc, spindle, bearings, and mating surfaces before replacing pressure plates to avoid misdiagnosing the source of vibration.
- Use high-precision forged or CNC-machined plates when low runout is required, especially for grinders operating above 10,000 RPM.
- Treat upper and lower pressure plates as dynamic power transmission components, not simple accessories, because they directly affect disc stability.
- Aim for pressure plate runout below 0.05 mm for professional-grade performance, compared with the 0.15 mm to 0.20 mm often seen in stamped plates.
- Avoid overtightening and always clean the seating surfaces, because improper mounting can defeat the benefits of precision flanges.
Frequently Asked Questions
What do upper and lower pressure plates do in an angle grinder?
The lower plate seats on the spindle and supports the disc, while the upper plate locks it in place. Together, they keep the disc centered, parallel, and firmly clamped during high-speed rotation.
How does pressure plate precision reduce vibration?
High-precision plates minimize runout and keep clamping force concentric. This reduces disc wobble at speeds above 10,000 RPM, lowering vibration transfer through the spindle and tool housing.
What runout level is typical for professional-grade pressure plates?
Standard stamped plates may show about 0.15 mm to 0.20 mm of runout, while high-precision forged or CNC-machined plates can target below 0.05 mm for better stability.
Can precision flanges fix every angle grinder vibration problem?
No. Vibration can also come from damaged discs, worn spindle bearings, bent arbors, debris on mating surfaces, or poor mounting technique. Precision plates work best on well-maintained tools.
What vibration symptom suggests pressure plate runout?
Plate runout often causes a high-frequency, directional wobble that becomes worse as cutting pressure is applied. Bearing wear usually adds heat and grinding noise, while disc imbalance often feels like rhythmic thumping.