


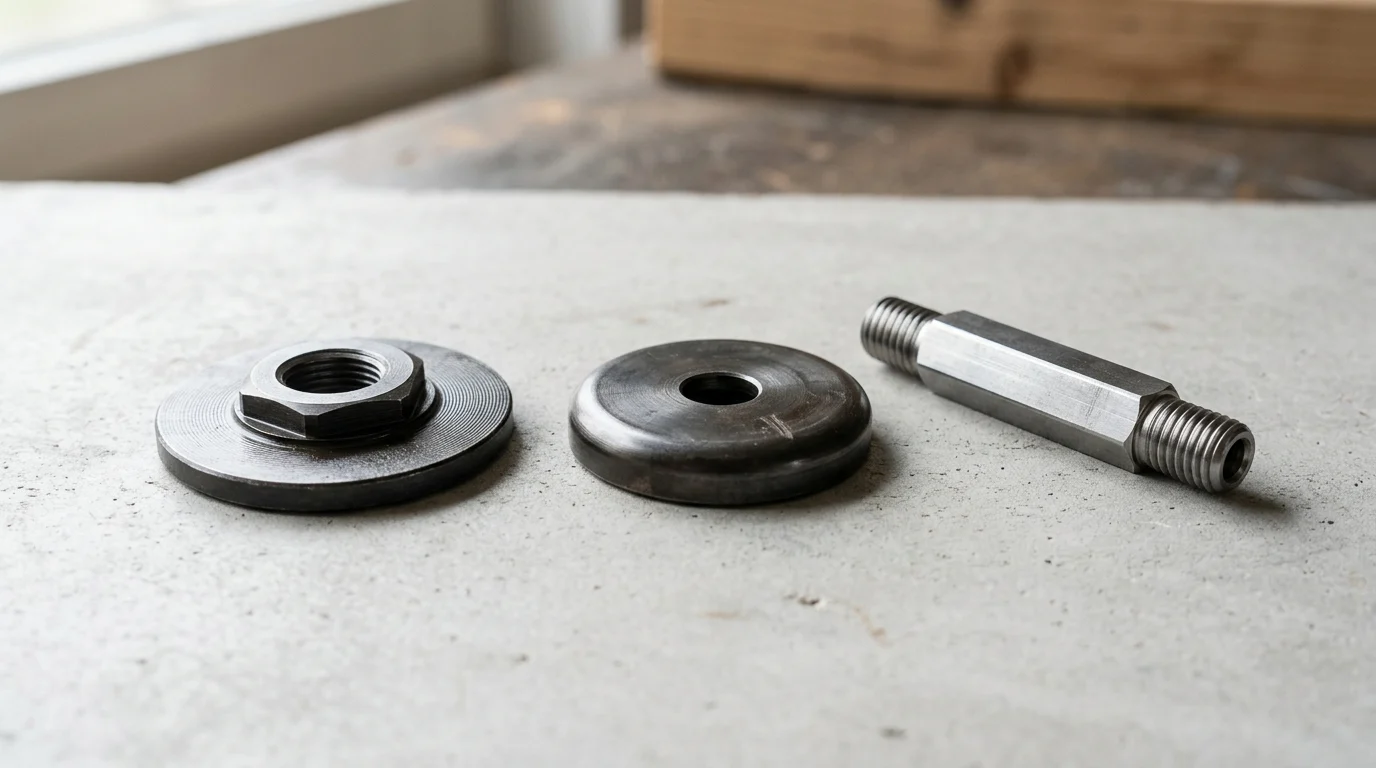
In power tool accessory manufacturing, quality control is not a back-end formality—it is a safety-critical discipline. Angle grinder pressure plates, drill conversion joints, polishing adapters, waxing accessories, and wool wheel components must withstand high-speed rotation, torque, heat, and repeated operator use. At 10,000 to 12,000 RPM, even a small dimensional error or imbalance can translate into vibration, fatigue, or failure. This article examines how manufacturers can use material verification, dimensional inspection, hardness control, AQL sampling, and process capability metrics to improve reliability, reduce defect rates, and build stronger procurement confidence in angle grinder part production.
Quality Control as a Strategic Advantage
For procurement managers and manufacturing engineers, the production of power tool accessories requires an uncompromising approach to quality assurance. Components such as angle grinder pressure plates, electric drill chucks, and wool wheel adapters operate under extreme dynamic stresses. With standard angle grinders reaching rotational speeds between 10,000 and 12,000 RPM, even microscopic deviations in mass distribution or structural integrity can lead to catastrophic failure.
Establishing a rigorous inspection framework is not merely a compliance exercise; it is a fundamental requirement for safety and operational longevity. For manufacturers, integrating these controls across the entire production lifecycle serves as a strategic differentiator in a highly competitive global market.
Business Value of Consistent Part Quality
Integrating advanced inspection protocols directly impacts the bottom line by minimizing material waste and mitigating warranty claims. Manufacturers producing Industrial Hardware who successfully reduce their defect rates—often aiming to drop from a historical industry average of 2.5% to below 0.5%, though exact targets vary by material and customer agreement—consistently report higher client retention.
Consistent part quality ensures that end-users experience less vibration, reducing operator fatigue and lowering the total cost of ownership through extended tool life. Furthermore, reliable production stabilizes the supply chain, allowing brands to forecast inventory and production schedules with greater accuracy.
Key Quality Control Terms and Definitions
Navigating this landscape requires familiarity with specific statistical and operational metrics. The Acceptable Quality Limit (AQL) defines the maximum number of defective units permitted in a batch before rejection, typically set at AQL 1.0 for major functional defects in power tool parts.
Additionally, the Process Capability Index (Cpk) measures a manufacturer's ability to produce parts within specified limits. A Cpk of 1.33 or higher is a common benchmark for precision metal components, indicating that process variation is well within tolerance parameters and the manufacturing line is highly stable.
Critical Specifications for Angle Grinder Parts
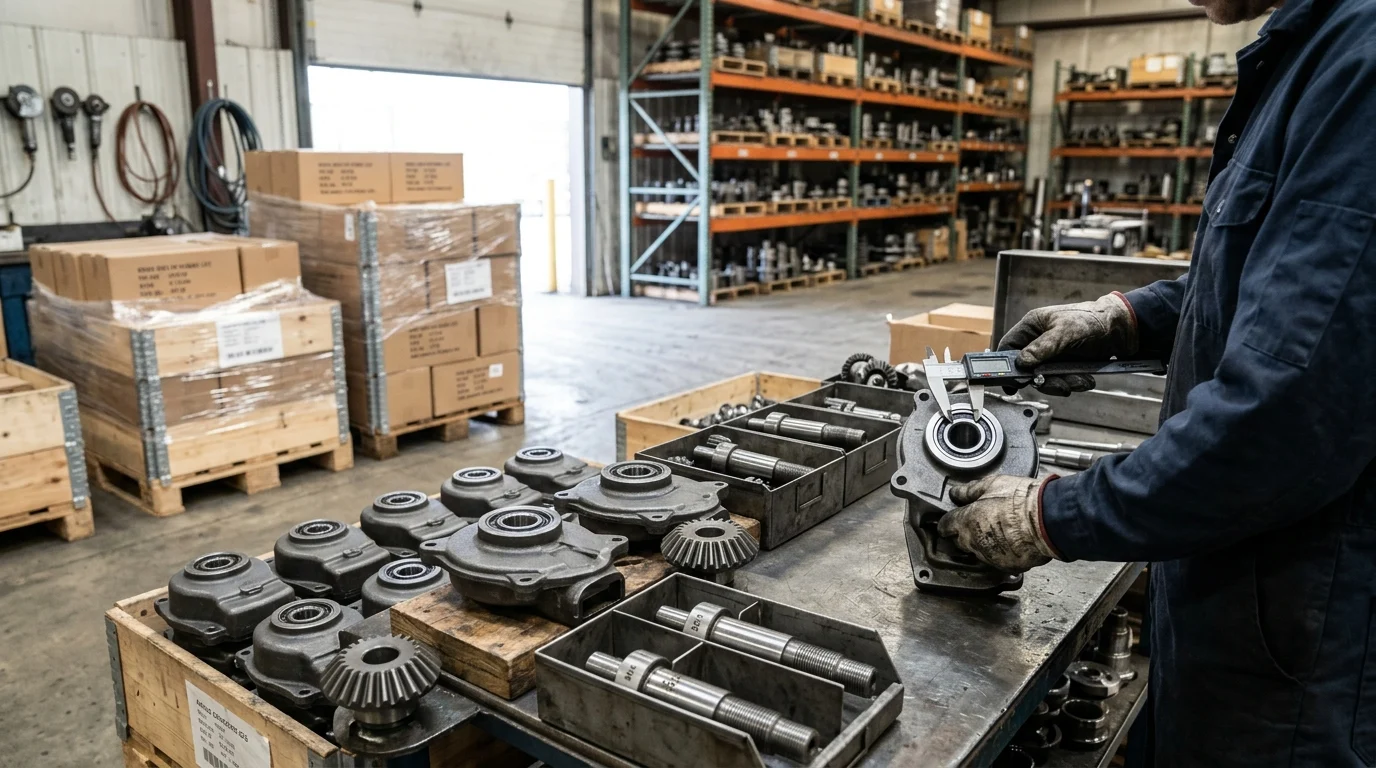
Defining precise specifications is the first step in ensuring that angle grinder and polishing accessories perform reliably under load. These specifications dictate everything from the raw material composition to the final dimensional tolerances, forming the baseline against which all inspections are measured.
Material Selection and Performance Requirements
The choice of raw material fundamentally determines the durability and safety of the final component. Standard angle grinder pressure plates—commonly produced for 100, 125, 150, 180, and 230 type machines—utilize materials such as 1045 carbon steel (often designated regionally as 45# steel), mild steel equivalents like Q235 (A3 steel), and high carbon steel.
For applications requiring complex geometries and high wear resistance, powder metallurgy is increasingly utilized. These materials are selected and processed to achieve a post-heat-treatment hardness range of HRC 42 to 48. This specific threshold provides an optimal balance between tensile strength and toughness, preventing brittle fractures during high-torque operation.
Dimensional and Functional Tolerances
Functional tolerances are strictly controlled to ensure concentricity and balance. A deviation of just 0.05 mm in the center bore of a grinding wheel pressure plate can induce severe vibrations at high rotational speeds.
Consequently, internal diameters are typically machined to a strict tolerance band of +/- 0.02 mm. Thread pitches on securing nuts and conversion joints must also adhere to Class 6H tolerances to guarantee a secure, non-slip fit, ensuring the abrasive wheel or polishing pad remains firmly locked in place.
Forged, Stamped, and Machined Parts Comparison
The manufacturing method heavily influences the final specifications and the required inspection checks.
| Manufacturing Method | Typical Tolerance (mm) | Material Strength | Cost Efficiency (High Volume) |
|---|---|---|---|
| Cold Forging | +/- 0.05 | Very High (Grain flow preserved) | Excellent |
| Precision Stamping | +/- 0.10 | Medium to High | Superior |
| CNC Machining | +/- 0.01 | High (Dependent on raw stock) | Moderate |
Selecting the right method depends on the specific Angle Grinder Accessories being produced. Forging offers the best structural integrity for load-bearing plates, while machining provides the extreme precision necessary for intricate conversion adapters.
Process Control from Forming to Finishing
The production route for high-performance hardware accessories follows a strict sequence: forging or stamping, followed by machining, heat treatment, surface treatment, and final testing. Maintaining process control across these sequential stages is vital, as an error in an early phase will compound, rendering subsequent finishing steps ineffective.
Forging, Stamping, and Machining Controls
Implementing robust controls during the initial forming and cutting phases ensures dimensional consistency. Facilities equipped with modern CNC Manufacturing infrastructure, such as fleets of fully automatic CNC machine tools and automatic tapping machines, can maintain tight process control.
These systems utilize continuous tool-wear monitoring and automated offset adjustments to prevent dimensional drift. By standardizing the machining environment, manufacturers ensure that every pressure plate or joint meets the exact programmed geometry before moving to the heat treatment phase.
Cold Heading and Automated Equipment Checks
For high-volume production of fasteners and structural joints, cold heading is highly efficient. Utilizing advanced machine forging technology and specialized cold heading models—including 19b, 24B, 28B, 136, 207, and 106—manufacturers can achieve production rates exceeding 120 parts per minute.
Automated equipment checks, such as in-line optical sensors and load monitors, are integrated into these machines. These sensors instantly detect short-feeds, excessive forming pressure, or malformed heads, automatically pausing production before defective batches are generated.
Common Process Risks and Prevention Methods
The most critical risks in this production route occur during heat treatment and surface finishing. Improper quenching can lead to micro-cracking or dimensional distortion exceeding 0.1 mm, rendering a precision Conversion Joint unusable.
Prevention methods include utilizing controlled-atmosphere furnaces to prevent surface decarburization and employing custom quenching fixtures. These fixtures hold parts securely to minimize warpage during rapid cooling, ensuring the components remain within acceptable tolerance limits for final surface plating or coating.
Inspection Standards by Part Type
Inspection protocols must be tailored to the specific function of the component. While a cosmetic polishing pad backing may require only basic dimensional checks, heavy-duty metal hardware demands rigorous metallurgical and mechanical testing to ensure compliance with international safety directives.
Load-Bearing Metal Parts
Components such as cutting machine pressure plates and electric circular saw pressure plates endure immense shear and clamping forces. Testing for these load-bearing parts focuses heavily on tensile strength and fatigue resistance.
Samples from each production batch are subjected to destructive testing, verifying that the yield strength meets baseline requirements—which often exceed 450 MPa depending on the specific alloy and heat treatment specified by the buyer. Magnetic particle inspection (MPI) or ultrasonic testing is also frequently deployed to detect subsurface flaws that could compromise the part under heavy operational loads.
Safety-Critical Components
High-speed rotational parts pose the greatest safety risk if they fail. Therefore, dynamic balancing and precise concentricity are the primary focus of Quality Inspection.
| Inspection Category | Testing Method | Acceptance Criteria |
|---|---|---|
| Dimensional | Coordinate Measuring Machine (CMM) | Within +/- 0.02 mm of CAD model |
| Metallurgical | Spectrometry & Hardness Testing | Matches specified alloy, HRC 42-48 |
| Dynamic Balance | Spin Testing / Balancer | Residual unbalance < 2.5 g-mm/kg |
Strict adherence to these inspection criteria guarantees that components will not disintegrate or cause dangerous kickback during operation, protecting the end-user and the equipment.
Traceability, Compliance, and Batch Records
Maintaining comprehensive batch records is a cornerstone of modern quality assurance. ISO 9001 compliant facilities implement traceability systems that link every finished part back to its original raw material melt number, the specific machine operator, and the heat treatment parameters.
These compliance records are typically retained for a minimum of 5 to 7 years. In the rare event of a field failure, this meticulous documentation ensures that the root cause can be swiftly identified and isolated, preventing widespread recalls and maintaining market trust.
Supplier Evaluation for Quality Control
For industrial buyers, partnering with the right manufacturer is as important as the product specifications themselves. Sourcing from established manufacturing clusters provides access to a mature industrial foundation and a comprehensive supply chain system capable of delivering mid-to-high-end precision forgings.
Manufacturing Capability and Inspection Systems
Evaluating a supplier requires a deep dive into both their production capacity and their inspection infrastructure. A reliable partner should offer integrated metal forming solutions, demonstrating ownership of the entire process from raw material processing to final testing.
Buyers should verify the presence of advanced testing instruments, such as optical comparators, profile projectors, and digital hardness testers, alongside high-capacity automated production lines. This dual capability ensures the supplier can handle both stringent precision requirements and large-scale volume demands.
Balancing Price, Tooling, and Quality Risk
Procurement teams must carefully weigh tooling investments against piece-price and quality risks. While dedicated cold forging dies may require an initial investment ranging from $3,000 to $5,000—though this varies widely based on part complexity and regional market rates—they dramatically lower the per-unit cost and improve dimensional consistency over high volumes.
Suppliers that mandate Minimum Order Quantities (MOQs) of 10,000 to 20,000 units for custom-tooled parts are typically structuring their production runs to ensure stable process control and adequate quality sampling, which ultimately protects the buyer from batch-to-batch variability.
Buyer Decision Criteria
Ultimately, the decision to onboard a new supplier hinges on a structured evaluation of their operational reliability. Audit criteria should always be scaled to match the buyer's specific risk profile and industry requirements. Procurement teams should utilize an actionable buyer checklist focusing on:
- Defect Rate Targets: A proven defect rate (e.g., less than 50 Parts Per Million), noting that acceptable PPM varies by component criticality and customer agreement.
- Lead Time Consistency: The ability to consistently meet agreed-upon delivery windows, such as 30 to 45-day lead times.
- System Transparency: Clear communication and documentation regarding their internal quality management systems.
- Process Validation: Rigorous on-site or third-party audits of the supplier's production route, specifically observing their forging, machining, and testing phases.
In conclusion, ensuring the reliability of angle grinder parts and related power tool accessories requires a comprehensive approach to manufacturing oversight. By defining strict material and dimensional specifications, enforcing process controls from forging to finishing, and rigorously evaluating supplier capabilities, brands can deliver safer, higher-performing tools to the market. Implementing these structured quality frameworks not only mitigates operational risks but also establishes a foundation for long-term supply chain success.
Key Takeaways
- Set clear inspection criteria for angle grinder parts because components operating at 10,000 to 12,000 RPM require tight control of balance, concentricity, hardness, and structural integrity.
- Use AQL 1.0 as a practical benchmark for major functional defects when evaluating batches of power tool accessories.
- Track process capability and aim for a Cpk of 1.33 or higher to confirm that precision metal parts are being produced consistently within tolerance.
- Select materials such as 1045 carbon steel, Q235, high carbon steel, or powder metallurgy based on the required balance of strength, wear resistance, toughness, and cost.
- Verify heat-treated components against an HRC 42 to 48 hardness range to reduce brittle fracture risk while maintaining durability under high-torque operation.
- Reducing defect rates from about 2.5% toward below 0.5% can lower waste, warranty claims, vibration issues, and customer complaints.
Frequently Asked Questions
Why is quality control critical for angle grinder parts?
Angle grinder parts often run at 10,000 to 12,000 RPM, so small defects in balance, hardness, or dimensions can cause vibration, premature wear, or unsafe failure. Rigorous inspection helps protect users and improves product reliability.
What defect rate should manufacturers target for power tool accessories?
Many manufacturers aim to reduce defect rates from around 2.5% to below 0.5%, depending on material, application, and customer requirements. Lower defect rates reduce waste, warranty claims, and supply chain disruption.
What does AQL mean in power tool part inspection?
AQL stands for Acceptable Quality Limit. It defines the maximum number of defective units allowed in a batch before rejection. For major functional defects in power tool parts, AQL 1.0 is commonly used.
What Cpk value indicates a stable manufacturing process?
For precision metal components, a Cpk of 1.33 or higher is commonly considered a strong benchmark. It shows that the process can consistently produce parts within specified tolerance limits.
Which materials are commonly used for angle grinder pressure plates?
Common materials include 1045 carbon steel, Q235 mild steel, high carbon steel, and powder metallurgy materials for more complex or wear-resistant parts. Material selection depends on strength, toughness, cost, and application requirements.