


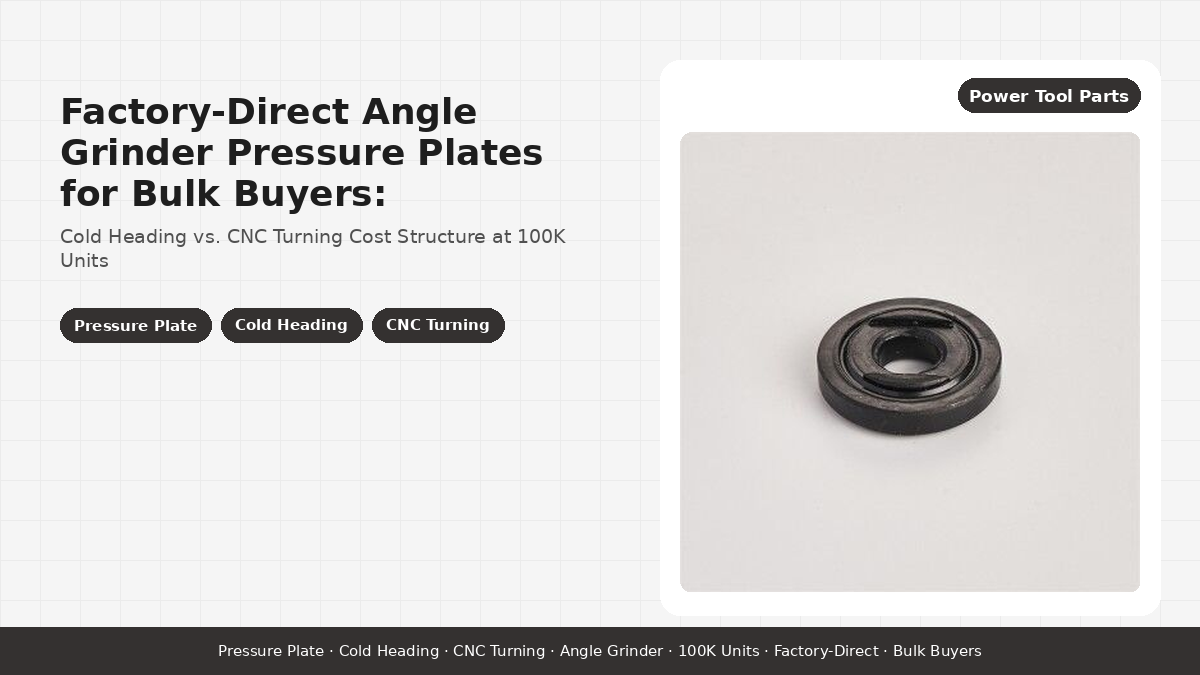
Private-Label Cutting Machine Pressure Plate Development: One-Stop Brand-Own Power Tool Line from Forging to Surface Treatment
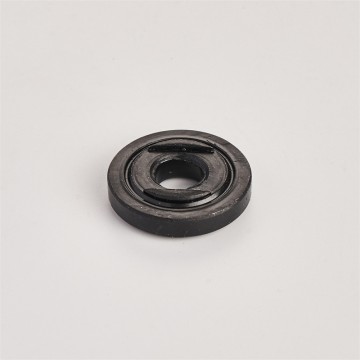
A product manager at a North American power tool brand owner sat across from three Chinese OEM suppliers at a Canton Fair booth in October 2025. Supplier A quoted $0.42 per cutting machine pressure plate with 8-week lead time, but the factory's forging dies could not match the brand owner's 76mm outer diameter specification without a $18,000 custom die setup. Supplier B quoted $0.55 per plate with 6-week lead time and had the forging dies in stock, but the surface treatment was outsourced to a separate plating shop 40km away, adding 2 weeks of logistics risk to every shipment. Supplier C quoted $0.48 per plate with 7-week lead time, had the forging dies in stock, AND ran the zinc plating line in-house — but the badging capability was limited to a single Pantone color and the carton design required 3-week turnaround through a third-party graphic design vendor. This guide is the field-tested version of how a power tool brand owner should evaluate the "one-stop" OEM claim — and what to verify on-site before committing to the private-label program.
This guide is built around the OEM development workflow used by power tool brand owners launching private-label cutting machine pressure plate programs with vertically integrated Chinese factories like Yuyao Guling Hardware Co., Ltd. — a precision forging and metal forming manufacturer operating 40+ fully automatic CNC machines and cold-heading lines, with in-house heat treatment, CNC machining, zinc plating, and badging / packaging capability for a true forging-to-surface-treatment OEM line.
The "one-stop" claim: 3 supplier types that brand owners actually meet
The "one-stop forging to surface treatment" claim is the most common OEM marketing language in the power tool accessory industry, but it covers three very different supplier types that brand owners actually meet in their RFQ pool. Supplier Type I is the vertically integrated OEM — the factory owns the forging dies, the heat treatment furnace, the CNC machining center, the plating line, and the badging / packaging equipment, with all five capabilities under one roof and one quality management system. Supplier Type II is the partially integrated OEM — the factory owns the forging dies and the CNC machining, but outsources the heat treatment and the surface treatment to separate vendors, typically within 50km of the main factory. Supplier Type III is the trading company with marketing claims of "one-stop" — the trading company has no actual production lines and subcontracts every step to different factories, adding 2-4 weeks of logistics and 1-2 layers of margin to the per-unit price.
The vertically integrated OEM (Type I) is the right partner for power tool brand owners launching a serious private-label program with annual volume above 5,000 units. The Type I OEM can compress the development timeline from 14-18 weeks to 10-14 weeks by running forging + machining + surface treatment in parallel (the forging sample can be machined while the heat treatment furnace is being prepared for the next batch). The Type I OEM can also resolve engineering issues faster because the forging die designer, the heat treatment engineer, the CNC machinist, and the plating chemist are all on the same engineering team and can troubleshoot in real time.
The partially integrated OEM (Type II) is acceptable for brand owners with annual volume 1,000-5,000 units who cannot find a Type I OEM with the right forging die inventory. The Type II OEM adds 2 weeks of logistics risk (heat treatment vendor delay, plating vendor delay) and 5-10% to the per-unit cost (subcontractor margin), but the engineering quality is typically acceptable if the OEM has long-term relationships with the outsourced vendors. The Type II OEM should be evaluated on the same 5-gate framework as the Type I OEM, but with extra scrutiny on the outsourced vendor audit (heat treatment furnace calibration records, plating line salt spray testing capability).
The trading company (Type III) should be excluded from any serious brand-owner private-label program. The Type III trading company cannot control the engineering quality, the lead time reliability, or the cost trajectory because every step is subcontracted to a different factory with different priorities. The Type III company's "one-stop" claim is marketing language that obscures the lack of actual production lines. The brand owner should run the 4-question triage in week 1 of the RFQ process to identify and exclude the Type III companies: (1) "Can you send factory audit photos dated within the last 90 days of your forging operation?" — Type III cannot; (2) "What is your in-house heat treatment furnace capacity?" — Type III says "outsourced"; (3) "Can you provide a sample of your in-house plating line?" — Type III sends a brochure photo; (4) "What is your badge tooling inventory?" — Type III says "we coordinate with our partner".
The 6-step OEM development workflow: from forging to surface treatment
The private-label cutting machine pressure plate development workflow is a 6-step engineering process that takes 10-14 weeks from RFQ approval to first article inspection at a vertically integrated OEM. Each step has a specific deliverable and a specific duration, and skipping any step typically causes a 2-4 week rework cycle later in the program. The 6 steps are documented below with typical duration and deliverable for each step, and the parallel vs sequential execution pattern that differentiates a vertically integrated OEM from a partially integrated OEM.
| Step | Activity | Duration (integrated) | Duration (non-integrated) | Deliverable |
|---|---|---|---|---|
| 1. Specification alignment + forging die design | Confirm plate dimensions, material grade, hardness range, thread spec, surface treatment | 2-3 weeks | 3-4 weeks | Signed technical specification sheet + forging die design drawing |
| 2. Forging sample fabrication + heat treatment | Forging die setup, sample forging, heat treatment per BS EN 10083-3 | 2-3 weeks (parallel) | 4-5 weeks (sequential) | Forged + heat-treated sample with hardness test certificate |
| 3. CNC machining to final tolerance | CNC turning + milling to dimensional tolerance per ISO 2768 | 1-2 weeks | 2-3 weeks | Machined sample with dimensional inspection report |
| 4. Surface treatment (plating) | Zinc plating ≥ 8μm / black oxide / nickel plating per BS EN ISO 1456 | 2-3 weeks (parallel with step 3) | 3-4 weeks (sequential + logistics) | Plated sample with salt spray test certificate per BS EN ISO 9227 |
| 5. FAT + badging + packaging sample | Dimensional + hardness + salt spray verification, badge artwork, color match, carton design | 1-2 weeks | 2-3 weeks | FAT report + pre-production sample with full brand-owner badging and packaging |
| 6. Production lot preparation | Production line scheduling, component pre-order, QC plan finalization | 2 weeks | 2-3 weeks | Production lot schedule with first-article trigger |
The parallel execution pattern is the key advantage of the vertically integrated OEM. In the non-integrated OEM (Type II), the forging sample must be sent to the outsourced heat treatment vendor (2-3 days logistics), then to the outsourced plating vendor (2-3 days logistics), and any rework causes the entire chain to restart. In the vertically integrated OEM (Type I), the forging sample can be moved to the in-house heat treatment furnace within hours, and any engineering issue can be resolved by the in-house engineering team without waiting for vendor response. The 4-week timeline savings is the operational difference between a Type I and Type II OEM, and it compounds across the entire private-label program lifecycle.
The FAT stage is the highest-leverage step in the workflow. It is where the brand owner verifies that the cutting machine pressure plate meets the dimensional specification (ISO 2768 tolerance grade), the hardness specification (HRC 35-45 per BS EN ISO 6508-1), and the corrosion specification (48-hour NSS per BS EN ISO 9227). The FAT should be witnessed on-site by the brand owner's engineering team or a third-party inspection agent, with measured values recorded against the specification and signed off by both parties. The FAT report becomes the baseline for the production lot acceptance and is the document the brand owner's quality team references during incoming-material inspection.
The badging and packaging stage is the second highest-leverage step. It is where the brand owner's identity is physically applied to the product. The badge artwork must match the brand's Pantone color reference (the OEM should have in-house Pantone color matching capability, not outsource to a graphic design vendor), the manual must be translated to the target market language (with native speaker verification), and the carton design must include the brand owner's logo, model number, and barcode. The pre-production sample with full badging and packaging should be reviewed by the brand owner's marketing team before the production lot is released.
Material and surface treatment: the 4 surface options for cutting machine pressure plates
Cutting machine pressure plates are available with four standard surface treatments, each addressing a different target market and warranty profile. The surface treatment selection is typically driven by the brand owner's target market (indoor industrial / outdoor construction / marine offshore / food-grade), the warranty commitment (90 days / 12 months / 24 months), and the per-unit cost target. The four surface treatments and their typical applications are summarized below.
| Surface treatment | Coating thickness | NSS rating | Application | Per-unit cost adder |
|---|---|---|---|---|
| Zinc plating (clear / yellow chromate) | Zn ≥ 8μm per BS EN ISO 1456 | 48-hour NSS | General industrial indoor / short-term outdoor use, 12-month warranty | Baseline (100%) |
| Black oxide coating | Thin conversion coating | 12-24 hour NSS | Indoor controlled storage applications, 6-month warranty | -15% (lower cost) |
| Electroless nickel plating | Ni ≥ 10μm | 240+ hour NSS | Marine / offshore / high-corrosion applications, 24-month warranty | +120-180% |
| Dacromet / zinc flake coating | Multi-layer flake | 480+ hour NSS | High-corrosion / chemical exposure applications, 36-month warranty | +200-300% |
The zinc plating with clear or yellow chromate passivation is the baseline surface treatment for power tool accessory private-label programs. The 48-hour NSS rating is adequate for general industrial indoor use and short-term outdoor exposure (3-12 months in a warehouse, on a retail shelf, or in a contractor's truck). The zinc plating cost is the baseline (100%), and the per-unit price adder for yellow chromate (vs clear chromate) is typically 5-10% for the supplementary corrosion resistance. The zinc plating thickness should be verified per BS EN ISO 1456 with an XRF coating thickness gauge at 3-5 measurement points per plate.
The black oxide coating is the cost-optimized surface treatment for indoor controlled storage applications where the corrosion exposure is minimal. The black oxide is a thin conversion coating that provides minimal corrosion protection (12-24 hour NSS) but gives the plate a matte black appearance that is preferred for some brand-owner aesthetics (typically power tool brands with a "professional black" product line). The black oxide cost is 15% below the zinc plating baseline, and the warranty commitment is typically 6 months.
The electroless nickel plating is the premium surface treatment for marine / offshore / high-corrosion applications where the 48-hour NSS is inadequate. The electroless nickel provides 240+ hour NSS rating and is suitable for coastal construction, offshore oil & gas, and marine applications where the plate is exposed to salt spray for extended periods. The electroless nickel cost is 120-180% above the zinc plating baseline, and the warranty commitment is typically 24 months. The electroless nickel thickness should be verified per ASTM B733 with an XRF coating thickness gauge.
The Dacromet / zinc flake coating is the high-end surface treatment for chemical exposure and high-corrosion applications where even the electroless nickel is inadequate. The Dacromet / zinc flake provides 480+ hour NSS rating and is suitable for chemical plant maintenance, offshore platform, and military / defense applications. The Dacromet cost is 200-300% above the zinc plating baseline, and the warranty commitment is typically 36 months. The Dacromet coating is a multi-layer flake structure that requires specialized application equipment and is typically only available at Tier I OEM facilities.
Private-label MOQ economics: 200-unit trial vs 1,000-unit launch vs 5,000-unit scale
The private-label MOQ economics for cutting machine pressure plates follow a stepped price curve where the per-unit price drops 15-20% from the 200-unit trial tier to the 1,000-unit launch tier, drops another 10-15% from 1,000 to 5,000 units, and stabilizes around 10,000 units. The price steps are driven by forging die setup amortization (the forging die cost is amortized across the order quantity), heat treatment furnace setup amortization (each heat treatment batch has a setup cost), CNC machining program setup amortization (each CNC program has a setup cost), and plating rack setup amortization (each plating rack has a setup cost). The table below summarizes the typical private-label MOQ economics.
| Order size | Typical per-unit price (76mm plate baseline) | Price step vs previous tier | Lead time | Application |
|---|---|---|---|---|
| 200-unit trial | Baseline (100%) | — | 10-12 weeks (integrated) / 14-16 weeks (non-integrated) | Pilot launch, retail test market |
| 1,000-unit launch | 80-85% of baseline | -15 to -20% | 10-12 weeks (integrated) | Regional launch, initial retail distribution |
| 5,000-unit scale | 68-75% of baseline | -10 to -15% | 12-14 weeks (integrated) | Multi-region launch, retail chain stocking |
| 10,000-unit+ national | 62-70% of baseline | -5 to -10% | 12-16 weeks (integrated) | National distribution, OEM supply contract |
The 200-unit trial order is the highest-risk order in the private-label program because it is where the forging die, the heat treatment, the CNC machining, the surface treatment, the FAT, the badging, and the packaging are validated for the first time. The 200-unit trial order should be priced as an investment in program qualification rather than as a per-unit commodity purchase. Brand owners who negotiate the 200-unit trial price down to commodity levels typically receive commodity-level engineering support, and the resulting 1,000-unit launch inherits the corner-cutting.
The 1,000-unit launch tier is the most common commercial order size for power tool brand owners with a single-region launch and a 6-12 month sales cycle. At 1,000 units, the per-unit price has compressed by 15-20% from the 200-unit trial, the lead time is still 10-12 weeks (at a vertically integrated OEM), and the OEM has typically stabilized the production line for the brand owner's specific configuration. The 1,000-unit launch tier is also where the brand owner should begin the second-source qualification (a parallel Chinese OEM with vertically integrated capability) to mitigate single-source supply chain risk.
The 5,000-unit scale tier is where the private-label program becomes a national-distributor relationship. At 5,000 units, the per-unit price has compressed by 25-30% from the 200-unit trial, the lead time has stretched to 12-14 weeks because of the larger production lot, and the OEM is typically willing to negotiate custom packaging, exclusive badging, and pallet-level shipping. The 5,000-unit tier is also where the brand owner should lock a 12-month forward contract with the OEM to insulate against steel price fluctuations and zinc plating cost increases.
The 5-gate factory qualification matrix for vertically integrated OEM
The 5-gate factory qualification matrix summarizes the brand owner's evaluation of a cutting machine pressure plate OEM across five dimensions: forging capability, heat treatment capability, CNC machining capability, plating capability, and badging / packaging capability. Each dimension is scored on a 1-5 scale, with 5 being best-in-class. A factory scoring 20 or higher out of 25 is a serious candidate for the brand owner's private-label program. A factory scoring 12 or lower should be excluded from the final selection. The matrix is applied to the 4-6 vertically integrated OEMs that survive the 4-question triage in week 1.
| Dimension | Score 1 (excluded) | Score 3 (acceptable) | Score 5 (best-in-class) |
|---|---|---|---|
| Forging capability | No forging dies, no in-house forging | Basic forging dies, single-station cold heading | Multi-station cold heading + forging dies, in-house die maintenance, 40+ CNC machines |
| Heat treatment capability | Outsourced heat treatment | In-house furnace, basic temperature control | In-house furnace per BS EN 10083-3, calibrated temperature uniformity, hardness test per BS EN ISO 6508-1 |
| CNC machining capability | Manual machining only | Basic CNC turning, IT10 tolerance | CNC turning + milling per ISO 2768 medium grade, in-process dimensional inspection |
| Plating capability | Outsourced plating | In-house plating line, no salt spray testing | In-house plating line per BS EN ISO 1456, in-house NSS salt spray chamber per BS EN ISO 9227 |
| Badging + packaging capability | No in-house badging, outsourced carton design | Basic badge tooling, single-color Pantone | Multi-color Pantone matching, in-house carton design, manual translation coordination |
The 5-gate matrix is applied with on-site factory audit data, not RFQ response claims. The forging capability score is verified by reviewing the forging die inventory (showing the range of plate diameters and thicknesses the factory can produce without custom die setup), the cold heading machine count and age, and the sample forged parts from past production lots. The heat treatment capability score is verified by reviewing the furnace calibration records, the temperature uniformity mapping, and the hardness test certificates from past production lots.
The CNC machining capability score is verified by reviewing the CNC machine count and age (preferably Mazak, Haas, or Doosan for ±0.01mm tolerance), the in-process inspection equipment (CMM, optical comparator, surface roughness tester), and the sample machined parts from past production lots with dimensional reports. The plating capability score is verified by reviewing the plating tank capacity, the plating chemistry control records, the XRF coating thickness gauge calibration, and the in-house salt spray chamber calibration and past NSS test reports.
The badging / packaging capability score is verified by reviewing the badge tooling inventory (showing the range of badge sizes and Pantone colors the factory can match), the in-house carton design samples, the manual translation coordination process (typically with a third-party translation vendor), and the past brand-owner packaging samples. The matrix output is the input to the final OEM selection.
The brand owner should select the top 2 OEMs by matrix score and run parallel 200-unit trial orders with both. The 200-unit trial order then becomes the final selection filter, with the OEM producing the better FAT report and the better-customized final plate winning the 1,000-unit launch order. Running parallel trials de-risks the single-source dependency and gives the brand owner negotiating leverage on the launch order pricing. The trial order should include the FAT inspection (witnessed on-site by the brand owner's engineering team or a third-party inspection agent) and the badging / packaging pre-production sample (reviewed by the brand owner's marketing team) before the launch order commitment.
When NOT to private-label (the 3 deal-breaker scenarios)
Private-label cutting machine pressure plate programs are not the right commercial model for every brand owner scenario. There are three deal-breaker scenarios where the brand owner should stay with the OEM-branded supply rather than launching a private-label program. Identifying these scenarios before the OEM qualification saves the brand owner 6-12 months of program delay.
Deal-breaker scenario 1 — Annual purchasing volume below 1,000 units. A brand owner with annual purchasing volume below 1,000 units cannot amortize the forging die setup, the heat treatment qualification, the FAT process, the badging tooling, and the manual translation across enough units to justify the program cost. The break-even point for a private-label cutting machine pressure plate program is approximately 1,000 units per year. Below 1,000 units, the OEM-branded supply is the lower total-cost option.
Deal-breaker scenario 2 — Target market requires OEM-branded service network. Some target markets (notably North American and European professional contractor channels) require OEM-branded service network coverage for warranty and serviceability. A private-label cutting machine pressure plate cannot access the OEM service network, and the brand owner would need to build a parallel service network — which is typically uneconomic below 5,000-10,000 units annual volume. In these markets, OEM-branded supply remains the lower-risk option.
Deal-breaker scenario 3 — Plating chemistry is locked by regional environmental regulation. Some regions (notably EU under REACH, California under Prop 65) restrict specific plating chemistries or require specific wastewater treatment documentation. A private-label program using a restricted plating chemistry is not feasible without the regional regulatory compliance, and the OEM must demonstrate wastewater treatment documentation and chemistry compliance for the target market. If the OEM cannot provide the regulatory documentation, the brand owner should not commit to the private-label program.
The 3 deal-breaker scenarios cover approximately 15-20% of the power tool brand-owner RFQ pool. The remaining 80-85% are candidates for a private-label program if the OEM passes the 5-gate qualification matrix. The brand owner should run the deal-breaker screen first (week 0), then run the 4-question triage (week 1), then run the 5-gate matrix (weeks 2-6), then commit to the parallel 200-unit trial orders (weeks 7-8). The total qualification timeline is 8-10 weeks and produces a defensible OEM selection with documented engineering and FAT evidence.
Engineering takeaway: vertical integration is what brand owners actually buy
The most important lesson from the 3-supplier-type pattern is that power tool brand owners are not buying cutting machine pressure plate hardware at a unit price — they are buying a vertically integrated OEM partnership that can deliver forging + heat treatment + CNC machining + plating + badging under one quality system with one project manager and one lead time commitment. A factory that quotes 20% below the median but outsources the heat treatment and the plating to separate vendors is not offering a discount — it is offering a 2-vendor logistics chain that will add 2-4 weeks of lead time variance and 1-2 layers of quality risk. A factory that quotes at the median with documented in-house forging + heat treatment + CNC + plating + badging capability is offering the vertical integration that the brand owner's launch program actually depends on.
For power tool brand owners evaluating Chinese OEMs like Yuyao Guling Hardware — a precision forging and metal forming manufacturer with 40+ fully automatic CNC machines and cold-heading lines, in-house heat treatment, in-house CNC machining, in-house zinc plating, and in-house badging / packaging capability for a true forging-to-surface-treatment OEM line — the private-label program should follow a five-step framework: (1) confirm in-house forging die inventory matches the brand owner's specification without custom die setup; (2) confirm in-house heat treatment furnace with BS EN 10083-3 steel grade certification; (3) confirm in-house CNC machining to ISO 2768 tolerance grade; (4) confirm in-house plating line with BS EN ISO 9227 NSS salt spray testing; (5) confirm in-house badging and packaging with Pantone color matching and carton design capability.
For brand owners beginning a private-label cutting machine pressure plate program, the recommended starting point is a custom precision forged power tool components OEM engagement to confirm the in-house forging die inventory and the OEM development timeline. For brand owners evaluating the broader product line capability, the best China outer flange nut factories manufacturers reference provides the cold-heading product line context. For brand owners specifying the conversion joint interface, the rust removal and polishing conversion joint product catalog provides the dimensional and thread specification baseline for the private-label program.
Procurement questions on private-label cutting machine pressure plate development
What is the minimum MOQ for a private-label cutting machine pressure plate program?
The minimum MOQ for a private-label cutting machine pressure plate program from a vertically integrated Chinese OEM is typically 200 units for a pilot run with custom badging and packaging, and 1,000 units for a launch run with full private-label carton design, custom tooling, and surface treatment specification. OEM factories quoting under 200 units MOQ for custom-branded cutting machine pressure plates are almost always trading companies without actual production lines.
What is the OEM development timeline from forging to surface treatment?
The OEM development timeline for a private-label cutting machine pressure plate is 10-14 weeks from RFQ approval to first article inspection: 2-3 weeks for specification alignment and forging die design, 2-3 weeks for forging sample fabrication and heat treatment, 1-2 weeks for CNC machining to final dimensional tolerance, 2-3 weeks for surface treatment (zinc plating, black oxide, or nickel plating), 1-2 weeks for FAT (Factory Acceptance Test) and badging/packaging sample, and 2 weeks for production lot preparation. Vertically integrated OEMs can compress this to 8-10 weeks by running forging + machining + surface treatment in parallel.
What is the price difference between private-label and OEM-branded cutting machine pressure plates?
Private-label cutting machine pressure plates typically cost 35-50% less than the equivalent OEM-branded unit at the same material and surface treatment specification, driven by the elimination of brand premium and OEM distributor margin. The savings are largest in the cutting machine accessory market where the OEM brand premium is typically 40-60% of the retail price. At 1,000+ unit annual volume, the savings compress to 25-35% because the OEM brand premium is smaller as a percentage of the BOM cost.
What surface treatments are available for cutting machine pressure plates?
Cutting machine pressure plates are available with four standard surface treatments: (1) zinc plating (Zn ≥ 8μm per BS EN ISO 1456) for general industrial indoor / short-term outdoor use, with 48-hour NSS salt spray rating; (2) black oxide coating for indoor controlled storage applications; (3) electroless nickel plating (Ni ≥ 10μm) for marine / offshore applications, with 240+ hour NSS rating; (4) Dacromet / zinc flake coating for high-corrosion applications, with 480+ hour NSS rating. The surface treatment selection should match the brand owner's target market and warranty requirements.
What materials are available for cutting machine pressure plates?
Cutting machine pressure plates are typically made from 45# medium carbon steel (per BS EN 10083-3 C45 grade) for general industrial applications, 40Cr alloy steel for higher-load applications, or 20CrMnTi for impact-resistant applications. For stainless steel requirements (food-grade, medical, or marine applications), 304 stainless or 316 stainless is available at 3-5x the cost of carbon steel. The material selection should be matched to the cutting machine's torque load, RPM duty, and target market corrosion exposure.
How do you verify a vertically integrated Chinese OEM's forging and surface treatment capability?
A vertically integrated Chinese OEM's forging and surface treatment capability is verified by reviewing: (1) the cold-heading and forging die inventory (showing the range of plate diameters and thicknesses the factory can produce); (2) the heat treatment furnace capacity (showing the throughput per shift and the temperature uniformity per BS EN 10083-3); (3) the in-house CNC machining capability (showing the tolerance grade per ISO 2768); (4) the in-house plating line (showing the tank capacity, the plating chemistry, and the salt spray testing capability per BS EN ISO 9227); (5) the badging and packaging capability (showing the badge tooling, the Pantone color matching, and the carton design samples). All five capabilities should be verified on-site, not claimed in RFQ responses.