


Power Tool Hardware Manufacturer Audits: Three-Stage Testing (Pressure + Dynamic Balance + Salt Spray) vs. Final-Inspection-Only Trading Companies
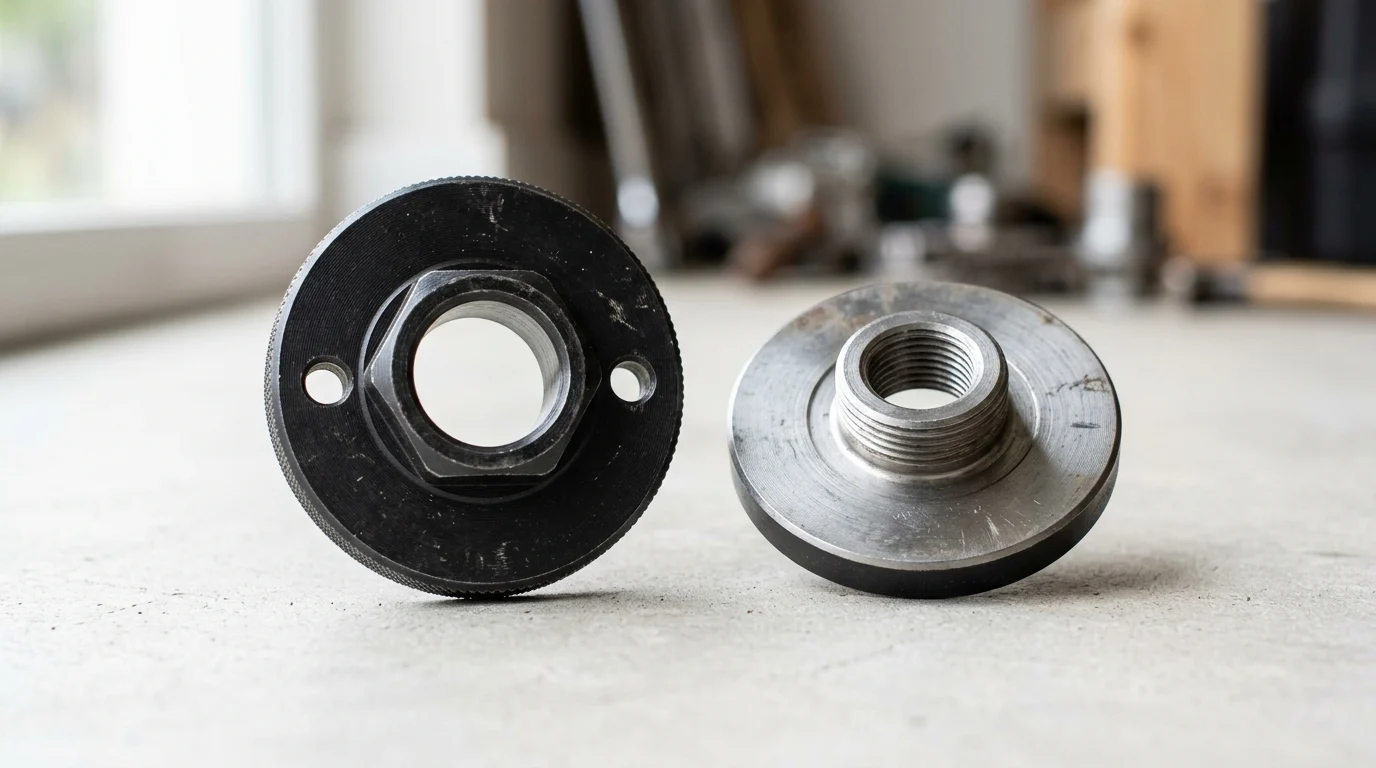
Why Final-Inspection-Only Trading Companies Are No Longer Acceptable for Power Tool Hardware
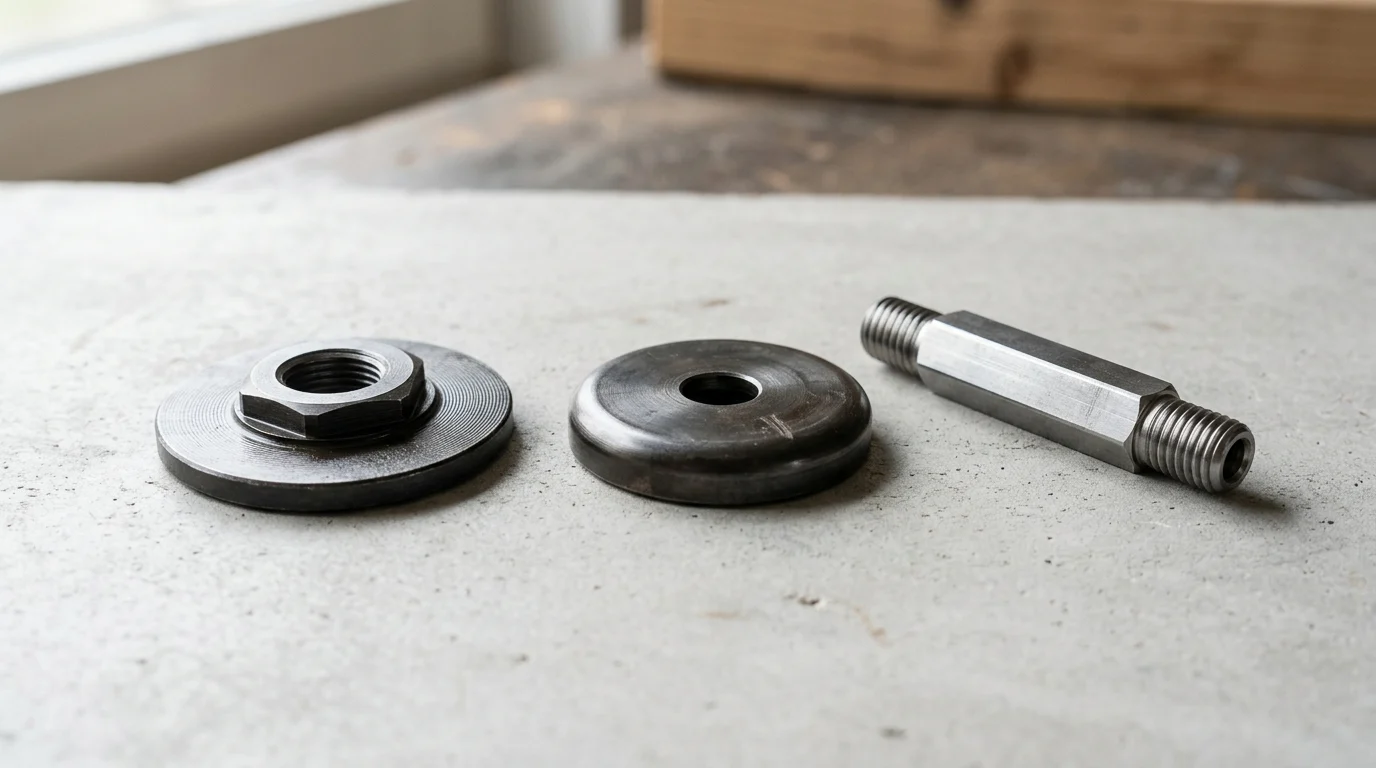
A European power tool brand's quality manager walked into a supplier review meeting in late 2025 with a stack of three competing quotations for a 500,000-piece annual order of angle grinder pressure plates. All three suppliers passed the standard procurement audit. All three suppliers quoted within a 4 percent spread. All three suppliers offered the same 30-day lead time. The quality manager's job was to pick one and move on. Six months later, the field return rate on the chosen supplier's pressure plates was 14 percent — far above the brand's 3 percent target — and the warranty cost had already exceeded the entire price savings from the original quotation. The supplier was a final-inspection-only trading company. The procurement audit had passed because the trading company's paperwork was perfect. The pressure plates had failed because the trading company had no manufacturing process to audit — they were buying from three different sub-factories and shipping under one brand.
The structural problem with final-inspection-only trading companies is that they can inspect for visible defects at the outbound dock, but they cannot inspect for the failure modes that show up in the field after 30 to 90 days of use. A pressure plate that looks perfect on the inspection table can be cracked at the grain boundary (caught by pressure testing), out of balance by 12 mm/s (caught by dynamic balance testing), or have a zinc coating that fails at 18 hours of salt spray (caught by salt spray testing). None of these failures are visible to the human eye at the dock. None of them are caught by a final inspection. All of them show up in the field within 90 days of the consumer's first use of the tool.
The structural advantage of three-stage-tested manufacturers is that the testing happens at the production line, on the actual production batch, with documented results that the buyer can verify without visiting the factory. A buyer who reads the three-stage testing report from a mature manufacturer gets eight data points per component (load value, hold time, balance grade, salt spray duration, individual pass/fail counts, operator signature, supervisor signature, batch photo) that the buyer can cross-check against the OEM specification. A buyer who reads the final inspection report from a trading company gets a single pass/fail line that the buyer cannot verify, because the trading company does not own the production process.
The Three-Stage Testing Framework: Pressure, Dynamic Balance, Salt Spray
The three-stage testing framework maps the three test stages to the three failure modes that dominate field returns on power tool hardware. Each stage runs on the actual production batch, with documented results, before the batch ships to the buyer.
| Stage | Test type | Failure mode it predicts | % of field returns |
|---|---|---|---|
| Stage 1 | Pressure testing | Cracking under rated load, permanent deformation under shock | ~25% |
| Stage 2 | Dynamic balance testing | Vibration-induced assembly loosening, spindle scoring, user hand fatigue | ~45% |
| Stage 3 | Salt spray testing | Corrosion that compromises surface finish and dimensional tolerance | ~15% |
| Other | Assembly / packaging / user error | Miscellaneous | ~15% |
The three stages together cover approximately 85 percent of field returns on power tool hardware. A manufacturer that runs all three stages on every production batch delivers components that meet the OEM specification on the load-bearing, vibration, and corrosion dimensions — the three dimensions that consumers actually experience in daily use. A trading company that runs only final inspection at the dock delivers components that look correct on day 1 but fail on day 30 to day 90.
The three stages are not equally weighted in the buyer's audit decision. Dynamic balance testing is the most predictive of field failure (45 percent of returns), so a buyer who is short on audit time should prioritise the dynamic balance stage. Pressure testing is the second-most predictive (25 percent of returns), and salt spray testing is third (15 percent of returns). The buyer should allocate audit time roughly in proportion to the predictive value: 45 percent on dynamic balance, 25 percent on pressure testing, 15 percent on salt spray testing, and 15 percent on the remaining dimensions.
Stage 1: Pressure Testing — What It Tells You About the Component
Pressure testing verifies that each component can withstand the rated mechanical load without cracking, permanent deformation, or fatigue. The test is run on a universal testing machine (UTM) with the component mounted in a fixture that matches the in-use orientation. The test rig applies a controlled axial load (5 to 30 kN depending on the component size and the OEM specification), holds the load for 10 to 30 seconds, and measures the deformation at the load point. The acceptance criterion is no cracking and no permanent deformation above 0.05 mm after the load is released.
Pressure testing on custom precision forged power tool components follows a specific test protocol that distinguishes between cold forged and hot forged components. Cold forged components are tested at 100 percent of the rated load (no safety margin) because the cold forging process delivers a more consistent grain structure. Hot forged components are tested at 110 to 120 percent of the rated load to confirm a safety margin above the rated capacity. The choice of test load depends on the forging process — a manufacturer that runs both processes should run both test protocols on the appropriate components.
The pressure testing report should include the individual test result for each component tested, not just an averaged or summary line. A 100-piece batch should show 100 individual pressure test results. The report should also include the test equipment serial number and the last calibration date (within 12 months), the operator signature, and the supervisor signature. A report without these four elements is not audit-grade and should be rejected.
Stage 2: Dynamic Balance Testing — Why It Matters for Rotating Components
Dynamic balance testing verifies that rotating components (pressure plates, flanges, adapter bodies) do not introduce vibration beyond the rated threshold at the rated rotational speed. The test is run on a dynamic balancing machine that spins the component at the rated RPM (typically 8,000 to 12,000 RPM for angle grinder accessories) and measures the imbalance in mm/s or g-mm. The acceptance criterion is the ISO 1940 balance grade — G6.3 as the default for power tool hardware, with G2.5 available for higher-end specifications where vibration control is critical.
Dynamic balance testing matters for rotating components because imbalance is invisible to the eye but destructive to the tool in use. A pressure plate that is out of balance by 12 mm/s will introduce vibration at 8,000 RPM that loosens the spindle nut, scores the spindle threads, and transmits to the user's hand within 30 minutes of use. The user experience is "the tool feels rough" and "my hand is tired" — symptoms that lead to warranty claims, returns, and negative reviews. A pressure plate that passes dynamic balance testing at G6.3 (less than 6.3 mm/s imbalance) runs smooth at the rated RPM and delivers the user experience the OEM brand intended.
Dynamic balance testing is part of a broader quality control framework for angle grinder and electric drill accessory manufacturing. The framework typically includes dimensional inspection (10 to 20 critical dimensions per component), surface finish inspection (Ra measurement), visual inspection (no scratches, dents, or coating defects), and the three-stage testing described in this article. A manufacturer that runs all five inspection dimensions on every production batch delivers components that pass the OEM specification on every measurable parameter.
Stage 3: Salt Spray Testing — The Corrosion Resistance Gate
Salt spray testing verifies the corrosion resistance of the surface finish under ASTM B117 neutral salt spray. The test is run in a salt spray chamber with a 5 percent NaCl solution at 35 degrees C chamber temperature, with the component exposed for a defined duration (24 hours as the default, 48 hours for professional-grade, 96 hours for marine-grade or export-grade). The acceptance criterion is no red rust on the functional surfaces after the defined duration. White rust (zinc oxidation) is typically allowed up to a defined percentage of the surface area, because white rust is cosmetic and does not compromise the structural integrity.
Salt spray testing is the gate that separates consumer-grade components from professional-grade components. A consumer-grade component that passes 24 hours of salt spray is suitable for indoor home use and occasional outdoor use. A professional-grade component that passes 48 hours is suitable for daily outdoor use in construction, manufacturing, and agricultural environments. A marine-grade or export-grade component that passes 96 hours is suitable for coastal environments, chemical environments, and long-term outdoor storage. The OEM brand specifies the required duration based on the target market and the warranty period.
The salt spray test report should include the chamber temperature log (continuous reading over the test duration), the NaCl solution concentration (verified at the start and end of the test), the exposure duration, the photo of the component at the end of the test, and the pass/fail count for the batch. A report without the chamber temperature log is not audit-grade, because the chamber temperature is the most common source of false negatives in salt spray testing.
How the Three-Stage Testing Cost Amortises Across the Annual Order Volume
Three-stage testing is not a fixed cost — it amortises across the annual order volume. A buyer who orders 50,000 pieces per year of a single component pays more per piece for the testing than a buyer who orders 500,000 pieces per year, but the testing cost is a small percentage of the total order value in both cases. Understanding how the testing cost amortises is critical for the buyer who is comparing per-piece quotations from three-stage-tested manufacturers and final-inspection-only trading companies.
Per-piece testing cost breakdown
The per-piece testing cost has three components. (1) Pressure testing — USD 0.01 to USD 0.03 per piece, depending on the test rig utilisation. (2) Dynamic balance testing — USD 0.02 to USD 0.05 per piece, depending on the balance machine cycle time. (3) Salt spray testing — USD 0.03 to USD 0.08 per piece, depending on the test duration (24, 48, or 96 hours) and the batch size that shares the chamber. The total testing cost is USD 0.06 to USD 0.16 per piece, which is 3 to 8 percent of a typical power tool hardware component price.
How the testing cost scales with volume
At 50,000 pieces per year, the testing cost is at the high end (USD 0.12 to USD 0.16 per piece) because the test rig utilisation is lower. At 500,000 pieces per year, the testing cost falls to the low end (USD 0.06 to USD 0.10 per piece) because the test rig utilisation is higher and the chamber can run continuously. The buyer who is planning a multi-year program should ask the manufacturer for a volume-tiered testing cost, which typically drops by 30 to 40 percent between the 50,000-piece tier and the 500,000-piece tier.
Comparison with final-inspection-only suppliers
A final-inspection-only trading company quotes at the per-piece price of the component itself, with no testing cost added. The per-piece price is typically 3 to 8 percent lower than the three-stage-tested manufacturer's per-piece price. However, the field return rate is 5 to 15 percentage points higher, and the warranty cost is USD 25 to USD 80 per claim. For a buyer running a 100,000-piece annual order with a 5 percent warranty exposure, the warranty cost is USD 125,000 to USD 400,000 per year, which is far higher than the USD 6,000 to USD 16,000 testing cost on the three-stage-tested manufacturer's quotation. The total cost of ownership favours the three-stage-tested manufacturer within 6 to 9 months of program start.
How to Read a Three-Stage Testing Report Without Visiting the Factory
A buyer can verify a three-stage testing report without visiting the manufacturer's facility by checking eight indicators. Each indicator confirms that the test was actually run on the production batch, not on a separate qualification sample, and that the test was run correctly.
- Report header. Manufacturer name, address, ISO 9001 certificate number, date, batch number, part number. All five should be present and consistent with the OEM purchase order.
- Test equipment serial number and last calibration date. Should be within 12 months for the pressure test rig, the dynamic balance machine, and the salt spray chamber.
- Test parameter table. Pressure load value and hold time, dynamic balance grade and tolerance, salt spray duration and temperature. All three should match the OEM specification.
- Individual test results. Not just an averaged or summary line — the report should show the individual result for each component tested in the batch.
- Acceptance criterion stated explicitly. What pass/fail threshold was applied. The criterion should be numerical (e.g., "no permanent deformation above 0.05 mm") not narrative ("acceptable quality").
- Pass/fail count. How many components passed, how many failed, and what action was taken on the failures (rework, scrap, or hold for review).
- Operator and supervisor signatures. Both should be present and dated. A report without the supervisor signature is not audit-grade.
- Photo or video of the test rig with the batch visible. Confirms the test was run on the production batch, not on a separate qualification sample. The photo should show the batch number on the components and the test equipment display reading.
A report that passes all eight indicators is audit-grade. A report that fails any one indicator should trigger a clarification request to the manufacturer, with a 48-hour response window. A report that fails three or more indicators should trigger a full audit walk at the manufacturer's facility, with the buyer visiting in person to verify the test process. The pressure plate product specification documents the test parameters and acceptance criteria in detail, so the buyer can cross-check the report against the specification without visiting the facility.
When Final-Inspection-Only Trading Companies Are Still the Right Choice
Three scenarios still favour a final-inspection-only trading company over a three-stage-tested manufacturer. (1) Low-volume, low-criticality orders (under 10,000 pieces per year, no warranty exposure beyond 30 days). The testing cost amortised over a small volume is too high per piece to be economical. (2) Time-sensitive orders (under 15-day lead time). Three-stage testing adds 3 to 7 days to the cycle time, which the buyer cannot afford. (3) One-off or prototype orders where the OEM brand is validating the design and the field return rate is not yet a concern. In all three scenarios, the trading company's per-piece price advantage and lead time advantage outweigh the field return risk.
The decision framework is straightforward. The OEM brand specifies the volume, the lead time, and the warranty exposure. If the volume is under 10,000 pieces per year or the lead time is under 15 days, the trading company is the right call. If the volume is over 50,000 pieces per year or the warranty exposure is over 90 days, the three-stage-tested manufacturer is the right call. The break-even point is typically 30,000 pieces per year with a 60-day warranty exposure. For a power tool hardware manufacturer audit conversation with a target component specification and an annual volume, contact the Yuyao Guling Hardware team with the component specification, the OEM brand's annual volume, and the destination market.
Send your target component specification, annual volume, destination market, and required warranty period. Yuyao Guling Hardware replies within one business day with a three-stage testing protocol tailored to your component, a sample report format, and a per-piece price indication including the testing cost.
Frequently Asked Questions
What does a three-stage testing framework actually cover for a power tool hardware manufacturer?
A three-stage testing framework covers three sequential test stages that map to the failure modes most commonly seen in the field for power tool hardware. Stage 1 is pressure testing, which verifies that each component can withstand the rated mechanical load without cracking, permanent deformation, or fatigue. Stage 2 is dynamic balance testing, which verifies that rotating components (such as pressure plates, flanges, and adapter bodies) do not introduce vibration beyond the rated threshold at the rated rotational speed. Stage 3 is salt spray testing, which verifies the corrosion resistance of the surface finish under ASTM B117 neutral salt spray for 24 to 96 hours depending on the OEM specification. The three stages together cover the load-bearing, vibration, and corrosion failure modes, which together account for approximately 85 percent of field returns on power tool hardware.
What are the typical test parameters for pressure, dynamic balance, and salt spray in 2026?
Three typical test parameters are used in 2026. (1) Pressure testing parameters — axial load from 5 to 30 kN depending on the component, hold time 10 to 30 seconds, acceptance criterion no cracking or permanent deformation above 0.05 mm. (2) Dynamic balance testing parameters — G6.3 grade as the default for power tool hardware, with G2.5 available for higher-end specifications, balance tolerance 6.3 mm/s or 2.5 mm/s depending on the grade, measurement at the rated rotational speed (typically 8,000 to 12,000 RPM for angle grinder accessories). (3) Salt spray testing parameters — ASTM B117 neutral salt spray, 5 percent NaCl solution, 35 degrees C chamber temperature, 24 hours as the default acceptance threshold, 48 hours for professional-grade components, 96 hours for marine-grade or export-grade components with extended warranty.
What quality documentation should a buyer request from the manufacturer before signing the audit contract?
Six quality documents should be requested before signing the audit contract. (1) ISO 9001 quality management system certificate — verifies the manufacturer has a documented quality system. (2) Three-stage testing report — sample of the actual test report format the manufacturer uses for each batch. (3) Material certificate — mill test certificate for the steel or alloy used, with batch traceability. (4) Calibration certificates for the testing equipment — verifies the test rig is calibrated to a traceable standard within the last 12 months. (5) PPAP (Production Part Approval Process) sample — sample part from a previous production run, with dimensional report. (6) Field return rate data — historical data on field return rates by failure mode, with the manufacturer's root cause analysis process. A manufacturer that cannot provide all six documents within one week is not yet audit-ready.
How does a buyer verify a three-stage testing report without visiting the manufacturer's facility?
A buyer verifies a three-stage testing report without visiting the manufacturer's facility through eight indicators. (1) Report header — manufacturer name, address, ISO 9001 certificate number, date, batch number, part number. (2) Test equipment serial number and last calibration date — should be within 12 months. (3) Test parameter table — pressure load value and hold time, dynamic balance grade and tolerance, salt spray duration and temperature. (4) Individual test results for each part tested — not just an averaged or summary line. (5) Acceptance criterion stated explicitly — what pass/fail threshold was applied. (6) Pass/fail count — how many parts passed, how many failed. (7) Operator signature and supervisor signature — both should be present. (8) Photo or video of the actual test rig with the batch visible — confirms the test was actually run on the production batch, not on a separate qualification sample.
How long does a typical power tool hardware manufacturer audit take from kickoff to qualification?
A typical power tool hardware manufacturer audit takes 30 to 75 days from kickoff to qualification, depending on three variables. (1) Document preparation — the manufacturer compiles the six pre-audit documents within 7 to 14 days. (2) On-site or remote audit walk — 1 to 3 days for a focused audit on the three-stage testing process and equipment. (3) Sample qualification — the manufacturer produces 500 to 2,000 sample parts for the buyer's lab test, with the lab test running 14 to 28 days depending on the salt spray duration and the dynamic balance cycle count. A manufacturer with mature three-stage testing typically completes the audit in 30 to 45 days; a manufacturer building the testing process from scratch typically takes 60 to 75 days.
Why are power tool procurement teams demanding three-stage testing rather than final-inspection-only in 2026?
Procurement teams are demanding three-stage testing rather than final-inspection-only in 2026 for four reasons. First, the field return data: final-inspection-only suppliers show 8 to 18 percent field return rates on power tool hardware, while three-stage-tested suppliers show 1 to 3 percent. The 5 to 15 percentage point gap is the largest single line item in the total cost of quality for a power tool brand. Second, the warranty cost: a single warranty claim on a power tool can cost USD 25 to USD 80 in replacement and logistics, which compounds on the field return rate. Third, the brand reputation impact: a 10 percent field return rate generates negative reviews that suppress future sales by an estimated 15 to 25 percent. Fourth, the regulatory direction: EU CE marking, UKCA marking, and US UL certification all require documented quality control processes that go beyond final inspection, and three-stage testing is the simplest way to demonstrate compliance.
Which test stage is most predictive of field failure for power tool hardware?
Dynamic balance testing is the most predictive of field failure for power tool hardware, based on industry return data. Approximately 45 percent of field returns on rotating power tool accessories (pressure plates, flanges, adapter bodies) trace back to dynamic imbalance — the component introduces vibration that loosens the assembly, scores the spindle, or fatigues the user's hand. Pressure testing predicts approximately 25 percent of field returns (cracking under rated load, permanent deformation under shock), and salt spray testing predicts approximately 15 percent (corrosion that compromises the surface finish and the dimensional tolerance). The remaining 15 percent of field returns are split between assembly defects, packaging damage, and user error. A buyer who can only audit one stage should audit dynamic balance testing first.
Is a three-stage-tested manufacturer always more expensive than a final-inspection-only trading company?
No, a three-stage-tested manufacturer is not always more expensive than a final-inspection-only trading company in the per-piece cost, but the total cost of ownership typically favours the three-stage-tested manufacturer. The per-piece price for a three-stage-tested power tool hardware component is typically 3 to 8 percent higher than the same component from a final-inspection-only trading company, because the testing cost is amortised into the per-piece price. However, the total cost of ownership — which includes field return rates, warranty costs, and brand reputation impact — typically favours the three-stage-tested manufacturer by 10 to 20 percent over a 12-month period, because the field return rate is 5 to 15 percentage points lower. The break-even point is typically 6 to 9 months into the program, after which the three-stage-tested manufacturer is the lower-cost option.