


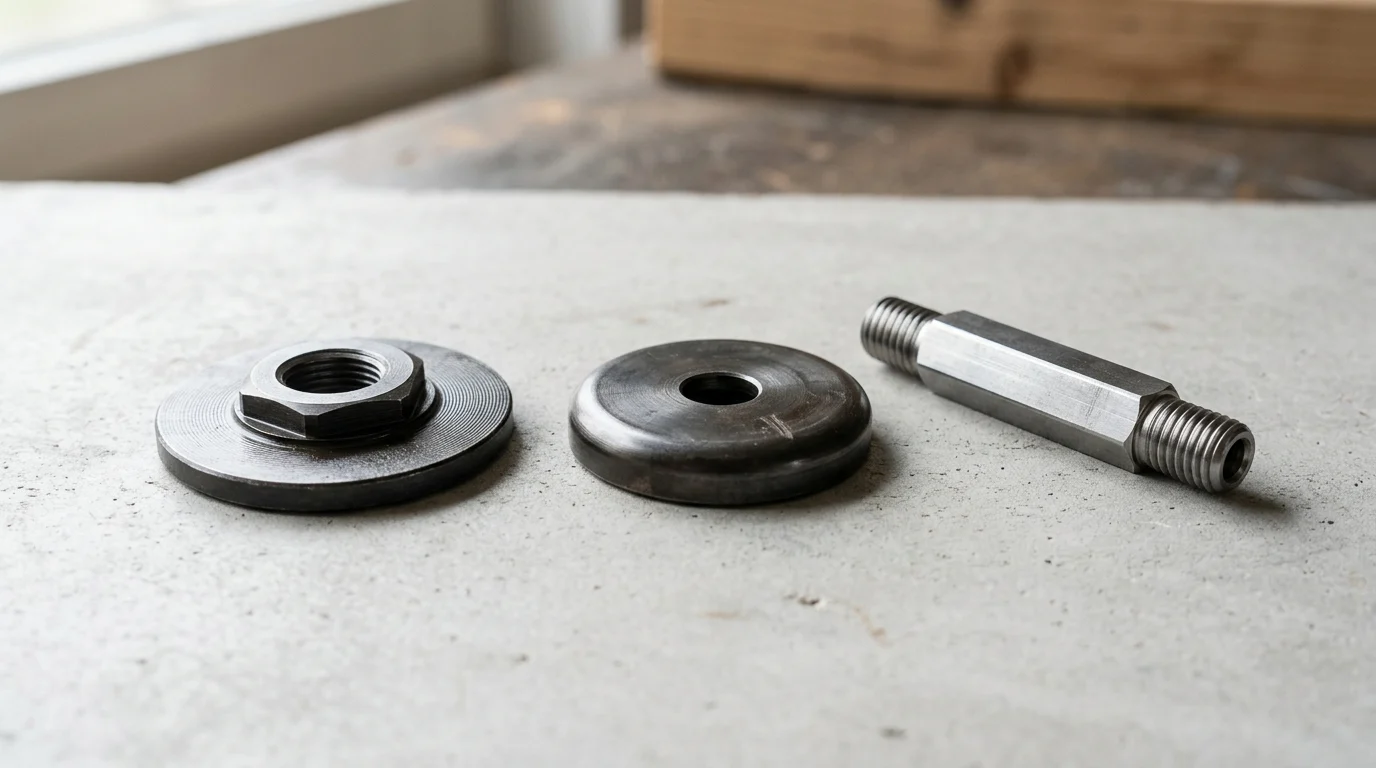
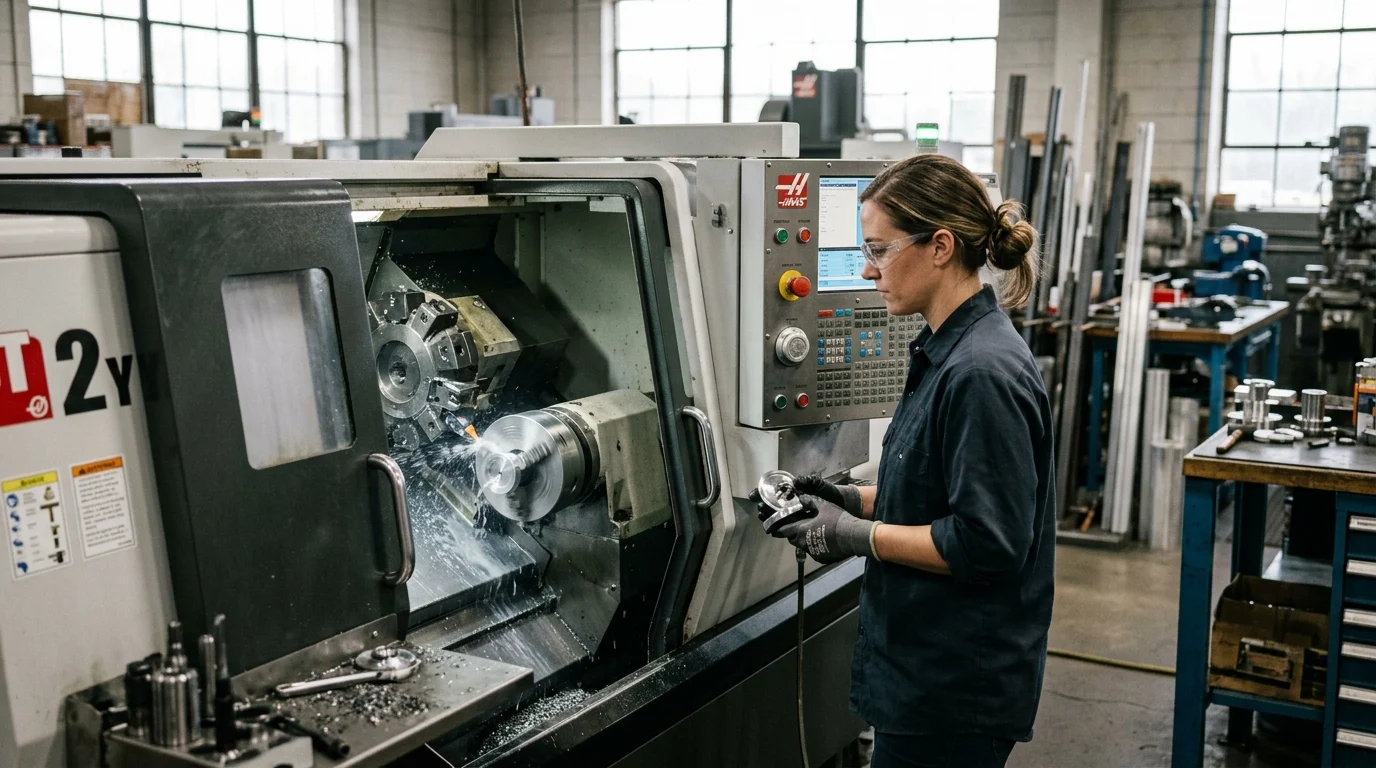
When a grinder accessory spins at industrial speeds, supply efficiency is not just about faster delivery—it is about repeatable safety, fit, and durability. OEM CNC manufacturing gives buyers tighter control over pressure plates, conversion joints, polishing wheels, waxing pads, wool wheels, and electric drill adapters by combining precision machining with the right forming, heat treatment, and inspection steps. For distributors, tool brands, and hardware buyers, the result is fewer fit issues, more stable batch quality, and clearer specifications for high-volume sourcing. This article explains where CNC adds the most value, what specifications buyers should define, and how modern production systems help reduce defects and delays.
Benefits of OEM CNC Manufacturing for Angle Grinder Accessories
Power tools take a massive beating in the field. When an angle grinder spins at upwards of 11,000 RPM, or an electric drill drives a heavy-duty attachment, the accessories connected to them—from pressure plates to wool wheels—need to be perfectly balanced and incredibly resilient. That is where OEM CNC manufacturing steps in, transforming raw steel into precision-engineered components that can handle intense mechanical stress without failing.
Relying on a mature industrial foundation allows manufacturers to push the boundaries of what these accessories can withstand. By modernizing the production line with automated equipment, brands can ensure that every pressure plate, conversion joint, and polishing wheel performs safely under heavy industrial loads.
Integrated forging, machining, and heat treatment
Getting a durable part usually means combining multiple manufacturing steps rather than relying on a single method. The most robust process route starts with raw material, moves to forging or stamping to establish the basic shape and optimize the metal's grain structure, and follows up with CNC machining for tight tolerances. Finally, the parts undergo heat treatment and surface finishing.
This integrated route guarantees that the metal forming solutions are not just dimensionally accurate, but structurally sound enough to survive heavy industrial use. By keeping forging, machining, and heat treatment closely linked in the supply chain, manufacturers can tightly control the mechanical properties of the final product. It is worth noting, however, that not all parts require this full suite; low-stress, non-rotating hardware may be better produced by simpler stamping or cold heading alone to avoid over-specifying and overpaying.
Improved fit for pressure plates and related parts
Pressure plates are the unsung heroes of cutting machines and grinders. If a pressure plate has even a fraction of a millimeter of runout, the entire tool vibrates, leading to operator fatigue and premature bearing failure. By leveraging advanced CNC processes, manufacturers can lock in perfect fits for standard specifications like the 100, 125, 150, 180, and 230 types.
If you are sourcing Angle Grinder Parts, looking for this level of dimensional accuracy is non-negotiable. A precision-machined fit ensures that cutting wheels, waxing pads, and grinding discs remain securely locked in place, drastically reducing the risk of catastrophic disc failure at high speeds.
Consistent quality for high-volume production
High-volume production demands absolute repeatability. It does not matter if the first part off the line is perfect if the ten-thousandth part fails an inspection. Modern facilities utilizing fleets of up to 40 fully automatic CNC machine tools can maintain defect rates well below typical industry targets, such as 500 PPM (parts per million), depending on part complexity.
This level of consistency means assembly lines do not stall, and end-users get a reliable product every single time. Automated testing instruments integrated directly into the production workflow catch microscopic deviations early, ensuring that high-volume orders maintain the same exacting standards as small-batch prototypes.
Key Specifications Buyers Should Define
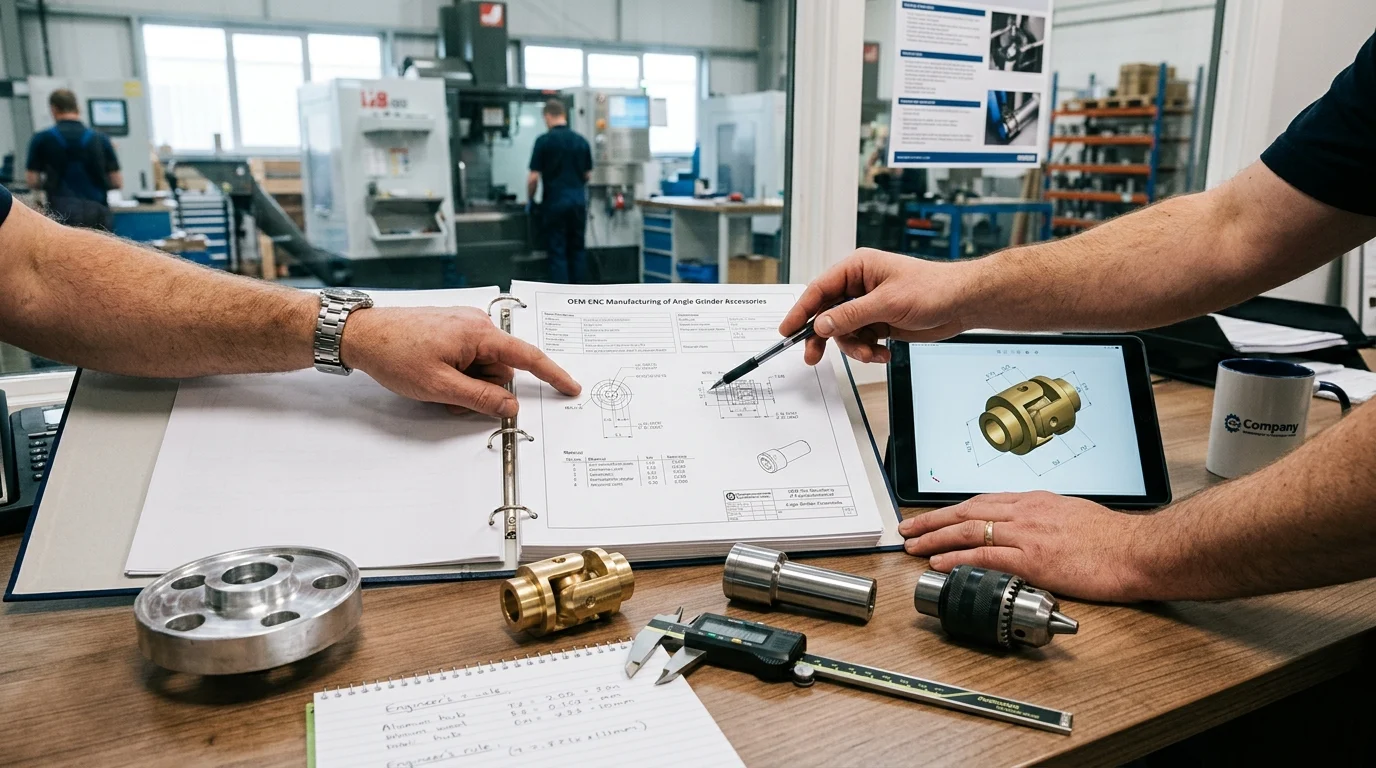
Before firing off a purchase order, buyers have to nail down the technical requirements. Vague specifications inevitably lead to mismatched expectations, creeping production costs, and parts that simply do not fit the intended power tool.
Drafting a comprehensive technical package upfront gives the OEM a clear roadmap, allowing them to optimize their machine setups and material purchasing for your specific project.
Materials, sizes, and tolerances
The foundation of any good accessory is its dimensional accuracy. Buyers need to clearly define the outer diameter, inner bore, thread specifications, and overall thickness. For high-speed rotating equipment, dimensional tolerances usually need to hit the ±0.01 mm mark.
Anything looser than that, and you risk dangerous wobbling during operation. Specifying these tight tolerances upfront ensures the manufacturer allocates the right CNC equipment—rather than older, less precise manual lathes—to your production run. However, buyers should add balanced caveats to their engineering drawings: over-specification raises costs significantly. Tight CNC tolerances should only be mandated where they directly impact safety, fit, or function. For static, low-stress components, looser tolerances are often perfectly acceptable.
Steel options such as 45 steel, A3 steel, and high carbon steel
Steel selection makes or breaks the lifespan of the product. You typically see three main players in this space: 45# steel, A3 steel, and high carbon steel. To ensure global buyers can specify accurately, it helps to map regional grades to international equivalents.
| Material Grade | Best Used For | Hardness Potential | Cost Profile |
|---|---|---|---|
| A3 Steel (Q235/SS400) | Low-stress backing pads, standard washers | Low to Medium | Very Economical |
| 45# Steel (C45/1045) | General pressure plates, standard joints | Medium (HRC 40-45) | Balanced |
| High Carbon | High-wear components, heavy-duty plates | High (HRC 45-55) | Premium |
Selecting the right grade depends entirely on the torque and friction the part will endure. For instance, 45# steel (C45/1045) is the industry workhorse, offering an excellent balance of machinability and post-heat-treat strength.
Functional requirements for angle grinder and cutting machine parts
Beyond just physical dimensions, you have to outline how the part will actually function in the field. Does the cutting machine part need specific surface treatments to resist rust in humid environments? Does it require dynamic balancing to prevent vibration?
When sourcing items like Polishing Accessories, specifying rotational balance and surface hardness (often targeting HRC 45-50) ensures the wool wheel or polishing pad runs smoothly without tearing itself apart under load. Communicating these functional requirements helps the factory dial in their heat treatment and finishing processes.
Where CNC Manufacturing Adds the Most Value
CNC machining is not just a manufacturing buzzword; it is a strategic tool for scaling quality. While older manual methods might work for basic hardware, modern power tool accessories demand a level of precision that only automated systems can reliably provide.
By understanding exactly where CNC technology adds the most value, buyers can make smarter decisions about which components require premium machining and which can rely on simpler forming techniques.
Automatic CNC machining for precision and repeatability
Automatic CNC machining takes human error out of the equation. By utilizing multi-axis lathes and automatic tapping machines, factories can churn out complex geometries with incredible repeatability. This automation can often reduce cycle times significantly—sometimes by 25% to 30% compared to semi-manual operations—depending on the specific part design.
Faster cycle times drive down per-unit costs without sacrificing quality. Furthermore, fully automatic machines can often run lights-out for certain production phases, significantly boosting the factory's overall output capacity and shortening delivery windows for bulk orders.
Quality checkpoints for threaded and fitted parts
Threaded components and fitted joints are notorious for causing assembly headaches. A slight burr or a mismatched thread pitch can scrap a whole batch of otherwise perfect parts. Implementing strict quality checkpoints using go/no-go gauges ensures every thread meets international standards.
Whether you are dealing with heavy-duty grinders or delicate Electric Drill Accessories, verifying thread integrity at multiple stages of production is crucial. CNC tapping centers provide the exact torque and pitch control required to make sure every accessory threads onto the tool spindle smoothly.
Forging versus CNC machining trade-offs
While the earlier section outlined the integrated process route, it is important to understand the specific trade-offs between these methods to avoid overpaying for unnecessary precision. It is rarely a choice of forging or CNC machining; it is usually about how they balance cost and accuracy. Cold heading and forging handle the bulk material movement efficiently, while CNC cleans up the critical mating dimensions.
| Process | Primary Function | Equipment Examples | Typical Tolerances |
|---|---|---|---|
| Cold Heading / Forging | Rapid near-net shaping, grain flow improvement | Models 19b, 24B, 28B, 136, 207 | ±0.1 mm to ±0.5 mm |
| CNC Machining | Final precision sizing, threading, finishing | Fully automatic CNC lathes, tapping centers | ±0.005 mm to ±0.02 mm |
Using a cold header or forging press for the initial form saves massive amounts of raw material and machining time. The subsequent CNC pass guarantees the part fits perfectly, offering the best of both worlds. For non-critical, low-stress parts, buyers might opt to skip the CNC phase entirely to save costs, relying solely on stamping or forging.
How to Reduce Sourcing Risk and Lead Time
Even the most precisely machined parts are useless if they are stuck in transit or delayed by supply chain bottlenecks. Managing sourcing risk and optimizing logistics is just as important as managing part quality.
Buyers who understand how to navigate OEM capacities and leverage regional manufacturing strengths can drastically cut down on their lead times and avoid costly stockouts.
Benefits of mature manufacturing clusters
Sourcing from mature manufacturing clusters offers a massive logistical advantage. These areas have dense, highly integrated supply chains where raw steel suppliers, heat treatment facilities, and plating shops are all located within a few miles of each other.
This proximity can often shave several days (frequently 5 to 7 days) off your total production lead time compared to dispersed supply chains. Because the factory does not have to ship parts across the country for a simple surface treatment, the risk of transit delays and lost inventory drops significantly.
How to evaluate supplier capacity
You need to know if a supplier can actually handle your volume before placing an order. Evaluating capacity means looking past the sales pitch and checking their actual equipment list. A solid OEM partner should have dozens of CNC machines and cold headers ready to go.
If your standard Minimum Order Quantity (MOQ) sits between 5,000 and 10,000 units, you need a factory that will not get bottlenecked by a single broken machine. Ask about their maximum monthly throughput and how they handle sudden spikes in order volume.
Practical steps to prevent production delays
To prevent unexpected delays, build buffer times into your initial order and be hyper-specific about finishing requirements. Ambiguity in surface treatment or heat treat specs is the number one cause of reworked batches and missed delivery dates.
For example, if you need a specific zinc plating thickness of 5 to 8 microns to prevent rust on Waxing Accessories, put it explicitly in the contract. Clear, quantifiable requirements ensure the factory gets it right the first time, keeping your supply chain moving smoothly.
How to Choose the Right OEM Partner
Finding a supplier is relatively easy; finding the right manufacturing partner takes a bit more digging. You want an OEM that deeply understands the specific, high-stress demands of the power tool accessory market.
A strong partnership is built on transparent communication, proven technical capabilities, and a mutual commitment to maintaining strict quality standards across every single production run.
Decision criteria for process, quality, and capacity
When evaluating potential partners, look for a proven, end-to-end process route. A manufacturer that handles forging, stamping, machining, heat treatment, and testing under one roof—or at least tightly manages them locally—offers superior quality control.
Advanced capabilities are also a major plus. Sometimes, specialized parts require powder metallurgy technology—a process ideal for creating complex, net-shape components like internal gears or self-lubricating fittings without the material waste of traditional machining. An OEM with diverse capabilities can pivot to the best method for your specific part.
When to choose a specialized manufacturer
General machine shops can make a metal disc, but specialized manufacturers understand the nuances of power tools. They know exactly why a 230-type pressure plate needs different structural integrity than a 100-type.
If you need specialized adapters or unique fittings, working with a dedicated Conversion Joint Manufacturer ensures you are getting engineering expertise, not just machine time. Specialized shops anticipate design flaws and can suggest material upgrades before production even begins.
Final procurement checklist before placing an order
Before you sign off on a mass production run, run through a strict final procurement checklist.
Key Takeaways
- Specify grinder sizes such as 100, 125, 150, 180, and 230 before ordering to ensure pressure plates, discs, and polishing attachments fit safely.
- Use CNC machining for rotating accessories because even minor runout can create vibration, operator fatigue, bearing wear, or disc failure at high RPM.
- Choose integrated forging, CNC machining, heat treatment, and finishing for high-load parts, but avoid over-specifying simple low-stress hardware.
- Ask suppliers to define inspection plans and PPM targets, especially for high-volume orders where the ten-thousandth part must match the first.
- Prioritize OEM partners with automated CNC capacity and testing equipment to reduce rework, stabilize lead times, and improve supply reliability.
Frequently Asked Questions
Why does CNC precision matter for angle grinder accessories?
Angle grinders can run above 11,000 RPM, so small errors in runout, thread fit, or balance can cause vibration, bearing wear, or unsafe disc movement. CNC machining helps keep critical dimensions consistent across pressure plates, conversion joints, and wheel adapters.
Which angle grinder accessory sizes should buyers specify?
Buyers should define the target tool type and standard size, such as 100, 125, 150, 180, or 230. They should also confirm thread type, bore size, thickness, material grade, surface finish, and packaging requirements before placing an OEM order.
When are forging and heat treatment necessary?
Forging and heat treatment are best for rotating or high-load parts that need strength, fatigue resistance, and stable clamping performance. Simpler low-stress parts may be produced by stamping or cold heading to control cost without overengineering.
How can OEM production improve supply efficiency?
OEM CNC production improves efficiency through repeatable machining, automated inspection, and integrated processes such as forging, machining, heat treatment, and finishing. This reduces rework, stabilizes lead times, and supports large-volume orders with consistent quality.
What defect rate should buyers discuss with suppliers?
For high-volume CNC orders, buyers should discuss measurable quality targets such as PPM limits, inspection frequency, and acceptance criteria. Advanced production lines may aim for defect rates below common targets such as 500 PPM, depending on part complexity.