


Factory-Direct Angle Grinder Pressure Plates for Bulk Buyers: Cold Heading vs. CNC Turning Cost Structure at 100K Units
TL;DR
- We manufacture angle grinder pressure plates in-house using both cold heading and CNC turning, so we can offer transparent cost comparisons at 100K-unit volumes.
- Cold heading delivers a lower per-unit forming cost for axisymmetric pressure plate geometries because we produce finished shapes from wire feedstock in a single high-speed die cycle.
- CNC turning excels when our customers require tight geometric tolerances, non-standard thread profiles, or custom bore dimensions that cold heading cannot achieve without secondary operations.
- At the 100K-unit threshold, the raw-material utilization gap between the two processes becomes the dominant cost driver in our factory.
- By sourcing factory-direct from our Yuyao facility, bulk buyers eliminate distributor markups and gain direct access to our engineering team for design-for-manufacturing reviews before we commit tooling.
When our bulk-buying customers ask us which production method yields the most competitive unit price for angle grinder pressure plates at high volumes, we always start with the same question: what does the part geometry demand? In our experience, the answer is never purely about cost — it is about matching process capability to functional requirements while keeping material waste, cycle time, and secondary operations in check. We have spent years operating both cold heading lines and CNC turning centers side by side in our Yuyao factory, and we want to share what we have learned so that procurement teams can make informed sourcing decisions.
In this article we walk through the cost structure of each process at the 100K-unit production run level, explain where the break-even points shift, and show how our vertically integrated approach as a custom precision forged power tool components manufacturer allows us to optimize total landed cost for buyers worldwide.
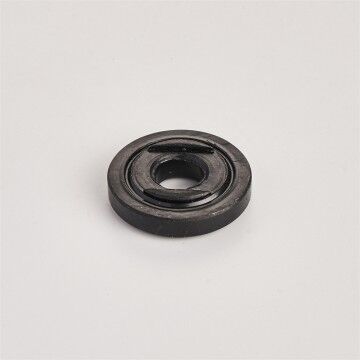
Understanding the Two Core Manufacturing Processes
Before we compare dollar-for-dollar cost breakdowns, we want to make sure our readers share a common understanding of what each process involves. Both cold heading and CNC turning are mature metal forming technologies that we run daily on our shop floor, but they approach part creation from fundamentally different directions.
Cold Heading: High-Speed Forming from Wire
In our cold heading operation, we feed straightened steel wire into a multi-station progressive die. Each station punches, extrudes, or upsets the material incrementally until the final pressure plate geometry emerges. The entire cycle happens at room temperature — no heating furnace required — which means we preserve the grain structure of the base steel and achieve excellent fatigue resistance without a post-forming heat treatment step. Our cold heading machines run at 80 to 200 parts per minute depending on plate diameter, which gives us the throughput advantage that makes high-volume orders economically attractive. For readers unfamiliar with the underlying science, the Wikipedia article on cold heading provides a solid technical primer.
What we value most about cold heading for angle grinder pressure plates is the material utilization rate. Because the wire feedstock is already close to the final cross-section, our scrap rate on a typical upper and lower pressure plate run stays below five percent. That efficiency compounds at 100K units and translates directly into lower per-part material cost for our customers.
CNC Turning: Precision Machining from Bar Stock
Our CNC turning centers take a different approach. We clamp round bar stock in a chuck, spin it at high RPM, and use programmable tool paths to cut the pressure plate profile, bore, and thread features in a single setup or across two turrets on our Swiss-type lathes. This subtractive process gives us extraordinary control over dimensional accuracy — we routinely hold ±0.01 mm on critical bore diameters and ±0.02 mm on concentricity, which matters when a pressure plate must mate precisely with an angle grinder adapter or conversion rod.
The trade-off is material waste. Turning a pressure plate from bar stock generates continuous chips that we collect and recycle, but the effective buy-to-fly ratio on a typical disc pressure plate can reach 40 to 55 percent. At 100K units that scrap delta becomes a meaningful line item, and it is the primary reason cold heading often wins on pure cost when the geometry permits it.
Cost Structure Breakdown — Cold Heading at 100K Units
We want to walk through each cost element that our production planning team accounts for when we quote a 100K-unit cold heading order for a standard angle grinder cutting disc pressure plate. The structure below reflects what we see in our own factory; other manufacturers may weight these categories differently.
| Cost Category | Cold Heading (100K Units) | Key Consideration |
|---|---|---|
| Raw material (wire coil) | Largest single cost driver | We purchase in bulk from local Ningbo steel suppliers, passing mill-rate savings to our buyers |
| Tooling (progressive dies) | Amortized across full run | Die life on our carbide tooling typically exceeds 500K hits, so at 100K units the per-part tooling cost stays minimal |
| Machine time + labor | Low per-part overhead | Our operators monitor multiple machines simultaneously thanks to automated feeding and ejection |
| Secondary operations | Optional thread rolling or deburring | We roll M10 threads in-line for pressure plate conversion kits without leaving the heading cell |
| Quality inspection | In-line sampling + final AQL | We use optical comparators and go/no-go gauges at the machine; our QC team references ISO metric thread standards for every threaded variant |
| Scrap / rework | Below 5% on typical runs | We track die wear in real time to catch dimensional drift before out-of-tolerance parts accumulate |
When our customers consolidate multiple pressure plate SKUs into a single blanket order, we can further distribute the die changeover time across the run. Our scheduling team batches diameters and thicknesses to minimize setup frequency, which is a practical advantage that we only achieve at the 100K-unit scale.
Cost Structure Breakdown — CNC Turning at 100K Units
Our CNC turning cost model shares several line items with the cold heading model, but the weighting shifts dramatically. Below we lay out what our engineering team accounts for when a customer specification calls for turned pressure plates at the same 100K-unit volume.
| Cost Category | CNC Turning (100K Units) | Key Consideration |
|---|---|---|
| Raw material (bar stock) | Higher per-part material cost | Bar stock costs more per kilogram than wire coil, and our chip yield adds hidden material expense |
| Cutting tools | Carbide inserts with scheduled replacement | We index inserts at predictable intervals and track tool life in our MES to avoid unplanned downtime |
| Machine time + labor | Longer cycle per part | A typical pressure plate takes 25–45 seconds on our CNC lathes versus sub-second on our cold headers |
| Secondary operations | Often minimal — thread cut in same setup | Our sub-spindle lathes complete back-side features without a second chucking, reducing handling cost |
| Quality inspection | CMM probing + statistical process control | We run in-process CMM checks on every 50th part and log data for full lot traceability |
| Scrap / rework | Typically 2–3% reject rate | Our CNC programs include automatic tool wear compensation to keep parts in tolerance across long runs |
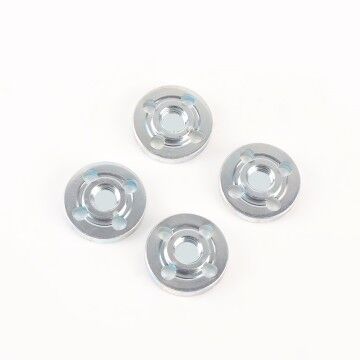
Where the Break-Even Shifts — Material Utilization and Cycle Time
Our production planners have modeled dozens of pressure plate geometries, and the pattern is consistent. For standard disc pressure plates with simple M10 bores and uniform wall thickness, cold heading wins on total cost since the material utilization advantage (95%+ versus 45–55%) overwhelms every other variable at 100K units. The underlying principles of forging — shaping metal without removing it — inherently produce less waste than subtractive machining.
However, we have seen the calculus reverse in specific scenarios. When a customer specifies a pressure plate with an eccentric bore, a stepped outer profile, or a tolerance band tighter than ±0.03 mm on concentricity, our CNC turning cells deliver the geometry in a single pass without the secondary grinding or milling that cold heading would require. In those cases, the cost of adding a secondary operation to the headed part erases the material savings, and CNC turning becomes the more economical path.
We guide every bulk buyer through this analysis before we commit to a production method. Our engineering team runs a DFM (design for manufacturing) review on the customer's drawing, calculates the total processing cost under both scenarios, and presents the comparison with clear assumptions. This transparency sets us apart as a precision hardware manufacturer that partners with buyers rather than quoting parts.
Tooling Investment and Amortization at Scale
Tooling cost is where many bulk buyers get tripped up as the upfront numbers look starkly different between the two processes. A set of cold heading progressive dies for a standard angle grinder pressure plate represents a moderate NRE (non-recurring engineering) investment that we amortize across the full production run. At 100K units, the per-part tooling contribution is negligible — often less than a fraction of a cent per piece.
CNC turning, by contrast, uses standard carbide inserts and modular tool holders that we already stock in our tool crib. The per-part tooling cost for a turned pressure plate is technically near zero in NRE terms, but the consumable insert cost per part is higher than the die-wear cost per part in cold heading. Our tooling engineers track insert consumption rates and optimize cut parameters so that we minimize insert changes without compromising surface finish or tolerance.
For buyers placing repeat orders beyond the initial 100K-unit run, our cold heading tooling continues to amortize further. We store dedicated dies for every active SKU in our tool room, which means a reorder triggers no additional tooling charge once the initial NRE is paid. This is a practical advantage we offer to long-term partners who maintain consistent part specifications across annual blanket orders.
Surface Finish, Tolerance, and Functional Performance
Our customers use angle grinder pressure plates in demanding environments — angle grinders spin at 10,000+ RPM, and the pressure plate must clamp cutting discs or grinding wheels without vibration or slippage. That means surface finish and flatness matter as much as dimensional accuracy.
In our cold heading process, the as-formed surface typically achieves Ra 1.6–3.2 µm, which is more than adequate for the clamping function of a pressure plate. The forging action compresses surface grain, producing a work-hardened outer layer that resists wear. For most standard applications — 100 mm, 115 mm, 125 mm, 150 mm, and 180 mm grinder models — we find that our cold headed plates meet OEM specifications without any surface finishing step.
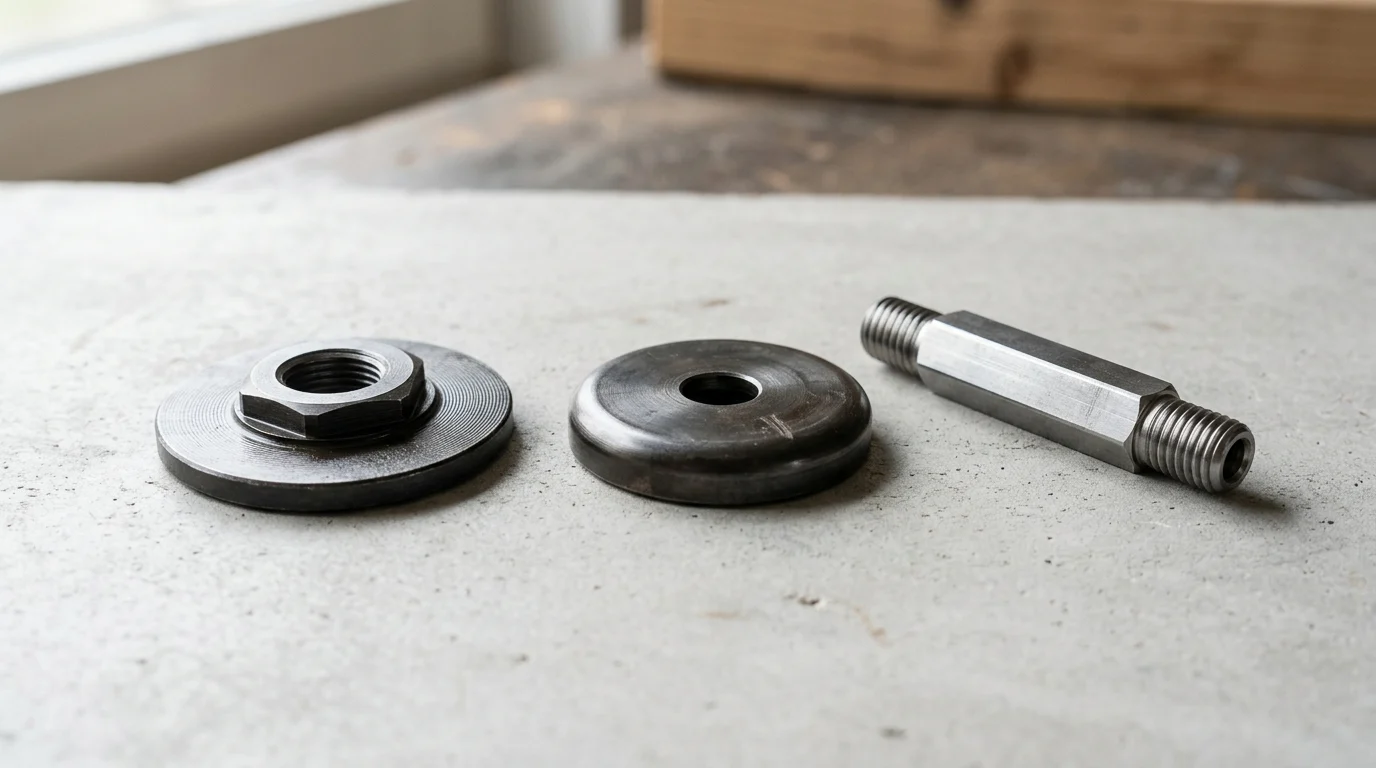
Our CNC-turned plates achieve Ra 0.8–1.6 µm as-machined, which gives them a slight edge in aesthetic quality and a measurably smoother contact surface. When a customer needs a pressure plate for a premium tool line where visual finish and packaging presentation matter, we recommend our CNC-turned option. We also offer optional polishing for customers wanting a mirror-like surface on their polishing and conversion joint accessories.
Flatness tolerance is another area where we differentiate. Cold headed pressure plates typically hold flatness within 0.05 mm across the clamping face, while our CNC-turned plates achieve 0.02 mm or better. For most angle grinder applications, 0.05 mm flatness is well within functional limits, but we provide the data so customers can decide which specification tier their end users require.
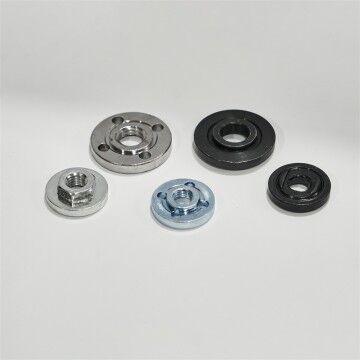
Quality Control and Compliance at 100K-Unit Volumes
Quality assurance at scale requires more than spot-checking a handful of parts from each batch. We have built our QC infrastructure around the principle that every pressure plate we ship must meet the same dimensional and metallurgical standards regardless of whether it was cold headed or CNC turned. Our internal quality control protocols draw on industry procedures and align with international standards.
For cold heading runs, we perform first-article inspection on the initial 50 parts, then shift to a statistical sampling plan (typically AQL 1.0 or tighter) for the remainder of the lot. Our optical comparators verify profile geometry, our thread gauges confirm M10 thread pitch and major diameter per ISO metric thread specifications, and our hardness testers spot-check the work-hardened surface layer to ensure it meets our fatigue-resistance targets.
For CNC turning runs, we integrate Renishaw probing into our machine cycles to measure critical dimensions on every part without operator intervention. We log every measurement in our MES (manufacturing execution system), which gives us full lot traceability and allows our customers to request dimensional data for any individual part in a shipment. This level of documentation is especially valued by our European and North American buyers who supply into regulated industrial supply chains.
In both processes, we maintain compliance with DIN standards and applicable regional safety requirements. Our customers rely on us to provide certificates of conformity, material test reports, and dimensional inspection sheets with every shipment.
Supply Chain Advantages of Factory-Direct Sourcing
We operate our production lines in Yuyao, Ningbo — one of China's most established hardware manufacturing clusters. Our location gives us immediate access to raw material suppliers, heat treatment shops, plating facilities, and a deep pool of skilled operators. When a bulk buyer sources directly from our factory, the entire supply chain compresses into a single point of accountability.
We eliminate intermediary markups that accumulate when parts pass through trading companies or distributors. Our export team handles documentation, customs declarations, and logistics coordination directly, so our customers receive factory pricing without sacrificing service quality. We encourage prospective buyers to review our full product catalog to see the breadth of pressure plate variants and related accessories we produce.
Our 40+ fully automatic CNC machines and cold heading lines run in parallel, which means we can split a large order across both processes when a customer's order includes multiple pressure plate geometries. Some SKUs go to the cold heading cell, others to the CNC lathes, and we ship everything in a consolidated container. This flexible production allocation is something only a vertically integrated factory like ours can offer, and it is a key reason we maintain long-term relationships with distributors and tool brands across global markets.
For buyers needing related accessories — such as electric drill conversion extension rods or hydraulic fittings and pipe brush assemblies — we consolidate these items into the same shipment, reducing per-unit freight cost and simplifying import logistics.
How We Help Bulk Buyers Choose the Right Process
Every bulk buyer we work with has a slightly different set of priorities. Some optimize purely on unit cost; others prioritize tolerance capability or surface finish. We have developed a structured consultative process that walks our customers through the decision framework before we quote a single part.
First, we review the customer's drawing to assess whether the geometry suits cold heading. If the part is rotationally symmetric with uniform wall thickness, cold heading is our starting point. If it has eccentric features or tight concentricity requirements, we recommend CNC turning. Second, we model the total cost at the target volume — including raw material, tooling amortization, machine time, labor, inspection, and scrap — and present a transparent comparison table. Third, we discuss lead time: cold heading dies add setup time on the initial order but flow quickly on reorders, while CNC turning programs faster initially but has longer per-unit cycles. We help our customers weigh these trade-offs against their inventory planning.
We invite procurement teams evaluating factory direct angle grinder pressure plate suppliers to contact our sales engineering team for a no-obligation DFM review. We share our manufacturing insights freely since we believe informed buyers become long-term partners.
Frequently Asked Questions
Q1: What is the minimum order quantity for factory-direct angle grinder pressure plates from your facility?
A: We accept orders starting from 1,000 pieces for CNC-turned plates and 5,000 pieces for cold headed plates. However, the 100K-unit threshold discussed in this article is where our cost optimization truly shines as tooling amortization and material bulk-purchase pricing reach their most favorable levels. For smaller trial orders, we recommend our CNC turning process to avoid the upfront die investment.
Q2: Can you produce pressure plates to custom dimensions that are not listed in your standard catalog?
A: Yes. We specialize in custom manufacturing and can produce pressure plates to your exact drawing specifications. Our engineering team reviews every custom request for manufacturability and will recommend the optimal process — cold heading, CNC turning, or a hybrid approach — based on your geometry, tolerance, and volume requirements. Visit our custom precision forged components page for more details on our capabilities.
Q3: What steel grades do you use for cold headed vs. CNC-turned pressure plates?
A: For cold heading, we typically use low-carbon and medium-carbon steels (such as SWRCH10K, SWRCH15K, and 10B21 boron steel) that deform cleanly at room temperature and respond well to thread rolling. For CNC turning, we work with a broader range including 45# carbon steel, 40Cr alloy steel, and stainless steel variants depending on the customer's corrosion-resistance and strength requirements. We select the grade during our DFM review based on the end-use application.
Q4: How do you handle thread quality on cold headed M10 pressure plates?
A: We form M10 threads using a dedicated thread-rolling station that is integrated into our cold heading cell. Thread rolling — as opposed to thread cutting — displaces material rather than removing it, which produces threads with superior fatigue strength and a smoother surface finish. Our thread-rolled M10 profiles conform to ISO metric thread Class 6g tolerance, which satisfies the vast majority of angle grinder OEM specifications worldwide.
Q5: What is the typical lead time for a 100K-unit order of cold headed pressure plates?
A: From the point of order confirmation, our standard lead time is 25–35 calendar days for a 100K-unit cold heading run. This includes die setup and tuning (5–7 days), full production run (10–15 days), quality inspection and packaging (3–5 days), and export documentation (2–3 days). Reorders of the same SKU typically ship within 15–20 days since the dies are already tooled and tested.
Q6: Do you provide samples before committing to a full production run?
A: We always provide first-article samples for customer approval before we begin mass production. For cold heading orders, we produce 20–30 sample pieces from the actual die so that the customer can evaluate dimensional accuracy, surface finish, and fit with mating components. For CNC turning, we typically ship 10–15 samples from the production program. We encourage our buyers to test these samples rigorously against their assembly and performance requirements before giving us the green light.
Q7: Can you combine pressure plates with other angle grinder accessories in a single shipment?
A: Absolutely. We manufacture a full range of angle grinder accessories including cutting disc pressure plates, flange kits, conversion rods, adapters, and extension rods — all under one roof. Consolidating multiple SKUs into a single container shipment reduces per-unit freight cost and simplifies our customers' import and warehousing operations. Our sales team can build a custom bundle quotation based on your specific accessory mix.
Q8: How does your factory ensure worker safety during high-volume cold heading operations?
A: We follow machine guarding and workplace safety practices aligned with international standards. Our cold heading cells are fully enclosed with interlocked safety guards, and our operators receive regular training on lockout/tagout procedures and emergency protocols. We maintain a safe working environment as we believe that a well-run factory is a safe factory — our production quality depends on it. Buyers can reference OSHA machine guarding guidelines as a benchmark for the safety standards we uphold.
Q9: What payment terms do you offer for bulk orders?
A: For new customers, we typically work with a 30% deposit upon order confirmation and 70% balance before shipment (T/T terms). For established partners with a proven order history, we offer more flexible terms including L/C at sight and extended T/T arrangements. We discuss payment structures on a case-by-case basis during our quotation process.
Q10: Do you hold certifications relevant to international markets?
A: Our factory operates under a documented quality management system, and we provide material certificates, dimensional inspection reports, and certificates of conformity with every shipment. We produce to DIN, ISO, and customer-specific standards. For buyers requiring third-party inspection, we welcome SGS, TÜV, or Bureau Veritas inspectors at our facility.
About the Author
Keke Huang
CEO at Yuyao Guling Hardware Co., Ltd.
Keke Huang leads Yuyao Guling Hardware Co., Ltd., a precision forging and metal forming manufacturer based in Yuyao, Ningbo — one of China's most established hardware production clusters. With a focus on mid-to-high-end electric tool accessories, Guling operates 40+ fully automatic CNC machines and cold-heading lines producing angle grinder pressure plates, flange kits, conversion joints, hydraulic fittings, and pipe brush assemblies for industrial buyers worldwide. Keke oversees product development, factory operations, and export strategy, working with distributors and tool brands across global markets to deliver consistent quality from a vertically integrated production facility.
Ready to Source Factory-Direct Angle Grinder Pressure Plates?
Our engineering team will review your drawing, recommend the optimal manufacturing process, and deliver a transparent cost breakdown — no obligation, no middleman.
Contact Us TodayFor more technical articles and product updates, visit our News section.