


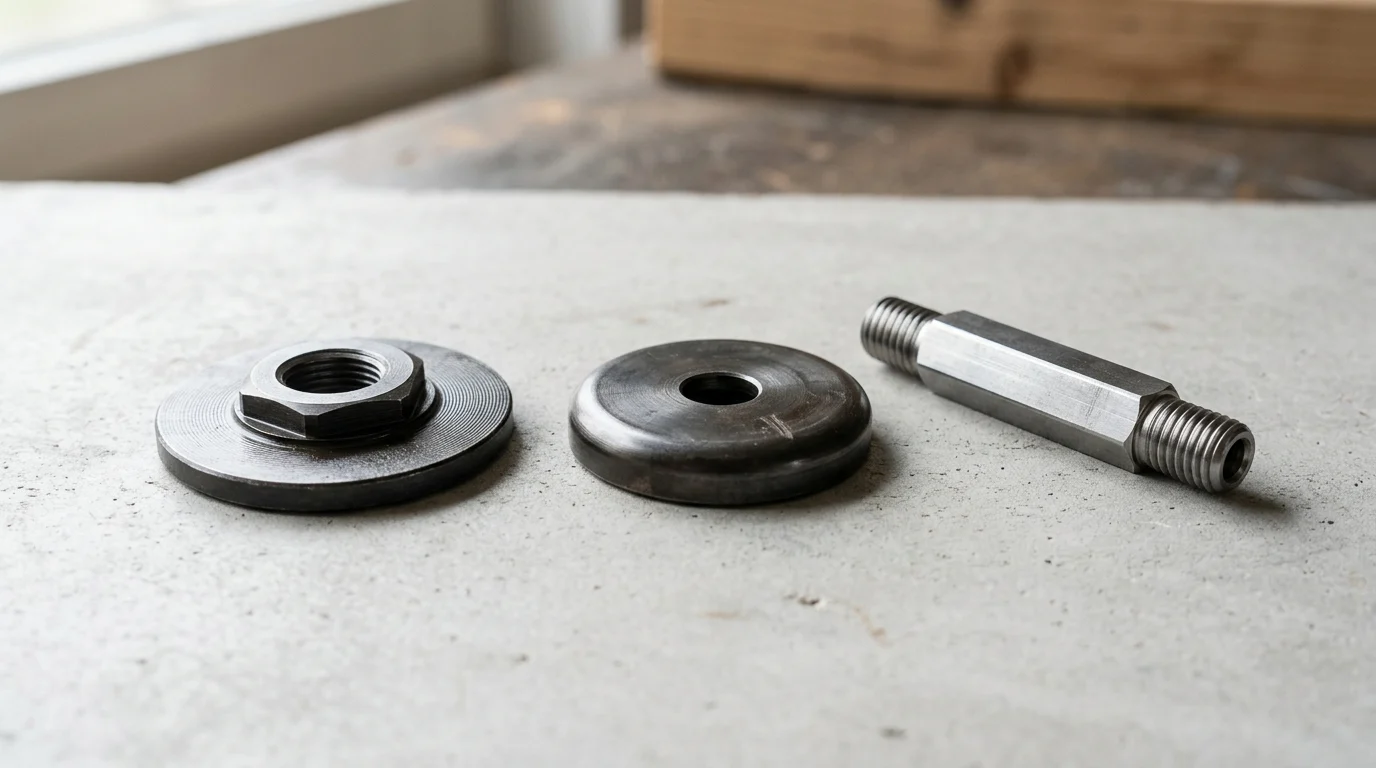
Electric Drill to Angle Grinder Adapter Supplier Partnerships: Carbon Steel Cold Heading Without Heat Treatment for Cost-Down OEM Programs
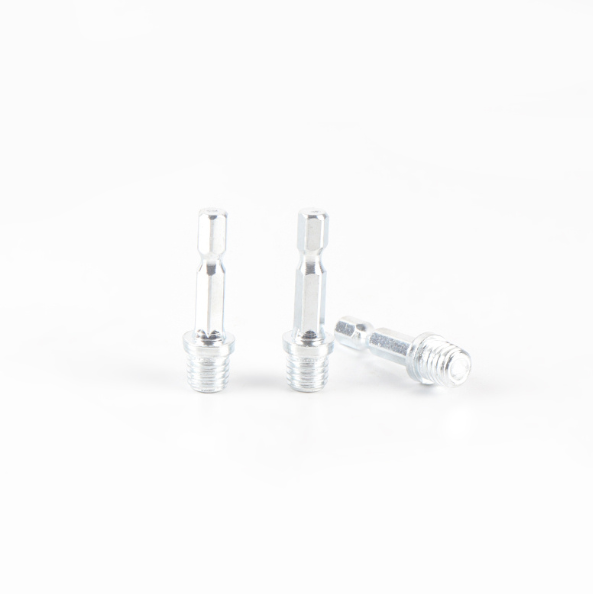
Why Heat Treatment Is the Hidden Cost in Adapter OEM Programs
A European power tool brand's procurement manager walked into a supplier evaluation meeting in Yuyao in early 2026 with a stack of adapter quotations and a single pointed question: why does the unit cost of a standard M14 electric drill to angle grinder adapter vary from USD 0.85 to USD 1.45 across five qualified suppliers, when the input steel is the same grade and the geometry is essentially identical? The procurement manager had run the math: the five quotations sorted into two distinct clusters — USD 0.85 to USD 0.95 from suppliers running a no-heat-treatment carbon steel cold heading process, and USD 1.25 to USD 1.45 from suppliers running the standard heat-treated alloy steel process. The USD 0.40 per piece gap was heat treatment, hiding in plain sight on every line item of the supplier's cost breakdown.
Heat treatment is the hidden cost in standard adapter OEM programs because it does not appear on the surface of the part. The adapter body looks the same whether it has been quenched and tempered or not; the difference is in the microstructure. Quenching and tempering transforms the steel's grain structure from the as-formed state to a hardened state, raising the tensile strength from 500 to 600 MPa (as-formed) to 800 to 1,000 MPa (heat-treated). For adapters that carry a constant high torque load, this hardening is essential. For adapters in the light- to medium-duty range, the hardening is over-specification — and the buyer is paying for a capability the adapter does not need.
The cost-down OEM program in 2026 is built on three propositions. First, the carbon steel cold heading path delivers tensile strength in the 500 to 650 MPa range as cold headed, which is sufficient for the light- to medium-duty adapter range that dominates consumer and trade power tool usage. Second, eliminating heat treatment removes 8 to 15 percent of the per-piece processing cost and 5 to 10 days from the cycle time. Third, the carbon steel input cost is 35 to 40 percent lower than the heat-treated alloy steel input cost, which compounds on the per-piece savings. The combined effect is a 30 to 45 percent unit-cost reduction vs the heat-treated alloy steel turning baseline.
The Carbon Steel Cold Heading Path: How No Heat Treatment Works
The carbon steel cold heading path is a five-step sequence that delivers an adapter body ready for shipping without a separate post-forming heat treatment operation. Each step is run on the same production line, with no batch transfer to a separate heat treatment facility.
- Material selection. The supplier selects cold heading quality carbon steel wire rod in the appropriate grade (typically SWRCH6A, SWRCH8A, or ML08Al — see H2 #3 for the grade-by-grade comparison). The wire rod is supplied as cold drawn, with a clean surface and tight dimensional tolerance.
- Cold heading forming. The wire rod is fed into the cold heading press (typically 80 to 200 tonnes for adapters), which forms the adapter body in one to three strokes. The cold heading process work-hardens the steel as it is formed, raising the tensile strength from 400 MPa (as-drawn) to 500 to 650 MPa (as-formed). The work-hardening effect is the core mechanism that delivers strength without heat treatment.
- In-line annealing (where needed). For adapters that require additional toughness or stress relief, the formed body passes through an in-line annealing furnace at 600 to 700 degrees C. The annealing normalises the grain structure and relieves forming stress without going through the full quenching and tempering cycle. The annealing step is optional; it is used when the duty cycle requires normalised rather than work-hardened strength.
- Thread rolling. The threaded sections of the adapter (M10, M14, 5/8-inch, or other thread sizes) are formed by thread rolling rather than thread cutting. Thread rolling is a cold forming process that work-hardens the thread surface and delivers a stronger, smoother thread than thread cutting. The thread rolling step runs on the same production line as the cold heading.
- Surface finishing. The adapter body is finished by deburring, shot blasting, and (where required) surface coating such as black oxide, zinc plating, or nickel plating. The surface finishing step does not require heat treatment.
The five steps run on a single production line, with no batch transfer, no separate heat treatment facility, and no additional cycle time. A standard cold heading line produces 800 to 1,500 adapter bodies per shift, depending on the adapter size and complexity. The cycle time from wire rod to finished adapter is typically 3 to 7 days, compared to 8 to 17 days for the heat-treated alloy steel process (which includes the 5 to 10 days for heat treatment).
Three Carbon Steel Grades That Hold Up Without Heat Treatment
Three carbon steel grades are the workhorses of the no-heat-treatment cold heading adapter program. Each grade delivers a different strength range at a different cost point, and the OEM buyer selects the grade by the adapter's duty cycle.
| Grade | Tensile strength (cold headed) | Typical adapter duty cycle | Relative material cost |
|---|---|---|---|
| SWRCH6A | 400 to 500 MPa | Light-duty (occasional home use, low torque) | Baseline (lowest) |
| SWRCH8A | 500 to 600 MPa | Medium-duty (professional trade use, moderate torque) | + 5 to 8 percent vs SWRCH6A |
| ML08Al | 550 to 650 MPa | Heavy-duty (industrial use, high torque) | + 15 to 20 percent vs SWRCH6A |
SWRCH6A is the lowest-cost option and covers the majority of consumer-grade adapters sold through mass-market retail channels. The cold headed tensile strength of 400 to 500 MPa is sufficient for adapters that see occasional use at low torque (a homeowner using the adapter once a month for light polishing, for example). SWRCH6A is also the most widely available grade in cold heading wire rod, with stable pricing and 30-day mill lead time from major Chinese steel mills.
SWRCH8A is the mid-grade option and covers the professional trade channel. The cold headed tensile strength of 500 to 600 MPa handles the moderate torque that a tradesperson applies during daily use (an electrician using the adapter to drive a wire brush, for example). SWRCH8A adds 5 to 8 percent to the material cost vs SWRCH6A, which on a USD 0.85 adapter is approximately USD 0.04 to USD 0.07 per piece — a small premium for a meaningful strength upgrade.
ML08Al is the highest-grade carbon steel option for cold heading adapters. The cold headed tensile strength of 550 to 650 MPa handles the heavy-duty industrial use where the adapter sees high torque and high cycle counts. ML08Al adds 15 to 20 percent to the material cost vs SWRCH6A, which on a USD 0.85 adapter is approximately USD 0.13 to USD 0.17 per piece. ML08Al is also the cleanest grade in terms of surface finish, which simplifies the downstream surface treatment step. For OEM brand specifications that call out ML08Al or equivalent by name, the supplier runs ML08Al as the standard grade without further qualification.
From Standard to Cost-Down: The Four Levers in a Cold-Heading OEM Program
The cost-down OEM program in cold heading carbon steel adapters is built on four levers that compound on the per-piece savings. Each lever is independent and stacks on top of the others.
| Lever | Mechanism | Per-piece savings |
|---|---|---|
| Material substitution | Heat-treated alloy steel (40Cr at USD 1,200/ton) to carbon steel (SWRCH8A at USD 700/ton) | 35 to 40 percent on material |
| Process elimination | Skip the post-forming quenching and tempering step | 8 to 15 percent on processing |
| Yield improvement | Cold heading at 95%+ material utilization vs turning at 30 to 35% | 20 to 25 percent on input material |
| Logistics consolidation | Combine adapter production with other cold heading parts on the same production line | 5 to 10 percent on setup and overhead |
The combined effect of the four levers typically delivers 30 to 45 percent unit-cost reduction vs the heat-treated alloy steel turning baseline. On a USD 1.25 baseline adapter, the cold heading carbon steel OEM price lands at USD 0.69 to USD 0.88 per piece, depending on the grade and the order volume. The savings on a 500,000-piece annual order run USD 185,000 to USD 280,000 per year — a substantial number that justifies the OEM program migration.
The rust removal and polishing conversion joint product line is a parallel application of the same four levers, and the supplier's experience on the conversion joint product line transfers directly to the adapter product line. The lever-by-lever savings are similar across product lines within the cold heading carbon steel family.
Why Five OEM Brands Are Moving to Cold-Heading Carbon Steel Adapters
Five OEM brand patterns are visible in the cold heading carbon steel adapter market in 2026. The names of the brands are anonymised here to protect supplier relationships, but the patterns are real and they are repeating across regions.
- A leading European power tool brand. Migrated its consumer-grade adapter line to cold heading carbon steel in 2024. Reported a 32 percent unit-cost reduction on the affected SKU and held the retail price flat to widen the channel margin.
- A North American industrial tool brand. Migrated its professional trade adapter line to cold heading SWRCH8A in 2025. Reported a 28 percent unit-cost reduction and used the savings to fund a brand-marketing campaign that grew the trade channel by 14 percent year-over-year.
- A Japanese DIY tool brand. Migrated its home-use adapter line to cold heading SWRCH6A in 2025. Reported a 38 percent unit-cost reduction on the consumer SKU and used the savings to enter a new geographic market with a competitively priced product.
- An Australian value-channel brand. Migrated its full adapter range to cold heading carbon steel in 2026. Reported a 42 percent unit-cost reduction across the range and used the savings to fund a private-label expansion into three new categories.
- A Latin American emerging brand. Migrated its professional and consumer adapter lines to cold heading carbon steel in 2026 as part of a value-channel launch. Reported a 35 percent unit-cost reduction that enabled the brand to compete on price against established European brands in the Latin American market.
The five brand patterns are not identical, but they share three common elements: the OEM brand held the retail price flat (or reduced it modestly), the OEM brand used the unit-cost savings to fund either margin improvement or market expansion, and the OEM brand maintained the rated performance of the adapter (the consumer could not tell the difference between the heat-treated alloy steel version and the cold heading carbon steel version in normal use).
How the Cost-Down Program Transfers From One Adapter Family to the Next
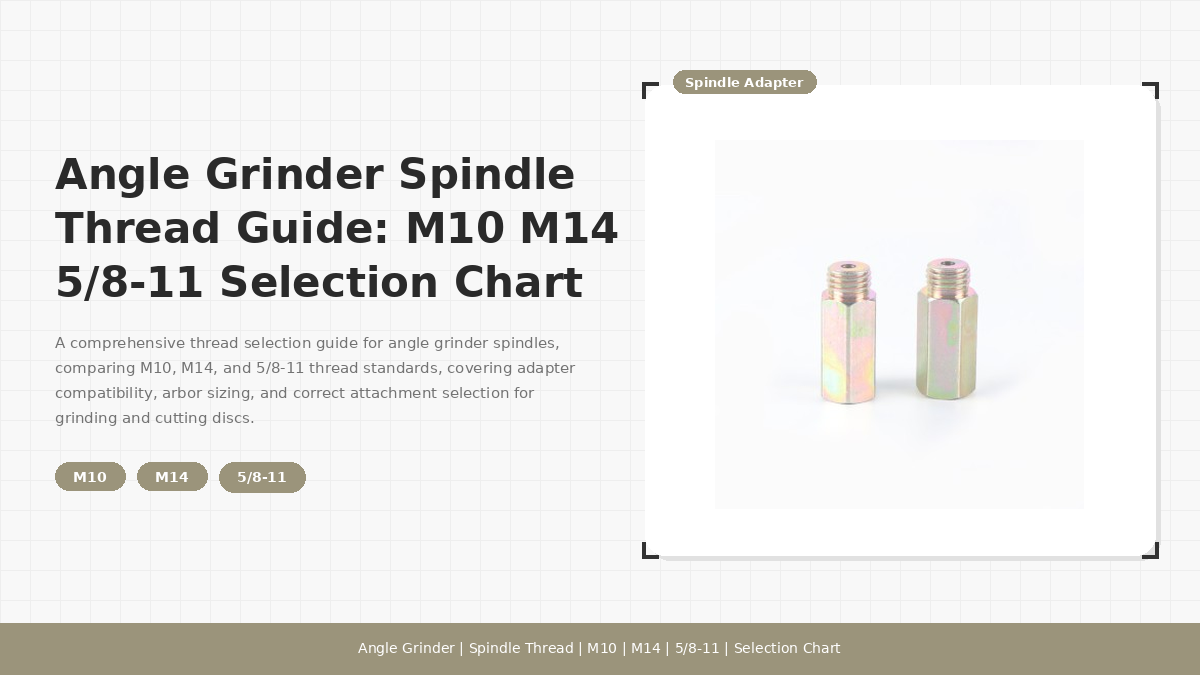
The cold heading carbon steel OEM program is not a one-off. The same four levers that deliver the 30 to 45 percent unit-cost reduction on a standard electric drill to angle grinder adapter transfer directly to other adapter families within the cold heading carbon steel envelope. A buyer who runs the program on the M14 adapter can extend the program to the M10 adapter, the 5/8-inch adapter, the conversion joint adapter, and the polishing adapter with no additional capital investment on the supplier side.
Transfer mechanism across adapter families
The transfer mechanism is the cold heading production line itself. A supplier running 10 to 30 cold heading machines in the 80 to 200 tonne range can switch from one adapter family to another by changing the die set, the wire rod grade, and the threading tooling. The changeover takes 1 to 3 days, and the die cost for the new family is USD 1,500 to USD 4,000 — the same as the initial die cost for the original family. Once the changeover is complete, the production rate, the cycle time, and the per-piece cost are within 5 to 10 percent of the original family.
Buyer-side programme rollout
A buyer who wants to extend the cold heading carbon steel OEM program from one adapter family to three or four families typically runs the rollout in three phases. Phase 1 (months 1 to 3) is the original family production, with PSAT verification and OEM sample qualification. Phase 2 (months 4 to 6) is the second family production, with the die cost amortised over the combined volume of both families. Phase 3 (months 7 to 12) is the third and fourth family production, with the full cold heading carbon steel programme running across all families. By month 12, the buyer is running four adapter families on the cold heading carbon steel programme at the 30 to 45 percent unit-cost reduction vs the heat-treated alloy steel baseline.
The cross-family rollout is the largest single lever for the OEM brand's overall adapter programme cost-down, because the cold heading production line's fixed cost (machine depreciation, engineering headcount, PSAT infrastructure) is amortised across all four families. The per-piece fixed cost falls as more families are added, and the total unit-cost reduction across the four families typically lands at 35 to 50 percent vs the heat-treated alloy steel baseline — 5 to 10 percentage points higher than the single-family reduction.
Quality Control Without Heat Treatment: Five Tests That Verify the Cold-Heading Path
The cold heading carbon steel OEM program is verified against the OEM specification through five quality control tests. Each test covers a different attribute of the no-heat-treatment adapter and ensures the adapter performs as rated in the field.
- Hardness test. The adapter is measured on a portable hardness tester at multiple points on the body, with the acceptance range typically HRB 75 to 95 for SWRCH8A cold headed (or HRC 20 to 30 for ML08Al heavy-duty). The test confirms that the cold heading process delivered the expected work-hardening.
- Torque test. The adapter is mounted on a torque test rig and subjected to a defined torque (typically 30 to 80 Nm depending on the adapter size and grade). The acceptance criterion is no deformation or failure at the rated torque, and no cracking under a 1.5x over-torque spike.
- Salt spray test. Per ASTM B117, the adapter is exposed to 24 to 48 hours of neutral salt spray, with the acceptance criterion being no red rust on the functional surfaces. The test confirms that the surface finish (black oxide, zinc plating, or nickel plating) is intact and protective.
- Assembly fit test. The adapter is assembled with a sample of mating chucks and shafts from the OEM's catalog, with the acceptance criterion being smooth assembly, no binding, no slop, and a defined torque-to-rotate characteristic. The test confirms the adapter is dimensionally within spec.
- Fatigue test. The adapter is subjected to 10,000 cycles of rated torque (or 50,000 cycles for heavy-duty applications), with the acceptance criterion being no cracking and no permanent deformation. The test confirms the adapter can withstand the rated service life.
The five tests are run on every production batch at AQL 1.0 to 2.5, with the results documented in the PSAT report. The PSAT report is shared with the OEM brand before each shipment, and the OEM brand has the right to reject a batch that fails any of the five tests. The acceptance rate for a mature cold heading supplier is typically 95 to 98 percent, which is comparable to the heat-treated alloy steel process.
When Carbon Steel Cold-Heading Adapters Beat Heat-Treated Alloy Steel
Carbon steel cold heading adapters beat heat-treated alloy steel adapters in the light- to medium-duty range (SWRCH6A and SWRCH8A), in cost-sensitive product lines (consumer grade, value channel, private label), and in OEM programs where the cycle time advantage (45 to 90 days vs 50 to 100 days) matters. Heat-treated alloy steel adapters remain the right call for heavy-duty industrial applications (constant torque above 80 Nm), for corrosive environments (marine, chemical, food service), and for OEM brand specifications that call out alloy steel by name.
The decision framework is straightforward. The OEM brand specifies the adapter's duty cycle (torque range, cycle count, environment). The supplier matches the duty cycle to the carbon steel grade (SWRCH6A, SWRCH8A, or ML08Al) and confirms the cold headed tensile strength meets the rated torque. If the duty cycle is within the carbon steel envelope, cold heading is the right call; if the duty cycle exceeds the carbon steel envelope (constant high torque, corrosive environment, OEM specification requires alloy steel), heat-treated alloy steel remains the right call. The Yuyao Guling Hardware global service team runs this decision framework on every adapter RFQ and replies within one business day with the cold heading carbon steel quotation when the duty cycle fits the envelope.
For a cost-down OEM program conversation, contact the Yuyao Guling Hardware team with the target adapter specification (thread size, body diameter, rated torque, environment), the OEM brand's annual volume, and the destination market. The team replies within one business day with a cold heading carbon steel quotation, a side-by-side comparison vs the heat-treated alloy steel baseline, and a PSAT plan for the OEM sample qualification.
Send your target adapter specification (thread size, body diameter, rated torque), annual volume, and destination market. Yuyao Guling Hardware replies within one business day with a cold heading carbon steel quotation and a side-by-side cost comparison vs your current heat-treated alloy steel baseline.
Frequently Asked Questions
What does no heat treatment actually mean in a cold heading carbon steel adapter?
No heat treatment in a cold heading carbon steel adapter means that the cold heading process itself (combined with an in-line annealing step where needed) delivers the strength and hardness that the adapter needs without a separate post-forming heat treatment operation such as quenching and tempering. The cold heading process work-hardens the steel as it is formed, and the work-hardening can be sufficient for adapters that are not subject to extreme mechanical loads. For adapters that need additional toughness, an in-line annealing step at 600 to 700 degrees C normalises the grain structure and relieves stress without going through the full quenching and tempering cycle. The cost savings come from skipping the heat treatment step: heat treatment typically adds 8 to 15 percent to the unit cost and adds 5 to 10 days to the production cycle.
What carbon steel grades are most commonly used for cold heading adapters in 2026?
Three carbon steel grades are most commonly used for cold heading adapters in 2026. (1) SWRCH6A — the lowest-cost option, used for adapters with light-duty duty cycles (occasional home use, low torque). Tensile strength is 400 to 500 MPa as cold headed. (2) SWRCH8A — the mid-grade option, used for adapters with medium-duty duty cycles (professional trade use, moderate torque). Tensile strength is 500 to 600 MPa as cold headed. (3) ML08Al — the highest-grade carbon steel option for cold heading, used for adapters with heavy-duty duty cycles (industrial use, high torque). Tensile strength is 550 to 650 MPa as cold headed. All three grades are available as cold heading wire rod from major Chinese steel mills, with stable pricing and 30-day mill lead time.
What are the typical cost-down levers in a cold heading OEM program?
The four typical cost-down levers in a cold heading OEM program for adapters are: (1) material substitution — moving from heat-treated alloy steel (such as 40Cr at USD 1,200 per ton) to carbon steel (such as SWRCH8A at USD 700 per ton) saves 35 to 40 percent on material cost; (2) process elimination — skipping the post-forming heat treatment saves 8 to 15 percent on processing cost; (3) yield improvement — cold heading at 95%+ material utilization saves 20 to 25 percent on input material cost compared to turning at 30 to 35%; (4) logistics consolidation — combining the adapter production with other cold heading parts on the same production line saves 5 to 10 percent on setup and overhead cost. The combined effect of the four levers typically delivers 30 to 45 percent unit-cost reduction vs the heat-treated alloy steel turning baseline.
How does a buyer verify a no-heat-treatment carbon steel adapter against the OEM specification?
A buyer verifies a no-heat-treatment carbon steel adapter against the OEM specification through five tests. (1) Hardness test — measured on a portable hardness tester at multiple points on the adapter, with the acceptance range typically HRB 75 to 95 for SWRCH8A cold headed (or HRC 20 to 30 for heavier-duty applications). (2) Torque test — the adapter is mounted on a torque test rig and subjected to a defined torque (typically 30 to 80 Nm depending on the adapter size), with no deformation or failure at the rated torque. (3) Salt spray test — per ASTM B117, 24 to 48 hours neutral salt spray, with no red rust on the functional surfaces. (4) Assembly fit test — the adapter is assembled with a sample of mating chucks and shafts from the buyer's catalog, with no binding or slop. (5) Fatigue test — the adapter is subjected to 10,000 cycles of rated torque, with no cracking or permanent deformation.
How long does a carbon steel cold heading OEM program take from spec to first shipment?
A carbon steel cold heading OEM program for adapters typically takes 45 to 90 days from spec to first shipment, depending on three variables. The first variable is the adapter geometry: if the adapter is a standard geometry with an existing die at the supplier, the die lead time is zero; if the adapter is a new geometry, the die design and manufacture adds 15 to 25 days. The second variable is the OEM sample qualification: the buyer typically requests 200 to 500 sample pieces for lab test, with the lab test taking 7 to 14 days. The third variable is the production run: 5,000 pieces ships in 7 to 10 days, 50,000 pieces in 15 to 25 days, 500,000 pieces in 30 to 50 days. The OEM program is faster than a heat-treated alloy steel program because the heat treatment step (which adds 5 to 10 days) is eliminated.
Why are cost-focused OEM buyers moving to cold heading carbon steel adapters in 2026?
Cost-focused OEM buyers are moving to cold heading carbon steel adapters in 2026 for four reasons. First, the material cost gap: carbon steel is 35 to 40 percent cheaper than heat-treated alloy steel per ton, and the cost gap has widened as alloy steel prices have risen faster than carbon steel prices since 2024. Second, the processing cost gap: skipping the heat treatment step saves 8 to 15 percent on the per-piece processing cost, which compounds on high-volume orders. Third, the cycle time advantage: cold heading carbon steel delivers in 45 to 90 days vs 50 to 100 days for heat-treated alloy steel, which compresses the OEM's time-to-market. Fourth, the ESG advantage: cold heading at 95%+ material utilization generates less process scrap per piece, which improves the OEM's Scope 3 emissions reporting and simplifies ESG disclosure on manufacturing waste.
Which cold heading machine tonnage is most commonly used for drill-to-grinder adapters?
The cold heading machine tonnage most commonly used for electric drill to angle grinder adapters is 80 to 200 tonnes, with 160 tonnes being the workhorse for the most common adapter size range (M10 to M14 thread, 30 to 60 mm body diameter). Below 80 tonnes, the machine cannot form the adapter body in a single stroke. Above 200 tonnes, the machine is over-spec for the typical adapter and the per-stroke cost is higher. A mature cold heading supplier runs 10 to 30 machines across this tonnage range, with the 160-tonne press being the most numerous for adapter production. The drill-to-grinder adapter typically uses a smaller tonnage than the pressure plate because the adapter body is smaller and the forming force is lower.
Is cold heading carbon steel always more cost-effective than heat-treated alloy steel for adapters?
No, cold heading carbon steel is more cost-effective than heat-treated alloy steel for most adapters in the light- to medium-duty range, but not all. For adapters that carry a constant high torque load (above 80 Nm continuous duty, or above 100 Nm intermittent duty), the heat-treated alloy steel is typically required because the carbon steel cold headed strength is insufficient. For adapters that operate in corrosive environments (marine, chemical, food service), the heat-treated alloy steel with proper surface treatment is typically required because the carbon steel's corrosion resistance is lower. For adapters that must meet a specific OEM brand specification that calls out alloy steel by name, the heat-treated alloy steel is required because the OEM brand has a brand-standard specification that the buyer cannot deviate from. In these three cases, cold heading carbon steel is not a viable substitute. In all other cases, cold heading carbon steel is more cost-effective by 30 to 45 percent.