


Deep-Cavity Grinding Extension Rod ODM Development: From Standard Angle Grinders to Extended-Reach Multi-Function Tool Adaptation
An industrial tool designer at a North American power tool brand owner was tasked with launching a deep-cavity grinding extension rod line for the marine hull cleaning and aerospace interior surface preparation segments. The first ODM partner proposed a 200mm fixed-length rod with M14-to-M10 thread adapter — simple, fast, but limited to 1 end-effector (grinding disc only). The second ODM partner proposed a 400mm modular rod with quick-change end-effector mount — 2x the engineering complexity, 6-week longer development, but adaptable to grinding + sanding + polishing + wire brush. The brand owner initially chose the first partner for speed, but 4 months later was forced to redesign the rod when the marine customer's specification changed to require a 350mm length with a polishing bonnet end-effector. The second partner's proposal would have absorbed the specification change without re-engineering. This guide is the field-tested version of how an ODM buyer should evaluate the deep-cavity grinding extension rod development workflow — and why the multi-function, modular design typically outperforms the single-end-effector, fixed-length design in 24-month lifecycle cost.
This guide is built around the ODM development workflow used by power tool accessory designers launching deep-cavity grinding extension rod programs with vertically integrated Chinese factories like Yuyao Guling Hardware Co., Ltd. — a precision forging and metal forming manufacturer operating 40+ fully automatic CNC machines and cold-heading lines, with in-house heat treatment, CNC machining, zinc plating, and badging / packaging capability for a true forging-to-surface-treatment OEM line.
The 3 application segments for deep-cavity grinding extension rods
Deep-cavity grinding extension rods serve 3 distinct application segments, each with different length requirements, different end-effector requirements, and different operating RPM requirements. The ODM buyer should specify the target segment first (industrial maintenance, marine hull cleaning, or aerospace interior surface preparation) and then design the extension rod around the segment's specification. The 3 segments are not interchangeable — a rod designed for industrial maintenance typically cannot meet the aerospace interior surface preparation's weight and balance specifications without re-engineering.
Segment 1 — Industrial maintenance. Industrial maintenance is the largest segment by unit volume but the most price-sensitive. The applications include engine cylinder bore surface preparation, pipe interior cleaning, container tank interior surface finishing, and mold cavity polishing. The typical extension rod length is 150-300mm, the typical shaft diameter is 8-10mm, the typical end-effector is a grinding disc or sanding pad, and the typical operating RPM is 6,000-10,000 RPM. The typical material is 45# medium carbon steel with zinc plating. The typical MOQ is 1,000-5,000 units annually.
Segment 2 — Marine hull cleaning. Marine hull cleaning is the medium segment by unit volume but the most corrosion-sensitive. The applications include fiberglass hull surface preparation, antifouling paint removal, and below-waterline surface finishing. The typical extension rod length is 300-450mm, the typical shaft diameter is 10-12mm, the typical end-effector is a wire brush or polishing bonnet, and the typical operating RPM is 4,000-6,000 RPM. The typical material is 304 stainless steel or 45# with marine-grade nickel plating. The typical MOQ is 200-1,000 units annually.
Segment 3 — Aerospace interior surface preparation. Aerospace interior surface preparation is the smallest segment by unit volume but the most specification-sensitive. The applications include aircraft cabin interior surface finishing, composite material surface preparation, and aerospace component finishing. The typical extension rod length is 200-400mm, the typical shaft diameter is 6-8mm (the lighter rod for fatigue reduction during long reach operations), the typical end-effector is a polishing bonnet or sanding pad, and the typical operating RPM is 4,000-6,000 RPM. The typical material is 40Cr alloy steel or 304 stainless steel with electroless nickel plating. The typical MOQ is 100-500 units annually.
The 3 segments have different lot sizes, different unit prices, and different engineering requirements. The ODM buyer should commit to the primary segment first (industrial maintenance for high-volume / standard specification, marine hull cleaning for medium-volume / corrosion-resistant specification, aerospace interior for low-volume / precision specification) and treat the other 2 segments as secondary markets that may require secondary product variants. The OEM development cost is amortized most efficiently when the brand owner commits to a primary segment with annual volume of 1,000+ units.
The 6-step ODM development workflow
The ODM development workflow for a deep-cavity grinding extension rod is a 6-step engineering process that takes 12-18 weeks from RFQ approval to first article inspection at a vertically integrated OEM. The 6 steps are documented below with the typical duration and the typical deliverable for each step. The 6-step workflow is the ODM buyer's engineering framework for managing the OEM relationship and verifying the engineering depth at each step.
| Step | Activity | Duration | Deliverable |
|---|---|---|---|
| 1. Specification alignment + engineering design | Confirm length, diameter, end-effector mount, thread interface, surface treatment, segment target | 3-4 weeks | Signed technical specification + 3D CAD model + prototype plan |
| 2. Shaft forging + heat treatment | Forging die setup, sample forging, heat treatment per BS EN 10083-3 | 3-4 weeks | Forged + heat-treated sample with hardness certificate |
| 3. CNC machining of thread ends | CNC turning + threading for proximal angle grinder interface and distal end-effector mount | 2-3 weeks | Machined sample with dimensional report + thread gauge certification |
| 4. Surface treatment (plating) | Zinc / nickel / chrome plating per BS EN ISO 1456 | 2-3 weeks (parallel with step 3) | Plated sample with salt spray test certificate per BS EN ISO 9227 |
| 5. FAT + dynamic balance verification | Dynamic balance testing at extended operating RPM, plus dimensional + hardness + salt spray verification | 2-3 weeks | FAT report with dynamic balance data + badging pre-production sample |
| 6. Production lot preparation | Production line scheduling, component pre-order, QC plan finalization | 2 weeks | Production lot schedule with first-article trigger |
The dynamic balance verification in Step 5 is the highest-leverage engineering step in the workflow. Unlike a standard angle grinder flange where the dynamic balance test is straightforward (concentricity at the flange face), the deep-cavity extension rod has a longer lever arm (150-600mm) that amplifies any run-out at the distal end. The permissible run-out at the distal end of the rod is typically 0.10-0.20mm at the extended operating RPM (vs 0.02-0.05mm for a standard flange), and the dynamic balance test must be conducted on the rod + end-effector assembly (not just the rod alone) to verify the actual operating performance. The ODM buyer should witness the dynamic balance test on-site and verify the run-out data is included on the lot-specific test certificate.
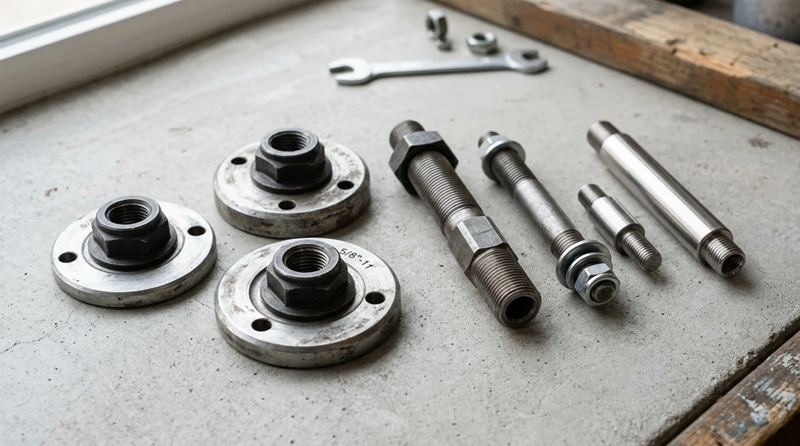
The thread interface specification in Step 1 is the second highest-leverage engineering decision. The thread interface determines the angle grinder compatibility — M14 male thread for medium industrial angle grinders (the most common global standard), M10 male thread for small angle grinders (e.g., 115mm / 4.5 inch), and 5/8-11 UNC male thread for North American angle grinders. The ODM buyer should specify the thread interface based on the target market — M14 for global / European / Asian markets, 5/8-11 for North American markets, M10 for small angle grinder / DIY markets. The thread interface should be verified with a thread gauge per ISO 1502 (for M14 / M10) or ANSI B1.1 (for 5/8-11 UNC) at the OEM's QC lab.
The end-effector mount specification in Step 1 is the third highest-leverage engineering decision. The end-effector mount determines the multi-function capability of the rod — a fixed M10 female thread on the distal end accepts only 1 end-effector type (e.g., a grinding disc with M10 male thread), while a quick-change hex adapter (typically 1/4" hex or 3/8" hex) accepts multiple end-effector types (grinding disc + sanding pad + polishing bonnet + wire brush + flap disc). The ODM buyer should specify the end-effector mount based on the target segment's flexibility needs — fixed M10 thread for industrial maintenance (single end-effector), quick-change hex for marine hull cleaning and aerospace interior (multiple end-effectors).
The fixed-length single-end-effector vs. modular multi-end-effector trade-off
The deep-cavity grinding extension rod design faces a fundamental engineering trade-off between fixed-length single-end-effector (simple, fast, low cost) and modular multi-end-effector (complex, slow, higher cost). The trade-off is not about which design is "better" — it is about which design matches the ODM buyer's target segment's specification stability over the 24-month product lifecycle. The decision rule is: if the target segment's specification change frequency is below 30% per year, choose the fixed-length design; if the specification change frequency is above 50% per year, choose the modular design.
Design A — Fixed-length single-end-effector. The fixed-length design has a single length (typically 150-300mm) and a single end-effector mount (typically M10 female thread for a grinding disc). The OEM development timeline is 12-14 weeks, the engineering cost is 1x baseline, and the per-unit cost is the lowest in the segment. The fixed-length design is appropriate for industrial maintenance where the rod is used for a single application (e.g., engine cylinder bore surface preparation) and the specification does not change frequently. The fixed-length design is NOT appropriate for marine hull cleaning or aerospace interior surface preparation where the same rod may need to handle grinding, sanding, polishing, and wire brushing in different applications.
Design B — Modular multi-end-effector. The modular design has a multi-length capability (typically 300-600mm with intermediate couplers) and a quick-change end-effector mount (typically 1/4" hex or 3/8" hex adapter). The OEM development timeline is 16-18 weeks, the engineering cost is 2-3x baseline (due to the modular couplers and the quick-change mount), and the per-unit cost is 30-50% higher than the fixed-length design. The modular design is appropriate for marine hull cleaning and aerospace interior surface preparation where the same rod may need to handle 4-5 end-effector types in different applications. The modular design is also appropriate for industrial maintenance brand owners who want to launch a single SKU that covers multiple applications.
The 24-month lifecycle cost comparison typically favors the modular design for the marine hull cleaning and aerospace interior segments. The reason is the specification change frequency — the marine hull cleaning segment sees a 50-70% specification change rate per year (new end-effector types, new length requirements, new OEM angle grinder interfaces), and the aerospace interior segment sees a 40-60% specification change rate per year. With a fixed-length design, each specification change requires a new OEM development cycle (12-14 weeks + $15,000-$30,000 engineering cost + new production lot setup). With a modular design, each specification change only requires a new end-effector adapter (4-6 weeks + $3,000-$5,000 engineering cost + small lot production). The cumulative cost over 24 months is typically 30-50% lower for the modular design in high-change-frequency segments.
The 3 application-form matrices: length × diameter × end-effector
The 3 application-form matrices summarize the deep-cavity grinding extension rod specifications across the 3 target segments. Each matrix maps the segment's typical application depth, the typical rod length, the typical shaft diameter, and the typical end-effector mount. The ODM buyer should use the matrices to align the rod specification with the target segment's requirements before locking the OEM development specs. The matrices are not prescriptive — they are engineering starting points that the ODM buyer should adjust based on the specific customer's requirements.
| Matrix | Segment | Application depth | Rod length | Shaft diameter | End-effector mount | Operating RPM |
|---|---|---|---|---|---|---|
| Matrix 1 — Industrial maintenance | Engine cylinder bore, pipe interior, container tank, mold cavity | 100-300mm cavity depth | 150-300mm | 8-10mm | M10 female thread (fixed, single end-effector) | 6,000-10,000 RPM |
| Matrix 2 — Marine hull cleaning | Fiberglass hull, antifouling paint removal, below-waterline surface | 300-500mm cavity depth | 300-450mm | 10-12mm | 1/4" hex quick-change (multi end-effector) | 4,000-6,000 RPM |
| Matrix 3 — Aerospace interior | Aircraft cabin, composite material, aerospace component | 200-400mm cavity depth | 200-400mm | 6-8mm (lightweight) | 1/4" hex or 3/8" hex quick-change (multi end-effector) | 4,000-6,000 RPM |
Matrix 1 (industrial maintenance) is the highest-volume matrix and the most cost-sensitive. The ODM buyer should optimize the rod design for cost-efficiency — using 45# medium carbon steel with zinc plating (the standard industrial specification), fixed M10 female thread end-effector mount (single end-effector), and the standard 8-10mm shaft diameter. The OEM development should focus on the production cost (forging setup, machining setup, plating setup) and the lead time (12-14 weeks for the standard OEM development timeline). The dynamic balance verification is at the standard 0.05-0.10mm run-out limit at the operating RPM.
Matrix 2 (marine hull cleaning) is the medium-volume matrix and the most corrosion-sensitive. The ODM buyer should optimize the rod design for corrosion resistance — using 304 stainless steel or 45# with marine-grade nickel plating (the marine specification), 1/4" hex quick-change end-effector mount (multi end-effector for grinding + sanding + polishing + wire brush), and the heavier 10-12mm shaft diameter. The OEM development should focus on the surface treatment (nickel plating ≥ 10μm per ASTM B733 with 240+ hour NSS salt spray rating per BS EN ISO 9227) and the modular coupler engineering. The dynamic balance verification is at the 0.10-0.15mm run-out limit at the extended operating RPM.
Matrix 3 (aerospace interior) is the lowest-volume matrix and the most specification-sensitive. The ODM buyer should optimize the rod design for weight reduction and fatigue resistance — using 40Cr alloy steel or 304 stainless steel with electroless nickel plating (the aerospace specification), 1/4" hex or 3/8" hex quick-change end-effector mount (multi end-effector for polishing + sanding), and the lightweight 6-8mm shaft diameter. The OEM development should focus on the fatigue testing (the rod must withstand 10,000+ hours of operation without fatigue failure) and the dimensional precision (ISO 2768 medium grade). The dynamic balance verification is at the 0.05-0.10mm run-out limit at the extended operating RPM.
Thread compatibility analysis: M14 / M10 / 5/8-11 UNC
The deep-cavity grinding extension rod's thread compatibility with the angle grinder is determined by the proximal end thread specification. The 3 standard thread specifications cover the global market — M14 for medium industrial angle grinders (most common global standard), M10 for small angle grinders (e.g., 115mm / 4.5 inch), and 5/8-11 UNC for North American angle grinders. The ODM buyer should specify the thread interface based on the target market — the M14 is the most common thread specification globally and should be the default choice unless the target market is exclusively North American (where 5/8-11 UNC is the dominant standard).
The thread interface specification must be verified with a thread gauge per ISO 1502 (for M14 / M10) or ANSI B1.1 (for 5/8-11 UNC) at the OEM's QC lab. The thread gauge certification should be included on the lot-specific test certificate with the thread specification, the thread gauge reading, the pass/fail result, and the inspector signature. The thread gauge certification is the ODM buyer's verification that the rod's proximal end thread will actually fit the target market's angle grinder, not just match the specification on paper.
The thread interface specification interacts with the end-effector mount specification. The combination of M14 proximal + M10 distal allows the rod to be used with a medium industrial angle grinder and a small grinding disc (the most common combination for industrial maintenance). The combination of 5/8-11 UNC proximal + 1/4" hex distal allows the rod to be used with a North American angle grinder and a quick-change end-effector system (the most common combination for marine hull cleaning). The ODM buyer should specify the proximal + distal thread combination based on the target market's angle grinder + end-effector combination, not just the proximal thread alone.
The 3 material options for the deep-cavity extension rod shaft
The deep-cavity grinding extension rod's shaft material determines the operating performance, the corrosion resistance, and the per-unit cost. The 3 standard material options are 45# medium carbon steel (per BS EN 10083-3 C45 grade), 40Cr alloy steel, and 304 stainless steel. The ODM buyer should select the material based on the target segment's load requirements, the corrosion exposure, and the per-unit cost target. The 3 material options are not interchangeable — a 45# rod cannot be upgraded to 304 stainless without re-engineering the shaft diameter and the end-effector mount.
Material 1 — 45# medium carbon steel (per BS EN 10083-3 C45 grade). 45# is the standard industrial material for general-purpose deep-cavity grinding extension rods. The 45# rod has a tensile strength of 600-750 MPa, a yield strength of 350-450 MPa, and a hardness of HRC 20-25 in the as-forged state (with HRC 35-45 achievable through heat treatment). The 45# rod is suitable for industrial maintenance applications with HRC 35-45 heat treatment and zinc plating ≥ 8μm per BS EN ISO 1456. The per-unit cost is the lowest in the segment. The 45# rod is NOT suitable for marine hull cleaning or aerospace interior applications due to the corrosion sensitivity.
Material 2 — 40Cr alloy steel. 40Cr is the higher-load material for industrial maintenance and aerospace interior applications. The 40Cr rod has a tensile strength of 800-950 MPa, a yield strength of 550-650 MPa, and a hardness of HRC 45-50 in the quenched and tempered state. The 40Cr rod is suitable for aerospace interior surface preparation with the high fatigue resistance required for 10,000+ hour operation. The 40Cr rod is also suitable for industrial maintenance with the higher load demand. The per-unit cost is 30-50% higher than the 45# rod.
Material 3 — 304 stainless steel. 304 stainless is the corrosion-resistant material for marine hull cleaning and food-grade applications. The 304 rod has a tensile strength of 500-650 MPa, a yield strength of 200-300 MPa, and a hardness of HRC 15-20 in the annealed state (with HRC 30-35 achievable through cold working). The 304 rod is suitable for marine hull cleaning with the corrosion resistance required for seawater exposure. The 304 rod is also suitable for food-grade applications (e.g., food processing equipment surface preparation) with the FDA / LFGB compliance. The per-unit cost is 3-5x higher than the 45# rod.
When NOT to ODM (the 3 deal-breaker scenarios)
ODM development is not the right commercial model for every deep-cavity grinding extension rod scenario. There are 3 deal-breaker scenarios where the power tool brand owner should consider standard product sourcing rather than ODM development. Identifying these scenarios before the OEM development saves the ODM buyer 6-12 months of program delay.
Deal-breaker scenario 1 — Annual purchasing volume below 100 units. A brand owner with annual purchasing volume below 100 units cannot amortize the ODM development cost (typically $15,000-$30,000 for the engineering design, forging die setup, and FAT process) across enough units to justify the program. The break-even point for an ODM deep-cavity grinding extension rod program is approximately 100-200 units per year. Below 100 units, the standard product sourcing (using an existing OEM's catalog deep-cavity rod) is the lower total-cost option.
Deal-breaker scenario 2 — Target market requires proprietary OEM brand on the rod. Some target markets (notably aerospace OEM and defense) require the OEM brand on the rod and may reject ODM-developed rods regardless of the engineering specification compliance. In these markets, the OEM brand premium is the customer's purchasing requirement, and an ODM-developed rod — even with identical engineering specifications — will not win the business. The brand owner should stay with the OEM-branded supply in these markets.
Deal-breaker scenario 3 — Specification is locked to a single customer's proprietary design. Some customers (notably large aerospace prime contractors) require the deep-cavity rod to be designed to a proprietary specification that cannot be re-used for other customers. In this scenario, the ODM development cost cannot be amortized across multiple brand-owner programs and the unit cost becomes prohibitive. The brand owner should consider the customer-funded ODM development model where the customer pays for the engineering design and the production lot setup.
The 3 deal-breaker scenarios cover approximately 20-25% of the deep-cavity grinding extension rod market. The remaining 75-80% are candidates for ODM development if the brand owner can commit to a primary segment with annual volume of 100+ units. The ODM buyer should run the deal-breaker screen first (week 0), then run the 6-step ODM development workflow (weeks 1-16), then commit to the production lot (weeks 17-18). The total ODM development timeline is 16-18 weeks and produces a defensible OEM development with documented engineering and FAT evidence.
Engineering takeaway: modular design wins on lifecycle cost for high-change-frequency segments
The most important lesson from the fixed-length vs. modular design trade-off is that the ODM buyer is not buying a deep-cavity grinding extension rod at a unit price — they are buying a 24-month lifecycle cost profile that depends on the target segment's specification change frequency. A fixed-length design that costs 30-50% less per unit but requires a new OEM development cycle for each specification change is more expensive over 24 months than a modular design that costs 30-50% more per unit but absorbs specification changes with a new end-effector adapter. The lifecycle cost analysis is the engineering basis for the modular design decision, and the specification change frequency is the engineering input.
For ODM buyers evaluating Chinese power tool accessory OEMs like Yuyao Guling Hardware — a precision forging and metal forming manufacturer with 40+ fully automatic CNC machines and cold-heading lines, in-house heat treatment, in-house CNC machining, in-house zinc plating, and the 3-stage testing capability (pressure + dynamic balance + salt spray) for the extension rod's surface treatment and dynamic balance verification — the ODM development should follow a six-step framework: (1) specification alignment + engineering design (3-4 weeks); (2) shaft forging + heat treatment (3-4 weeks); (3) CNC machining of thread ends (2-3 weeks); (4) surface treatment (2-3 weeks, parallel with step 3); (5) FAT + dynamic balance verification (2-3 weeks); (6) production lot preparation (2 weeks). The framework is the ODM buyer's verification tool for the engineering depth and the lot-specific test certificate discipline.
For ODM buyers beginning a deep-cavity grinding extension rod program, the recommended starting point is a rust removal and polishing conversion joint ODM engagement to confirm the OEM's ODM development workflow and the multi-function end-effector mount capability. For ODM buyers evaluating the angle grinder adapter compatibility, the buy best angle grinder adapter suppliers ODM reference provides the thread compatibility framework. For ODM buyers specifying the proximal end interface, the custom precision forged power tool components development catalog provides the forging and machining capability baseline for the ODM program.
ODM questions on deep-cavity grinding extension rod development
What is a deep-cavity grinding extension rod and what is it used for?
A deep-cavity grinding extension rod is a power tool accessory that extends the reach of a standard angle grinder by 150-600mm, allowing the operator to grind, sand, or polish inside deep cavities (e.g., engine cylinder bores, pipe interiors, container tanks, mold cavities) that are inaccessible with a standard angle grinder. The extension rod interfaces with the angle grinder's M14 or M10 or 5/8-11 UNC arbor thread on the proximal end, and carries a smaller diameter shaft (typically 6mm / 8mm / 10mm) on the distal end that mounts the grinding disc, sanding pad, or polishing bonnet. The extension rod is typically used for industrial maintenance, marine hull cleaning, and aerospace interior surface preparation.
What is the OEM development timeline for a deep-cavity grinding extension rod?
The OEM development timeline for a deep-cavity grinding extension rod is 12-18 weeks from RFQ approval to first article inspection: 3-4 weeks for specification alignment and engineering design (length, diameter, thread interface, end-effector mount), 3-4 weeks for shaft forging and heat treatment, 2-3 weeks for CNC machining of the thread ends and any specialized features, 2-3 weeks for surface treatment (zinc plating, nickel plating, or chrome plating), 2-3 weeks for FAT (Factory Acceptance Test) including dynamic balance verification at the extended operating RPM, and 2 weeks for production lot preparation. The OEM development timeline is typically 2-4 weeks longer than for a standard power tool accessory due to the dynamic balance verification at the extended length.
What is the difference between a standard angle grinder extension rod and a multi-function tool extension rod?
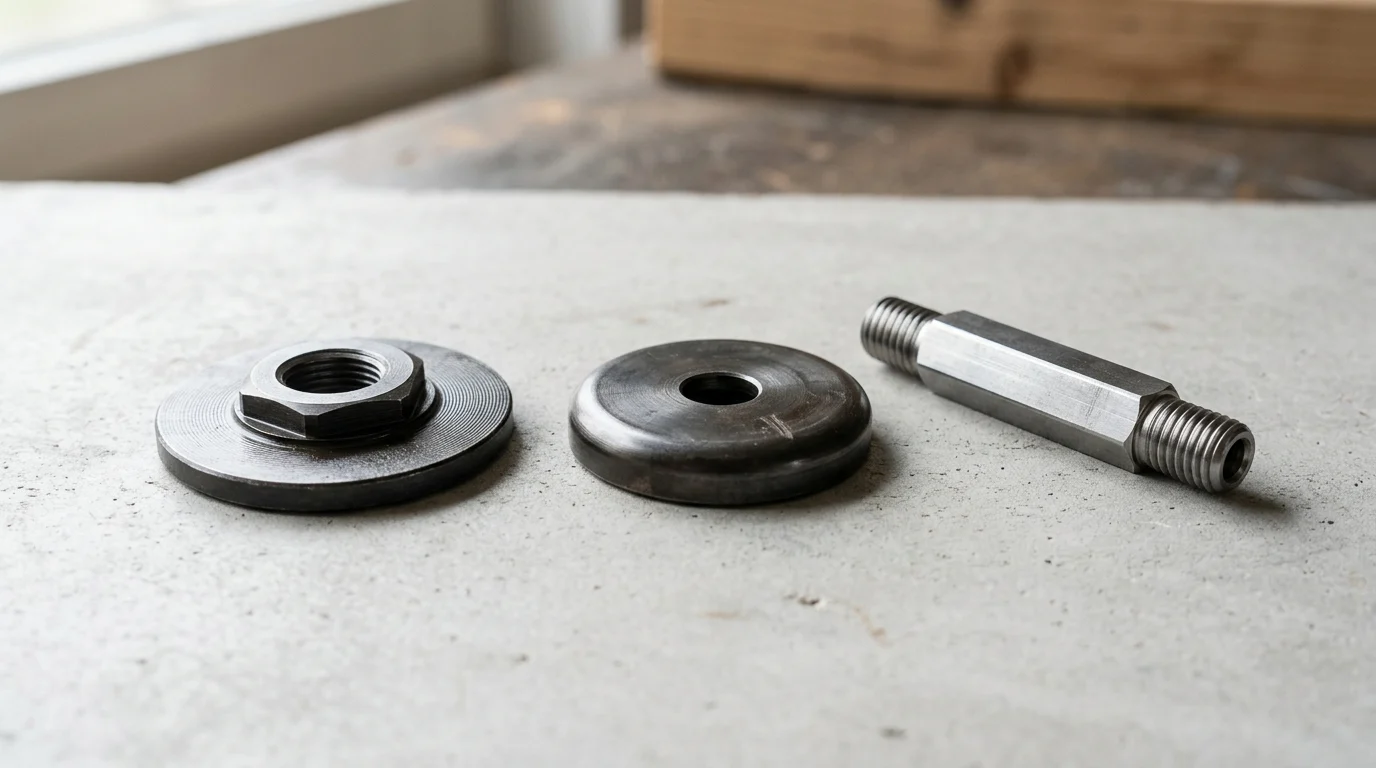
A standard angle grinder extension rod is designed for a single end-effector type (typically a grinding disc or sanding pad) and a fixed length (typically 150-300mm). A multi-function tool extension rod is designed for multiple end-effector types (grinding disc + sanding pad + polishing bonnet + wire brush + flap disc) and a modular length (typically 300-600mm with intermediate couplers). The multi-function rod requires a quick-change end-effector mount (e.g., M10 female thread on the distal end with a hex adapter) and a higher torque capacity to handle the wider range of end-effector loads. The OEM development complexity is 2-3x higher for the multi-function rod due to the modular design and the wider end-effector compatibility.
What materials are used for deep-cavity grinding extension rods?
Deep-cavity grinding extension rods are typically made from 45# medium carbon steel (per BS EN 10083-3 C45 grade) for general industrial applications, 40Cr alloy steel for higher-load applications, or 304 stainless steel for marine / food-grade applications requiring corrosion resistance. The shaft is typically 6-12mm diameter depending on the length and the operating load. The proximal end (angle grinder interface) is typically M14 male thread for medium industrial angle grinders, M10 male thread for small angle grinders, or 5/8-11 UNC for North American angle grinders. The distal end (end-effector interface) is typically M10 female thread or hex adapter for the grinding disc / sanding pad.
How do you verify the dynamic balance of a deep-cavity grinding extension rod?
The dynamic balance of a deep-cavity grinding extension rod is verified on a balancing machine at the OEM's QC lab, with the test conducted at the extended operating RPM (typically 6,000-10,000 RPM for grinding applications, 4,000-6,000 RPM for sanding applications). The permissible run-out is typically 0.10-0.20mm at the distal end of the rod (vs 0.02-0.05mm for a standard flange), reflecting the longer lever arm of the extension rod. The dynamic balance test is conducted on the rod + end-effector assembly (not just the rod alone) to verify the actual operating performance. The run-out data is recorded on the lot-specific test certificate with the test RPM, the run-out limit, the measured run-out, and the pass/fail result.
What is the MOQ for ODM deep-cavity grinding extension rods?
The MOQ for ODM deep-cavity grinding extension rods from a vertically integrated Chinese OEM is typically 100-300 units for a pilot run with custom length and end-effector mount, and 500-1,000 units for a launch run with full private-label badging and packaging. The MOQ is lower than standard power tool accessories (typically 200/500/2,000 unit tiers) because the extension rod is a longer / more specialized product with a narrower market. The per-unit price drops 15-20% from the 100-300 unit pilot tier to the 500-1,000 unit launch tier, and another 10-15% from the 500-1,000 to 2,000+ unit scale tier.