


Deep-Cavity Grinding Extension Rod ODM Development: From Standard Angle Grinders to Extended-Reach Multi-Function Tool Adaptation
Why Deep-Cavity Grinding Needs an Extension Rod Beyond the Standard Angle Grinder
An automotive mechanic in a Munich service centre was tasked with removing surface rust from the inside of an engine bay sub-frame in early 2026. The standard 100 mm angle grinder could reach the front-facing surfaces but could not reach the inside corners of the sub-frame, where the rust was concentrated. The mechanic tried three workarounds: a longer abrasive disc (which could not reach the corners), a flexible shaft attachment (which lost torque under load), and a different tool entirely (which changed the workflow). None of the workarounds worked. The rust removal job took three times longer than it should have, and the mechanic's hand fatigue from the awkward angles left him unable to work the rest of the day. The job needed a deep-cavity grinding extension rod — a 300 to 400 mm rigid extension that carried an abrasive brush at the working end and mated to the mechanic's standard angle grinder at the drive end. The extension rod did not exist as a catalog item. The mechanic's tool brand commissioned an ODM development program with a 90-day target.
Deep-cavity grinding needs an extension rod beyond the standard angle grinder because the standard tool body is the wrong shape for cavity access. The standard angle grinder is 250 to 300 mm long and is designed for front-facing surface grinding where the operator can see the work and apply downward force. A deep cavity — the inside of an engine bay, the interior of an industrial tank, the inside of an aerospace wing component — is the opposite geometry: the operator cannot see the work, the force direction is sideways or upward, and the cavity walls block direct tool access. The extension rod moves the abrasive end of the tool into the cavity while keeping the drive end (motor, handle, switch) outside the cavity where the operator can control it.
The extension rod is not a stock catalog item for most deep-cavity applications because the cavity geometry, the reach envelope, and the tool interface combination are specific to each application. A catalog supplier would need to stock thousands of extension rod variants to cover all the application combinations, which is not economical. The ODM development path — where the supplier engineers the extension rod to the buyer's specification — is the dominant path for deep-cavity grinding extension rods in 2026.
Step 1: Defining the Extension Length and Reach Envelope
The extension length and reach envelope are the first two parameters the buyer specifies in the ODM program. The extension length is the total length from the drive end (where the extension rod connects to the angle grinder) to the working end (where the abrasive or polishing tool mounts). The reach envelope is the three-dimensional space the working end can access when the extension rod is mounted on the drive tool. For a deep cavity, the reach envelope typically needs to cover 200 to 800 mm of depth plus 50 to 200 mm of lateral offset from the cavity opening.
| Reach range | Total length | Typical application | Construction |
|---|---|---|---|
| Short reach | 100 to 200 mm | Automotive wheel well rust removal, small appliance internal cleaning | Single piece, fixed shank |
| Medium reach | 250 to 400 mm | Engine bay polishing, pipe interior cleaning | Single piece or 2-piece with coupling |
| Long reach | 500 to 1,000 mm | Industrial tank interior cleaning, aerospace component polishing | Multi-piece with 2 to 4 coupling joints |
The extension length and reach envelope definition sets the structural requirements for the rest of the ODM program. A short-reach extension rod can be a single piece of cold-headed carbon steel. A medium-reach extension rod may require a two-piece assembly with a coupling joint in the middle for shipping and storage. A long-reach extension rod typically requires a multi-piece assembly with 2 to 4 coupling joints, and may require flexible sections where the cavity geometry demands non-rigid access. The cost per piece rises with the number of pieces and the complexity of the coupling joints, which is why the buyer should specify the reach envelope as accurately as possible before the ODM engineering design starts.
Step 2: Specifying the Shank, Coupling and Tool Adaptation Interface
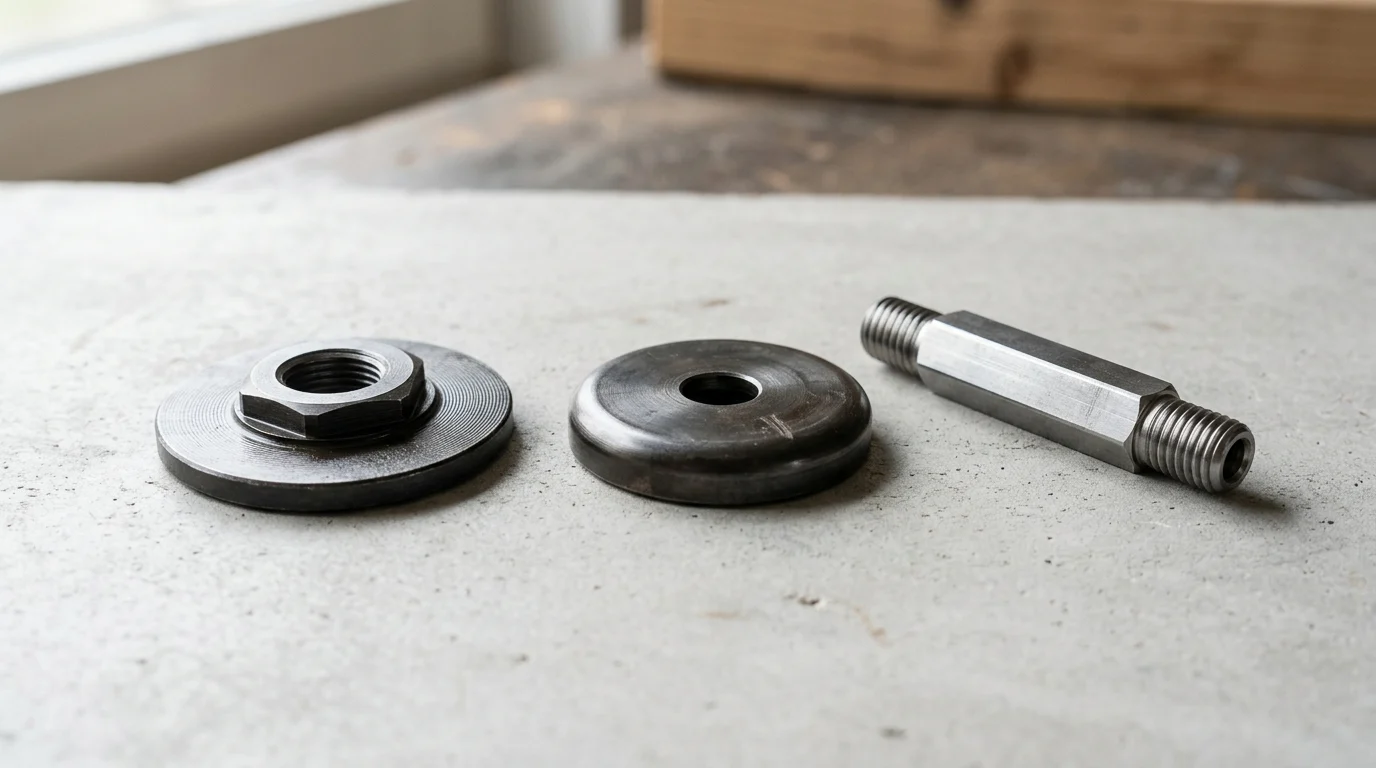
The shank is the drive end of the extension rod that connects to the angle grinder (or the electric drill, or the polisher — the multi-function tool adaptation is in the name). The coupling is the joint in the middle of a multi-piece extension rod that allows the rod to be assembled and disassembled for shipping and storage. The tool adaptation interface is the working end of the extension rod that mounts the abrasive, brush, polishing pad, or other accessory. Each of the three interfaces has its own specification set, and the ODM engineering design must harmonise all three for the extension rod to function correctly.
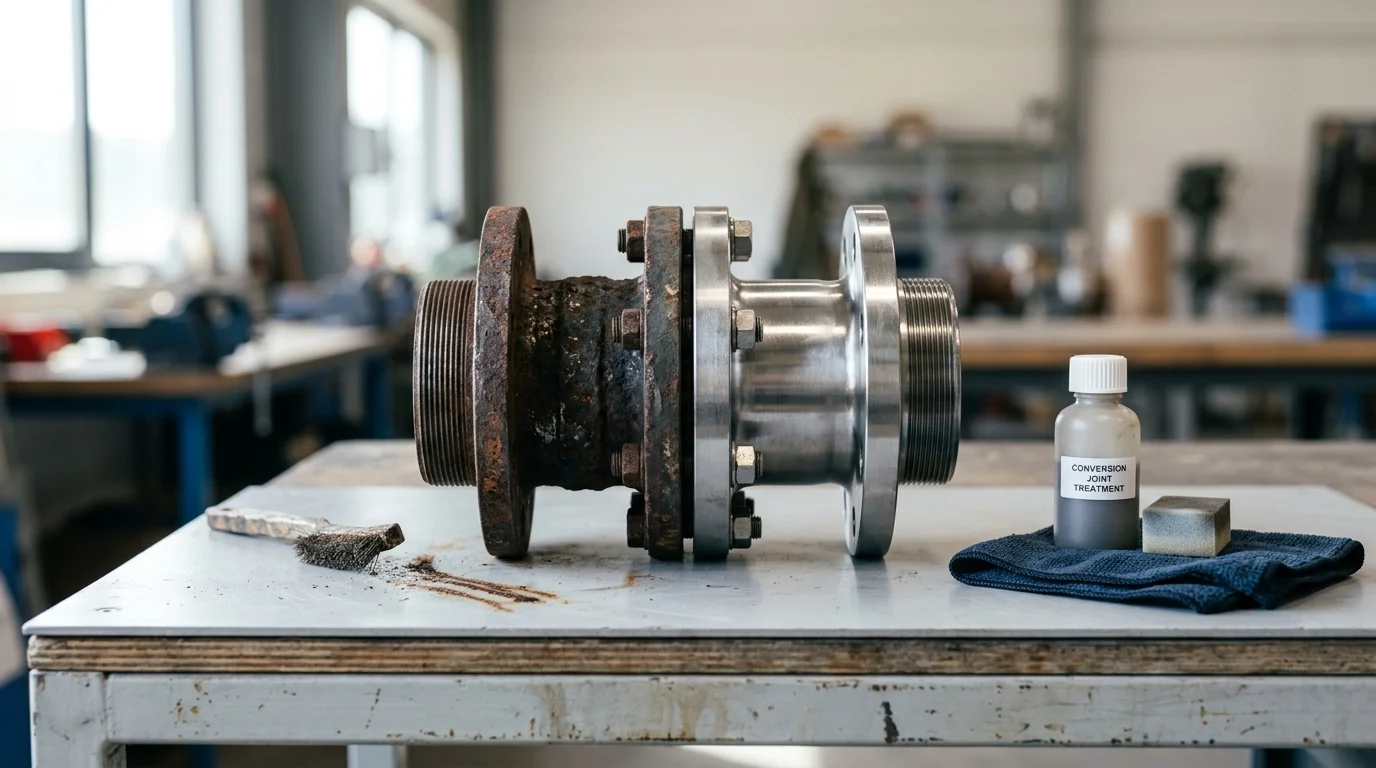
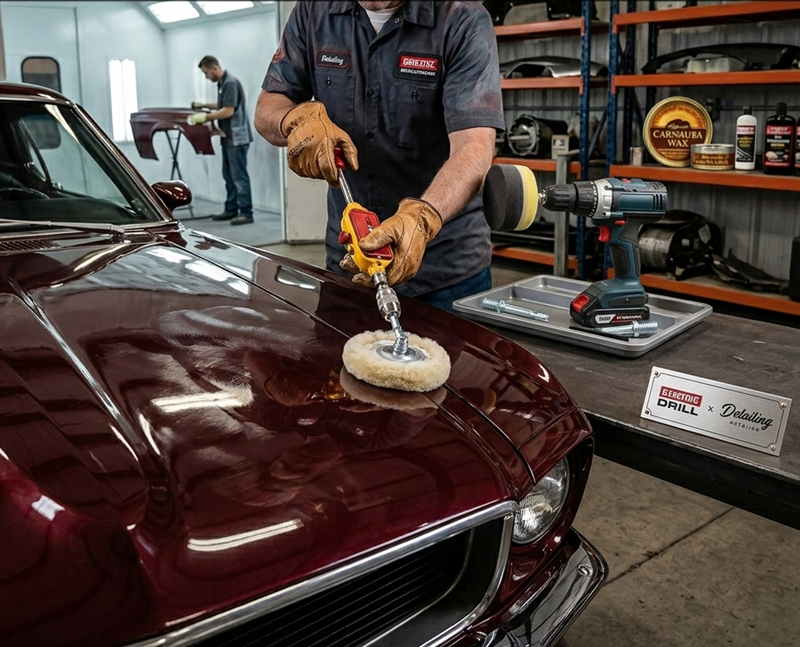
The rust removal and polishing conversion joint product line uses a typical multi-function tool adaptation interface that is directly applicable to deep-cavity grinding extension rods. The conversion joint mounts on the drive end of an angle grinder or electric drill, and the working end accepts a wide range of accessories — brushes, polishing pads, abrasive discs, wool wheels. For deep-cavity grinding, the same conversion joint concept is extended by adding a rigid rod between the conversion joint and the accessory.
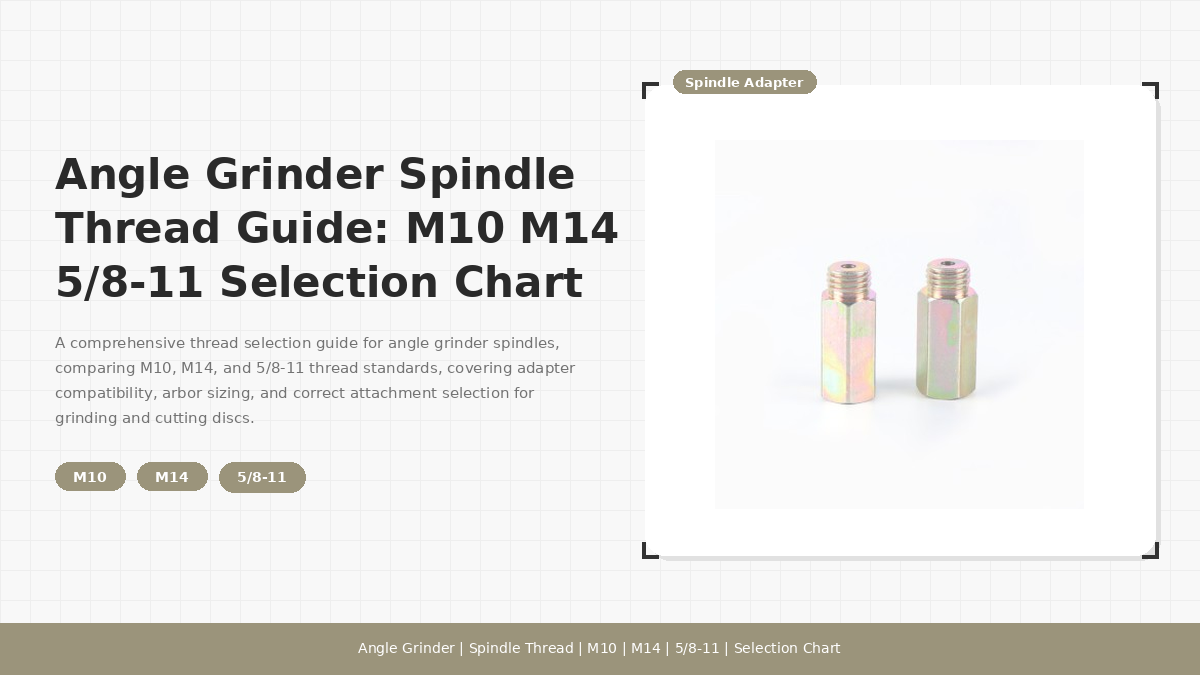
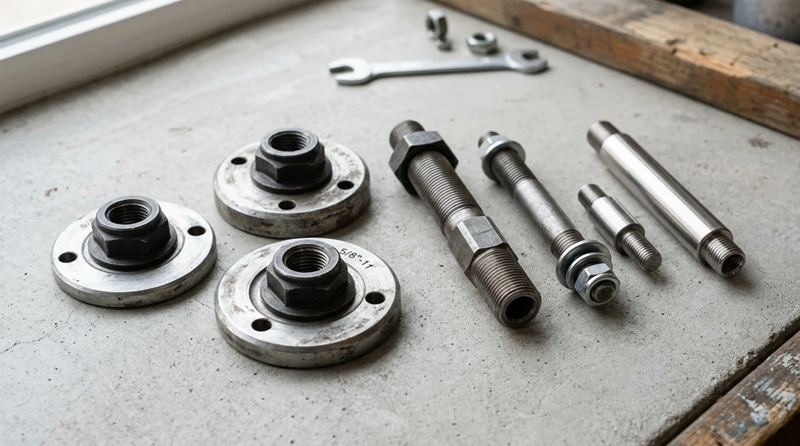
The most commonly specified shank interfaces for deep-cavity grinding extension rods in 2026 are M14 x 2.0 metric thread (the heavy-duty angle grinder standard), M10 x 1.5 metric thread (the light-duty angle grinder standard), 5/8-inch x 11 UNC thread (the North American angle grinder standard), and 1/4-inch hex shank (the electric drill standard). The most commonly specified tool adaptation interfaces at the working end are the same four, plus specialised interfaces for proprietary abrasive systems. A multi-function extension rod typically has an angle grinder thread on the drive end (M10 or M14) and a hex shank or smaller thread on the working end, depending on the accessory.
Step 3: Material Selection for the Extension Rod Body
The extension rod body material is selected by three parameters: the reach length (which determines the weight and the rigidity requirement), the duty cycle (which determines the strength requirement), and the environment (which determines the corrosion resistance requirement). Three materials cover the majority of deep-cavity grinding extension rod applications in 2026.
| Material | Cost (USD/ton) | Reach range | Application |
|---|---|---|---|
| Carbon steel (SWRCH8A) | ~700 | Short reach (100 to 200 mm) | Light-duty, dry environment |
| Stainless steel (304 / 316) | ~2,200 to 3,500 | Medium reach (250 to 400 mm) | Wet or chemical environment |
| Aluminium alloy (6061 / 7075) | ~3,000 to 4,500 | Long reach (500 to 1,000 mm) | User hand fatigue concern |
Carbon steel (SWRCH8A or equivalent) is the lowest-cost option for short-reach extension rods in light-duty applications. The cold-headed carbon steel delivers sufficient strength and rigidity for short-reach use, and the material cost is the lowest of the three options at approximately USD 700 per ton. The angle grinder adapter product line uses cold-headed carbon steel for similar reach ranges.
Stainless steel (304 or 316 grade) is the corrosion-resistant option for medium-reach extension rods in wet or chemical environments. Stainless steel can be machined from bar stock to the required geometry, and the corrosion resistance eliminates the need for a separate surface coating. The material cost is approximately USD 2,200 to USD 3,500 per ton, which is 3 to 5 times the carbon steel cost but is justified by the longer service life in corrosive environments.
Aluminium alloy (6061 or 7075 grade) is the lightweight option for long-reach extension rods where the user's hand fatigue is a concern. Aluminium 6061 is the general-purpose option with good machinability and adequate strength. Aluminium 7075 is the higher-strength option with strength comparable to many steels at one-third the weight. The material cost is approximately USD 3,000 to USD 4,500 per ton. For long-reach extension rods over 600 mm, the weight savings of aluminium over steel is 50 to 65 percent, which directly reduces the operator's hand fatigue over a working day.
Step 4: Prototype Build, Lab Test and Multi-Function Tool Adaptation
The prototype build for a deep-cavity grinding extension rod runs 10 to 20 days, with 10 to 50 prototype pieces produced for the buyer's lab test. The prototype build uses the same production process that the supplier will use for serial production — cold heading for short-reach carbon steel rods, machining for medium-reach stainless steel rods, and machining or extrusion for long-reach aluminium rods. The prototype build confirms that the supplier can produce the geometry within the dimensional tolerance and within the cost target.
The lab test runs 5 to 10 days and covers five verification points. (1) Dimensional verification — every critical dimension is measured on every prototype piece, with the dimensional report compared to the OEM specification. (2) Torque test — the extension rod is mounted on the rated drive tool and subjected to the rated torque, with no failure or permanent deformation. (3) Vibration test — the extension rod is run at the rated RPM for 30 minutes, with vibration measured at the working end and the drive end, with no excessive vibration above the rated threshold. (4) Corrosion test — salt spray test per ASTM B117 for the rated duration (24 hours for indoor use, 48 hours for outdoor use, 96 hours for marine use). (5) Multi-function tool adaptation test — the extension rod is mounted on each of the target drive tools (angle grinder, electric drill, polisher) in turn, and the mounting is verified for fit, torque transmission, and concentricity.
The multi-function tool adaptation test is the specific test that distinguishes a deep-cavity grinding extension rod from a single-purpose extension rod. A single-purpose extension rod is designed to mount on one specific drive tool and accept one specific accessory. A multi-function extension rod is designed to mount on multiple drive tools (typically 2 to 4) and accept multiple accessories (typically 4 to 8), which is what the deep-cavity grinding application requires. The ODM engineering design must accommodate the dimensional and tolerance stack-up of all the tool combinations.
How the ODM Development Cost Amortises Across Adapter Family Extensions
The ODM development cost for a deep-cavity grinding extension rod amortises across the buyer’s product portfolio in three ways. A buyer who runs the program on a single extension rod pays the full upfront cost on that one product. A buyer who extends the program to a family of extension rods (short reach + medium reach + long reach) amortises the upfront cost across the family. A buyer who extends the program to a broader accessory portfolio (extension rods + adapters + pressure plates) amortises the upfront cost across the portfolio. The per-piece development cost falls sharply as the portfolio expands.
Cost amortisation across the extension rod family
The upfront development cost for an ODM extension rod family (3 reach ranges × 3 interface combinations = 9 SKU variants) is USD 12,000 to USD 25,000 for engineering design, prototype build, and tooling setup across the family. This upfront cost is amortised over the buyer’s annual volume across all 9 SKU variants. At an annual volume of 50,000 pieces spread across the family, the per-piece development cost is USD 0.24 to USD 0.50 per piece. At an annual volume of 200,000 pieces, the per-piece development cost falls to USD 0.06 to USD 0.13 per piece, which is a small fraction of the catalog price for similar products.
Cost amortisation across the broader accessory portfolio
The upfront development cost for an ODM extension rod family overlaps significantly with the development cost for other ODM accessories on the same production line. The cold heading tooling, the threading equipment, the surface treatment line, and the QC test rig are all shared across the family. A buyer who adds adapters and pressure plates to the same ODM program amortises the shared tooling and equipment across the broader portfolio, which drops the per-piece development cost by another 30 to 50 percent compared to the extension rod family alone. The break-even point for a multi-portfolio ODM program is typically 12 to 18 months, after which the per-piece cost is below the catalog price for every SKU in the portfolio.
Comparison with separate per-SKU ODM programs
A buyer who runs separate ODM programs for each SKU (one program for the short-reach rod, another program for the medium-reach rod, another for the long-reach rod) pays the full upfront cost for each program. The per-piece development cost is 2 to 3 times higher than the family-level ODM program, and 3 to 5 times higher than the multi-portfolio ODM program. The separate per-SKU approach makes sense only when the buyer’s annual volume per SKU is too low to justify the family-level investment (under 5,000 pieces per SKU per year). For most power tool accessory buyers with a 50,000+ piece annual volume across the family, the family-level or multi-portfolio ODM program is the right call.
Step 5: Certification, Serial Numbering and Container-Ready Shipment
Certification for a deep-cavity grinding extension rod depends on the destination market. For the EU market, CE marking is required and is documented via the supplier's Declaration of Conformity, with the relevant EN standards applied (typically EN 60745 for hand-held motor-operated electric tools, and EN ISO 12100 for general machinery safety). CE marking for an extension rod takes 15 to 30 days, including the technical file preparation and the EU authorised representative appointment where needed.
For the North American market, UL certification is typically required for the extension rod when it is sold as part of a complete power tool system. UL certification for an extension rod takes 30 to 60 days, with the UL engineer reviewing the technical file and the test report from a UL-accredited lab. For the Australian and New Zealand markets, RCM marking is required, which is typically faster than CE or UL and takes 10 to 20 days.
Serial numbering for an ODM extension rod follows three mechanisms. (1) Serial number prefix allocation — the ODM assigns a unique 3 to 4 character prefix to the buyer (for example, KGH for a brand starting with those letters). (2) Sequential numbering range — the ODM maintains a sequential numbering range that increments with each batch. (3) Batch traceability record — each batch's serial number range is recorded in the ODM's batch traceability database, with the production date, the material batch number, and the production line. The serial numbering is laser-etched on every extension rod, which allows the buyer to trace any individual rod back to the production batch in the event of a field issue.
Container-ready shipment for an extension rod ODM program typically uses a 20-foot or 40-foot container with the rods packed in individual paper cartons (10 to 50 rods per carton depending on the size), with the cartons palletised and stretch-wrapped for container shipping. The ODM supplier handles the container loading, the customs documentation, and the freight forwarding. The buyer takes delivery at the destination port.
When Custom ODM Extension Rods Beat Standard Catalog Sourcing
Custom ODM extension rods beat standard catalog sourcing for deep-cavity grinding applications in three scenarios. (1) Application-specific geometry — when the cavity depth, the reach envelope, or the tool interface combination is outside the catalog supplier's stock range, ODM development is the only option. (2) Annual volume above the break-even point — when the buyer's annual volume exceeds 20,000 to 30,000 pieces, the per-piece ODM cost falls below the catalog price because the catalog price includes a distributor markup of 15 to 30 percent. (3) Brand-specific differentiation — when the buyer wants the extension rod to carry the buyer's brand, SKU, and packaging, ODM development is required because catalog suppliers sell under their own brand.
The decision framework is straightforward. The buyer specifies the cavity depth, the reach envelope, the drive tool interface, the working end interface, the annual volume, and the destination market. If the application is within a catalog supplier's stock range and the annual volume is under 20,000 pieces, catalog sourcing is the right call. If the application is outside the catalog range or the annual volume is over 30,000 pieces, ODM development is the right call. The custom precision forged power tool components engineering capability supports both paths, with the ODM path running through the 6-step development cycle described in this article.
For a deep-cavity grinding extension rod ODM program conversation, contact the Yuyao Guling Hardware team with the target cavity depth, the drive tool interface (M10 / M14 / 5/8-inch / hex shank), the working end interface, the annual volume, and the destination market. The team replies within one business day with a feasibility assessment, a development timeline, and a per-piece price indication at three volume tiers (10,000 / 50,000 / 200,000 pieces per year).
Send your target cavity depth, drive tool interface, working end interface, annual volume, and destination market. Yuyao Guling Hardware replies within one business day with a feasibility assessment, a 60 to 120 day development timeline, and a per-piece price indication at three volume tiers.
Frequently Asked Questions
What does ODM development actually mean for a deep-cavity grinding extension rod buyer?
ODM development for a deep-cavity grinding extension rod means that the supplier owns the product design from the specification sketch through to the production-ready part, and the buyer provides the brand, the target market, and the volume commitment. The supplier runs the engineering design, the material selection, the prototype build, the lab test, the certification, and the serial production. The buyer receives the finished extension rod packaged under the buyer's brand, ready for distribution. ODM is different from OEM (which means the buyer owns the design and the supplier manufactures to print) and different from OBM (which means the buyer buys the supplier's stock design and adds the buyer's brand label). For deep-cavity grinding extension rods, ODM is the most common path because the application-specific geometry (length, reach envelope, shank interface) typically requires a custom design that the buyer does not have the in-house engineering capacity to specify in CAD detail.
What extension length and reach envelope are most commonly specified by ODM buyers?
Three extension length and reach envelope ranges are most commonly specified by ODM buyers in 2026. (1) Short reach — 100 to 200 mm total length, used for shallow cavity grinding such as automotive wheel well rust removal and small appliance internal cleaning. The short reach extension rod is typically a single piece with a fixed shank on one end and a threaded interface on the other. (2) Medium reach — 250 to 400 mm total length, used for moderate cavity grinding such as engine bay polishing and pipe interior cleaning. The medium reach extension rod is typically a single piece or a two-piece assembly with a coupling joint in the middle. (3) Long reach — 500 to 1,000 mm total length, used for deep cavity grinding such as industrial tank interior cleaning and aerospace component polishing. The long reach extension rod is typically a multi-piece assembly with 2 to 4 coupling joints and flexible sections where needed.
What tool adaptation interfaces are most commonly specified for multi-function extension rods?
Four tool adaptation interfaces are most commonly specified for multi-function extension rods in 2026. (1) M10 x 1.5 metric thread — the standard interface for light-duty angle grinder accessories, used for brushes, small polishing pads, and light grinding wheels. (2) M14 x 2.0 metric thread — the standard interface for heavy-duty angle grinder accessories, used for cutting discs, heavy grinding wheels, and wire cup brushes. (3) 5/8-inch x 11 UNC thread — the North American standard for angle grinder accessories, equivalent to M16 x 2.0 metric thread for the same heavy-duty application. (4) Hex shank 1/4-inch or 6.35 mm — the standard interface for electric drill accessories, used for drilling, light grinding, and screwdriver bits. A multi-function extension rod typically combines two interfaces: an angle grinder thread (M10 or M14) on the drive end and a hex shank on the accessory end, or vice versa.
How does the ODM handle a brand-specific extension rod serial number range?
The ODM handles a brand-specific extension rod serial number range through three mechanisms. (1) Serial number prefix allocation — the ODM assigns a unique 3 to 4 character prefix to the buyer (for example, KGH for a brand starting with those letters), and the prefix is laser-etched on every extension rod the ODM produces for the buyer. (2) Sequential numbering range — the ODM maintains a sequential numbering range that increments with each batch produced, with the range documented in the buyer's brand SKU master. (3) Batch traceability record — each batch's serial number range is recorded in the ODM's batch traceability database, with the production date, the material batch number, the production line, and the operator signature. The buyer can request the serial number range report at any time and trace any individual extension rod back to the production batch.
How long does an ODM extension rod development cycle typically run from spec to first shipment?
An ODM extension rod development cycle typically runs 60 to 120 days from spec to first shipment, depending on four variables. (1) Design complexity — a standard single-piece extension rod with one interface takes 15 to 25 days for engineering design; a multi-piece assembly with 2 to 4 coupling joints takes 30 to 50 days. (2) Material procurement — carbon steel wire rod is available from stock (5 to 10 days); stainless steel wire rod requires mill order (20 to 35 days); special alloys such as titanium require mill order plus import (40 to 60 days). (3) Prototype build and lab test — 10 to 20 days for 10 to 50 prototype pieces and 5 to 10 days for lab test. (4) Certification — CE marking for the EU market takes 15 to 30 days; UL certification for the North American market takes 30 to 60 days; both in parallel takes 30 to 60 days. The full cycle is typically 60 to 120 days, with most programs landing at 75 to 95 days.
Why are power tool accessory buyers choosing ODM development over catalog sourcing for extension rods?
Power tool accessory buyers are choosing ODM development over catalog sourcing for extension rods in 2026 for four reasons. First, the application specificity — deep-cavity grinding in automotive, aerospace, and industrial applications requires extension lengths and shank interfaces that catalog suppliers do not stock. Second, the brand differentiation — the buyer wants the extension rod to carry the buyer's brand name and SKU, which requires ODM branding at the production stage. Third, the volume economics — once the buyer's annual volume exceeds 50,000 pieces, the ODM unit cost falls below the catalog unit cost (because catalog sourcing includes a distributor markup of 15 to 30 percent). Fourth, the quality control — ODM development allows the buyer to specify the material certificate, the test protocol, and the surface finish, which catalog suppliers cannot guarantee.
Which extension rod body material is most commonly specified by ODM buyers in 2026?
Three extension rod body materials are most commonly specified by ODM buyers in 2026. (1) Carbon steel (SWRCH8A or equivalent) — the lowest-cost option, used for short-reach (100 to 200 mm) extension rods in light-duty applications. The material cost is approximately USD 700 per ton and the rod can be manufactured by cold heading or machining. (2) Stainless steel (304 or 316 grade) — the corrosion-resistant option, used for medium-reach (250 to 400 mm) extension rods in wet or chemical environments. The material cost is approximately USD 2,200 to USD 3,500 per ton and the rod is manufactured by machining from bar stock. (3) Aluminium alloy (6061 or 7075) — the lightweight option, used for long-reach (500 to 1,000 mm) extension rods where the user's hand fatigue is a concern. The material cost is approximately USD 3,000 to USD 4,500 per ton and the rod is manufactured by machining from bar stock or by extrusion.
Is ODM development always more expensive than buying a standard catalog extension rod?
No, ODM development is not always more expensive than buying a standard catalog extension rod, but the total cost structure differs. The upfront development cost for an ODM extension rod program is USD 3,000 to USD 8,000 for engineering design, prototype build, and tooling setup. This upfront cost is amortised over the buyer's annual volume. At an annual volume of 5,000 pieces, the per-piece ODM cost is 20 to 35 percent higher than the catalog price (because the upfront cost is amortised over a small volume). At an annual volume of 50,000 pieces, the per-piece ODM cost falls to within 5 percent of the catalog price. At an annual volume of 200,000 pieces, the per-piece ODM cost is typically 10 to 20 percent lower than the catalog price, because the ODM unit cost drops with volume while the catalog price stays flat. The break-even point is typically 20,000 to 30,000 pieces per year.
About the Author
References and Industry Resources
The following resources were used to support the ODM development analysis in this article. They are industry-association and standards-body references, not the underlying ISO/SAE/ASTM standards themselves. For exact standard text, refer to the regulatory authority directly.
- Society of Automotive Engineers (mechanical and material standards body): SAE International
- British Standards Institution (cold heading and fastener standards portal): BSI Group Standards
- McMaster-Carr (industrial supplier reference catalogue for fasteners and tooling): McMaster-Carr Industrial Supply
- Cold heading steel supplier (carbon and alloy steel wire rod with material certificates): AHP Steel Cold Heading Wire Rod Reference
- ASTM International mechanical testing standards resource (open access summary): SAE International Standards Portal