


Cold Heading vs CNC Turning for Fastener Hardware: Tolerance and Cost Matrix
For a fastener OEM buyer deciding between cold heading and CNC turning, the question is rarely about which process is "better." It is about which process matches your tolerance class, volume tier, and fastener category — and where the crossover points sit. Here is the 6-category × 2-process × 3-volume decision matrix we use in our own RFQ responses, plus the cold-heading mechanical limits that force a switch to CNC turning (or a hybrid of the two), drawn from our 2025 Q1 process comparison and SAE J429 / DIN 933 / GB/T 5783 sourcing standards.
- "Cold heading" forms the part in 1-3 die strokes at 100-300 pieces per minute; "CNC turning" removes material at 5-20 pieces per minute. The cycle-time gap is the primary cost driver at volume.
- Cold heading reaches ISO 2768-m or 2768-c on the formed features; CNC turning reaches 2768-f or precision-grade. The right tolerance on the right feature is the procurement question.
- At 10K units and above, cold heading wins on unit cost for any geometry it can form; at 1K units and below, CNC turning wins because the cold-heading die has to be amortized.
- Material yield is the second-largest cost driver: cold heading at 95%+ vs CNC turning at 30-60% on hex bolts — that yield gap translates directly to material cost per piece.
- For most fastener categories, the right answer is a hybrid: cold heading forms the rough shape, thread rolling finishes the thread, and CNC finish-turning reaches the tight-tolerance features that heading alone cannot hit.
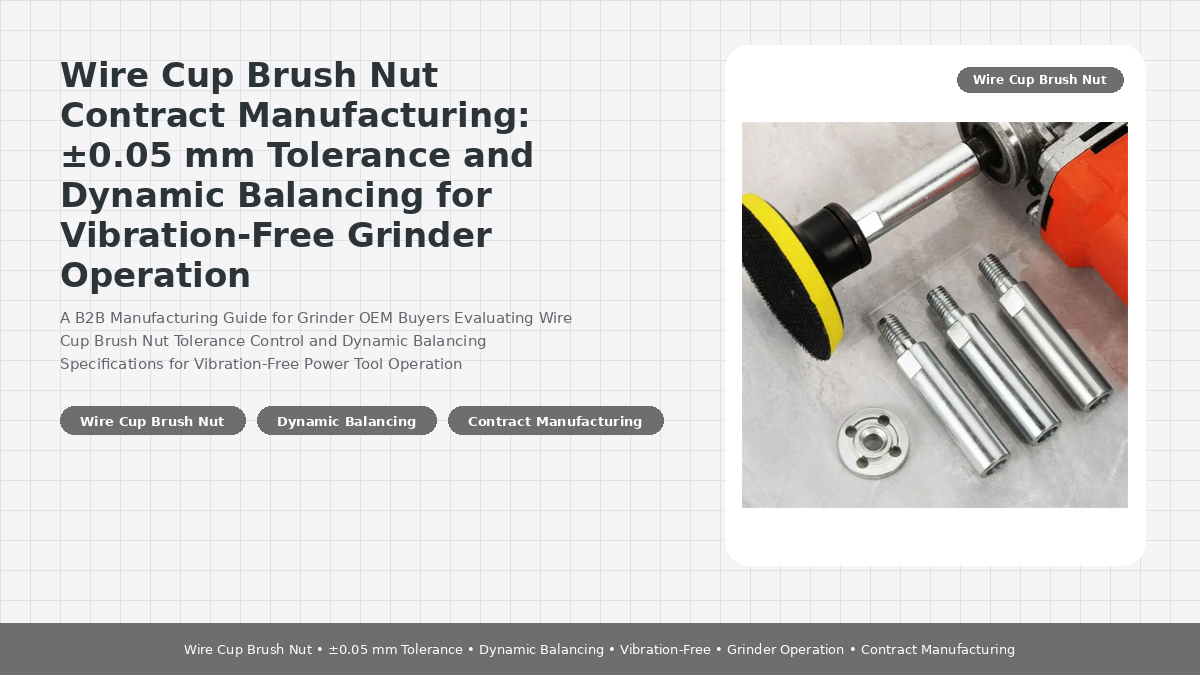
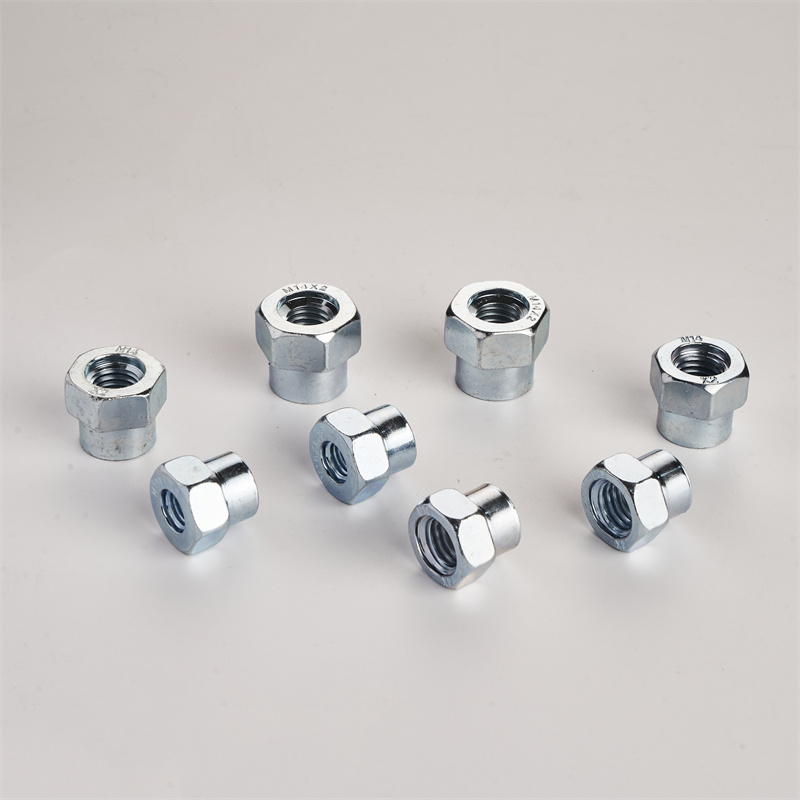 Gulin hexagonal locking nut for angle grinder spindle — the cold-heading + thread-rolling fastener referenced in this article's tolerance and cost matrix.
What "Cold Heading" and "CNC Turning" Actually Mean for a Fastener (And Why the Tolerance Class Drives the Decision)
A fastener's hexagonal locking nuts product page might list a single "material" and a single "tolerance" without ever telling you which process made it. The process matters because it sets the ceiling on what the tolerance can be, the floor on what the unit cost will be, and the practical MOQ for the SKU. Cold heading is a high-speed cold plastic-forming process: a coil of steel wire feeds into a multi-station die, and a punch forms the part in 1-3 die strokes at 100-300 pieces per minute. CNC turning is a subtractive process: a bar of steel feeds into a lathe, and a cutting tool removes material to form the part at 5-20 pieces per minute.
Both processes can produce a hex-head bolt to a usable specification; both processes are widely used in commercial fastener production. The trade-off is not about whether one process can do the job — it is about which process is the better economic answer for the SKU's volume tier and tolerance class. The tolerance class drives the decision more than any other single factor, because ISO 2768 (the general tolerance standard for machined and formed parts) sets four classes — fine (f), medium (m), coarse (c), and very coarse (v) — and the achievable tolerance class on the formed features differs by process.
6 Fastener Categories × 2 Processes: Which Format Fits Each One
Six common fastener categories a B2B buyer will spec, with the process that fits each one best:
| Fastener category | Cold heading fit | CNC turning fit | Default process |
|---|---|---|---|
| Hex head bolt (DIN 933 / GB/T 5783 / ASME B18.2.1) | Strong | Slow at volume | Cold heading + thread rolling |
| Socket head cap screw (DIN 912 / ISO 4762) | Strong | Slow at volume | Cold heading + hex-socket milling |
| Hex nut (DIN 934 / ISO 4032) | Strong | Not economical | Cold heading + tapping |
| Flat washer (DIN 125 / ISO 7089) | Strong | Not economical | Cold heading (stamping die) |
| Dowel pin (ISO 2338 / DIN 6325) | Limited to L/D ≤5 | Strong | CNC turning (straightness-critical) |
| Custom flange adapter (drawing-based) | Conditional | Strong | CNC turning + secondary drilling |
The pattern: cold heading wins on the formed-in-one-stroke fastener categories (hex bolt, hex nut, flat washer) where the head and body share a rotational symmetry. CNC turning wins on the long-aspect-ratio (dowel pin) and asymmetric (custom flange adapter) categories where cold heading die complexity or material-flow control becomes the bottleneck. The custom flange adapter row is the one a fastener buyer most often gets wrong, because the drawing looks like a hex-bolt family member at first glance.
ISO 2768 Tolerance Class Compatibility: m-K, c-K, f-K, Precision
The four tolerance classes of ISO 2768 — fine (f), medium (m), coarse (c), and very coarse (v) — define acceptable dimensional deviation on linear dimensions. The achievable tolerance class differs sharply by process on the formed features of a fastener:
| ISO 2768 tolerance class | Typical linear deviation (mm, M8 part) | Cold heading on head geometry | CNC turning on all features |
|---|---|---|---|
| Fine (f) | ±0.1 mm | Limited (with coining) | Achievable |
| Medium (m) | ±0.2 mm | Standard | Achievable |
| Coarse (c) | ±0.5 mm | Standard | Achievable |
| Very coarse (v) | ±1.0 mm | Standard | Achievable |
The right way to read the table is by feature, not by the part. For the head geometry of a hex bolt — across-flats, head height, corner radius — cold heading with a coining pass reaches ISO 2768-f. For the threaded shank, cold heading forms the unthreaded blank, and the thread is rolled afterward to a 6g/6h fit per ISO 898-1, which is finer than ISO 2768-f for threaded engagement. For long-aspect-ratio features (dowel pin, custom adapter), cold heading cannot hold straightness and roundness; CNC turning is the right process. The spec to write on the drawing is the tightest tolerance on each feature separately, not a single ISO 2768 class for the whole part.
Unit Cost at 10K / 100K / 1M Runs: A 6×2×3 Cost Matrix for Procurement
For a fastener buyer doing a multi-year budget, the relevant comparison is unit cost at the actual volume tier of the SKU. We do not publish list pricing on the website because it varies by region, finish, and order volume, so the framework below is a unit-cost relative index with cold heading on a standard hex-head bolt M8 at 100K runs set to 100 as the reference.
| Volume tier | Cold heading cost index (M8 hex bolt) | CNC turning cost index (M8 hex bolt) | Process winner |
|---|---|---|---|
| 10K unit run | 140 (die amortization) | 180 (full cycle) | Cold heading |
| 100K unit run | 100 (reference) | 175 (slight cycle gain) | Cold heading |
| 1M unit run | 75 (volume discount) | 170 (no learning curve) | Cold heading |
The crossover for a hex-bolt M8 is well above 1M units — cold heading wins on cost at any volume tier where the die can be amortized. The breakeven for cold heading is around 5K-10K units per part number (depending on die complexity); below that, CNC turning wins. The unit-cost gap widens with material yield: cold heading at 95%+ material utilization vs CNC turning at 30-60% on a hex bolt, which translates directly to material cost per piece. For buyers buying on landed cost, the freight cost is similar between the two processes; the gap is at the per-piece manufacturing cost.
Cold Heading Mechanical Limits: When Work-Hardening Forces a Switch to Turning
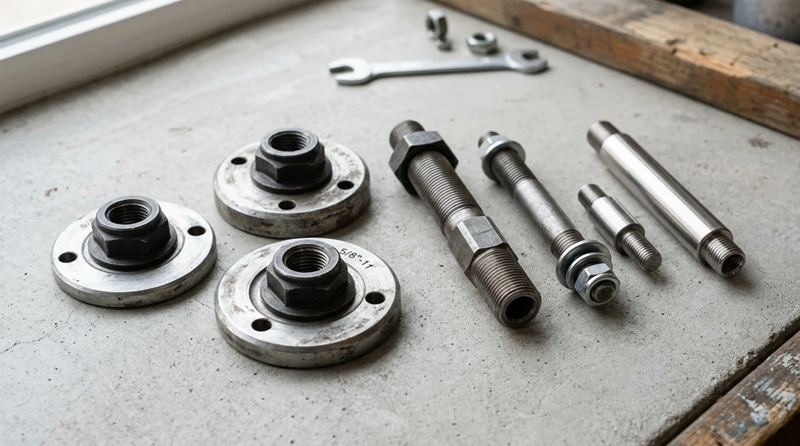
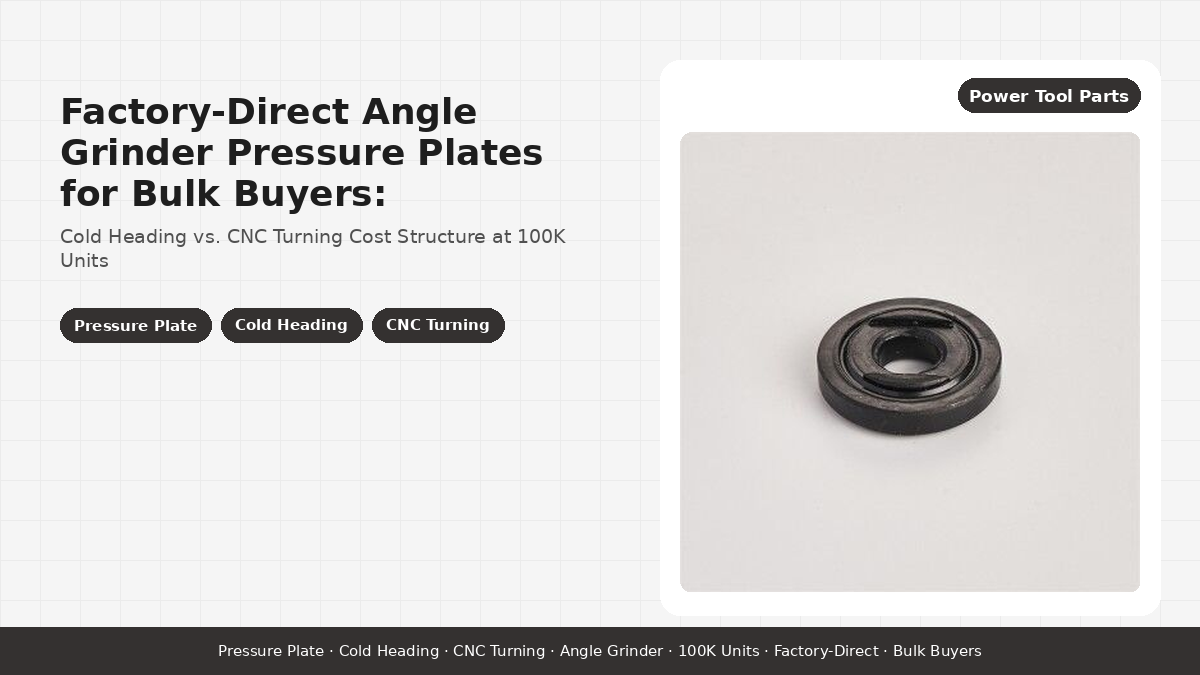
Cold heading has real mechanical limits that a fastener buyer should understand before specifying a process. The first limit is material work-hardening. Austenitic stainless (304, 316) work-hardens under cold deformation; the die force for a 304 stainless M8 hex bolt is roughly 1.5-2.0x the force for the same part in 1018 carbon steel. Most cold heading lines are rated for stainless up to M16 at moderate geometry; beyond that, the press tonnage requirement crosses into specialized cold-heading equipment. The second limit is geometry: deep internal threads that go past the part midpoint, thin-walled long shafts with L/D ratio above 8, and very small fasteners below M3 where die strength limits cold heading. The third limit is part size: very large fasteners above M24 where press capacity is the bottleneck. For fasteners above M24 in 304/316, CNC turning or warm heading is often the right answer. angle grinder pressure plate category draws on both processes — the body is cold-headed for grain-flow strength, and the spindle bore is finish-turned for fit with M10/M14/5/8-11 spindle standards.
The Buyer Decision Matrix: Tolerance × Volume × Category
Pulling the framework together, here is the decision matrix a fastener OEM sourcing team should walk through at RFQ stage:
| Buyer signal | Default process | Why |
|---|---|---|
| Volume tier below 5K units per SKU | CNC turning | Cold heading die cannot be amortized below this tier |
| Volume tier 5K-10K units per SKU | Cold heading (single-die) | Die amortization works at this tier |
| Volume tier above 100K units per SKU | Cold heading (multi-die) | Multi-die cold heading maximizes cycle-time and yield |
| Tolerance class ISO 2768-f on a long-aspect-ratio feature | CNC turning | Cold heading cannot hold straightness and roundness |
| Standard bolt / nut / washer geometry | Cold heading + thread rolling | Best unit economics at any volume above 5K |
| Custom flange adapter or asymmetric geometry | CNC turning | Cold heading die cost is prohibitive on asymmetric parts |
| Stainless 304/316 above M16 | CNC turning or warm heading | Cold heading work-hardening limit on austenitic stainless |
| Thread tolerance tighter than 6g/6h | CNC thread milling | Thread rolling cannot reach 4g/4h aerospace-grade tolerance |
For most standard fastener categories — hex bolt, hex nut, flat washer — the answer is cold heading. For long-aspect-ratio features (dowel pin, custom adapter) and short-run / prototype work, the answer is CNC turning. For volume production of structural fasteners to SAE J429 mechanical-property specs, the answer is often a hybrid: cold heading forms the rough shape, thread rolling finishes the thread, and CNC finish-turning reaches the tight-tolerance features that heading alone cannot hit.
6 Sourcing Mistakes When Specifying Fastener Process (And How to Avoid Them)
- Specifying a single ISO 2768 class for the whole part. Specify tolerance class per feature (head vs shank vs thread); mixing f-class head with 6g thread on a hex bolt is standard and saves cost.
- Quoting cold heading for a custom geometry that the die maker says needs a 3-station progressive die. Multi-station progressive dies multiply die cost by 2-4x; CNC turning may be cheaper even at volume.
- Forgetting about thread-rolling die cost in the cold-heading quote. Thread rolling is a separate operation with its own die; the cold-heading quote is incomplete without it.
- Specifying stainless 304 cold heading above M16 without confirming press tonnage. Work-hardening on 304 above M16 often crosses press-tonnage limits; switch to CNC turning or warm heading.
- Treating "M8 hex bolt" as one SKU across vendors. Across-vendor tolerance class, head marking, and finish vary; specify per drawing and per spec, not per nominal size.
- Ignoring the surface-treatment interaction with cold heading. Cold-headed parts have a work-hardened surface layer; some surface treatments (electroplating) bond differently than on a turned surface; specify and test.
FAQ: Cold Heading vs CNC Turning Questions Fastener Buyers Ask
Can cold heading reach ISO 2768-f (fine) tolerance on a hex bolt?
On standard hex-head external dimensions (across-flats, head height, corner radii), yes — cold heading with a finishing coining pass typically reaches ISO 2768-f on the head geometry. On the threaded shank, no — cold heading forms the unthreaded blank, and the thread is rolled afterward. Rolled threads typically reach 6g/6h tolerance per ISO 898-1, which is finer than ISO 2768-f for threaded engagement. The trick is to specify the right tolerance on the right feature: ISO 2768 for the head, ISO 898 for the thread.
Why is cold heading cheaper than CNC turning at high volume?
Cold heading forms a fastener from a single coil of wire in 1-3 die strokes at 100-300 parts per minute; material utilization is typically 95%+. CNC turning removes material to form a fastener at 5-20 parts per minute from bar stock; material utilization drops to 30-60% on turned fasteners depending on geometry. The cycle-time and material-yield gap is the primary cost driver. At 10K units and above, cold heading wins on unit cost for any geometry it can form. At 1K units and below, CNC turning wins because cold heading requires a custom die set that has to be amortized over the run.
When does CNC turning beat cold heading on a fastener project?
CNC turning beats cold heading when the geometry has features cold heading cannot produce: deep internal threads that go past the part midpoint, thin-walled long shafts (L/D ratio above 8), very small fasteners below M3 where die strength limits cold heading, very large fasteners above M24 where press capacity is the bottleneck, work-hardening materials like 301/304 stainless at heavy reductions, and short-run parts below the cold-heading die amortization threshold (typically under 1K units per part number). CNC turning is also the right answer for prototypes and small-batch samples.
Does cold heading work on stainless steel fasteners?
Yes, but with caveats. Austenitic stainless (304, 316) work-hardens under cold heading; the die force for a 304 stainless M8 hex bolt is roughly 1.5-2.0x the force for the same part in 1018 carbon steel. Most cold heading lines are rated for stainless up to M16 at moderate geometry; beyond that, the press tonnage requirement crosses into specialized cold-heading equipment. For martensitic stainless (410, 420) the forming is easier but post-form heat treatment is required for strength. For fasteners above M16 in 304/316, CNC turning or warm heading is often the right answer.
What tolerance does cold heading actually achieve on the thread?
Cold heading forms the unthreaded blank; threads are produced by a separate thread-rolling operation after heading. Rolled threads on a cold-headed fastener typically achieve 6g/6h tolerance per ISO 898-1 (medium fit), which covers roughly 80% of commercial fastener applications. For tighter thread tolerance (4g/4h, aerospace-grade), or for left-hand threads, Acme threads, or multi-start threads, CNC thread-milling or single-point turning is required. The combination of cold heading + thread rolling covers the bulk of the bolt/screw market; CNC thread-milling is the exception rather than the rule.
How does cold heading compare with CNC turning on material yield?
Cold heading yields 95%+ because it forms the part from wire without removing material — the slug is shaped, not cut. CNC turning yields 30-60% on typical hex bolts and 20-40% on long-shaft fasteners, because most of the bar stock is turned into chips. The yield gap is one of the largest contributors to the unit-cost gap at volume. For buyers buying on cost-per-shipped-piece, the yield gap translates directly to material cost per piece. For buyers buying on landed cost-per-piece, freight cost is similar because both processes produce parts of similar mass.
Is there a hybrid cold heading + finish-turning process?
Yes, and it is the right answer for several real-world fastener specs. Cold heading forms the rough shape (head + most of the shank), and a finish-turning operation refines the features that cold heading cannot reach — secondary diameters, special under-head fillets, and tight-tolerance features. The hybrid process is common in structural bolts to ASTM A325/A490 specs, where the head is cold-headed for grain-flow strength and the shank is finish-turned to meet the body-diameter tolerance. The hybrid is also used for flanged hex bolts where the flange geometry needs a tighter tolerance than cold heading alone delivers.
What is the typical MOQ difference between cold heading and CNC turning?
Cold heading requires a custom die set per part number. Die cost for a standard hex-bolt die set runs in the low-to-mid four-figure USD range; that cost has to be amortized over the run. The breakeven point is typically 5K-10K units per part number, depending on die complexity and steel grade. CNC turning requires only a part program, not a die, so MOQs are effectively 1 — but the per-piece cost is higher to cover programming, setup, and slower cycle times. For short-run / prototype work, CNC turning is the default; for medium-to-high volume production, cold heading wins.
Sourcing a fastener program at the right tolerance × volume × category combination? Our RFQ team responds to spec requests in under 24 hours with a process recommendation, a sample box shipped within 5 business days, and a quote ladder across the 10K / 100K / 1M volume tiers. Gulin manufacturing
Sources & further reading — SAE J429 mechanical properties for externally threaded fasteners · DIN Deutsches Institut für Normung · ASM International · ASME · McMaster-Carr fastener reference · US ITA · USITC · EN standards