


In angle grinder manufacturing, material choice is not just a cost decision—it directly affects safety, torque transmission, wear life, and compatibility at speeds that can exceed 10,000 RPM. Carbon steel remains a practical standard for critical hardware such as locking nuts, flanges, fasteners, and gears because it combines strength, machinability, and scalable production through forging, stamping, and heat treatment. This article examines why grades such as 1045 and Q235 are widely used, where carbon steel outperforms alternatives, and when corrosion protection or alloy upgrades become necessary. For buyers and engineers sourcing carbon steel hardware parts, understanding these trade-offs helps ensure reliable performance in demanding power tool applications.
Why Carbon Steel Hardware Parts Are Preferred
The manufacturing of heavy-duty power tools demands materials that can withstand intense mechanical stress, high rotational speeds, and constant vibration. For decades, carbon steel hardware components have served as the common default for critical power tool mechanisms. It is important to clarify that in this context, "accessories" refers to internal hardware, fasteners, and gears, rather than consumable items like abrasive discs. The balance of high tensile strength, excellent machinability, and cost-effectiveness makes carbon steel a highly practical option for high-stress parts in angle grinders, circular saws, and cutting machines. However, carbon steel carries a noticeable weight penalty compared to alternatives like aluminum or polymers, which are typically preferred for tool housings and safety guards.
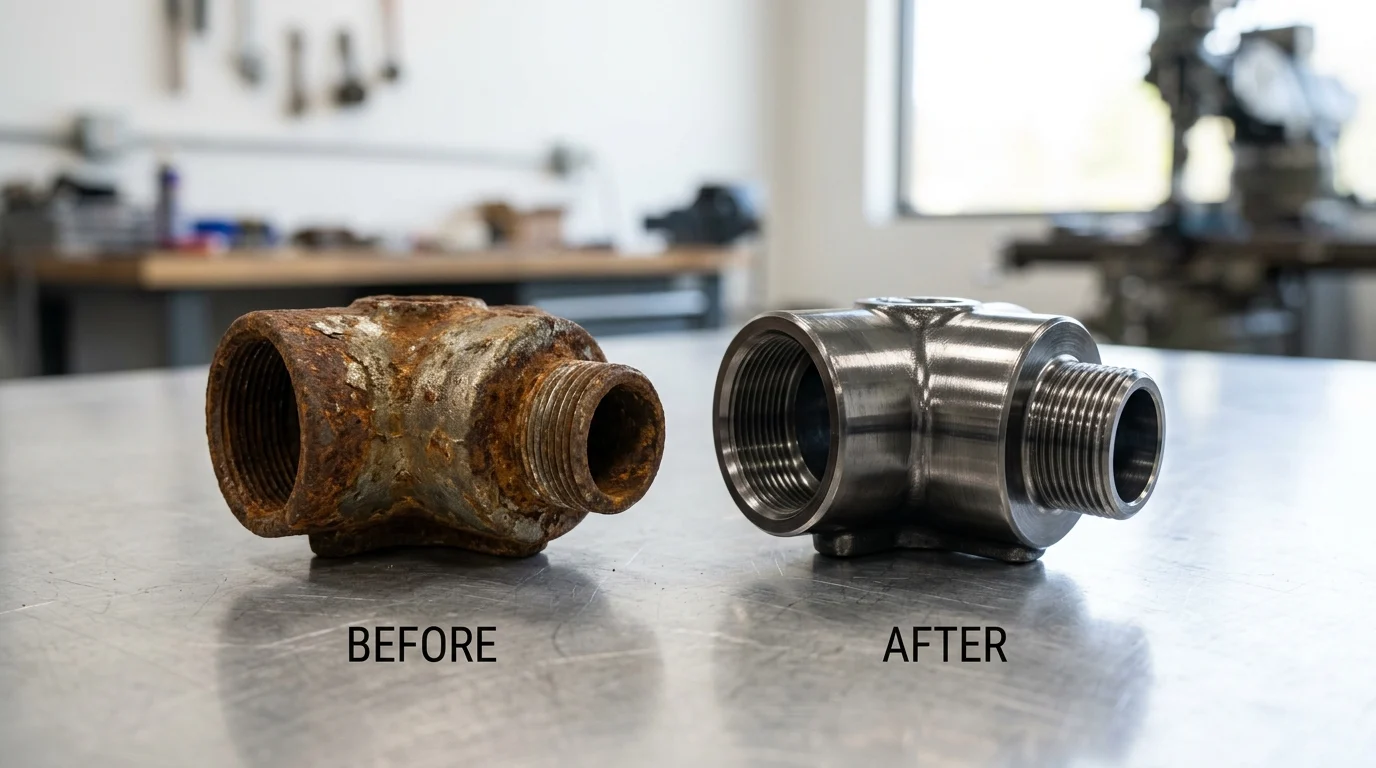
Because angle grinders are subjected to severe torque and abrasive forces, internal mechanisms and external fasteners must guarantee operational safety and long-term durability. Forging and stamping allow manufacturers to produce highly reliable components that meet specific international standards, such as ISO, DIN, GB, or ANSI specifications. Engineers must also mitigate carbon steel's inherent susceptibility to rust by applying appropriate surface treatments, or opt for stainless steel and specialized alloy steels when operating in highly corrosive environments.
Common Carbon Steel Parts in Angle Grinders
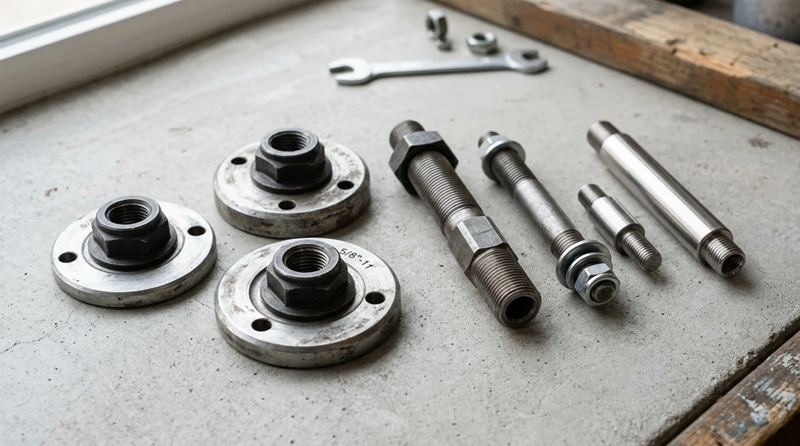
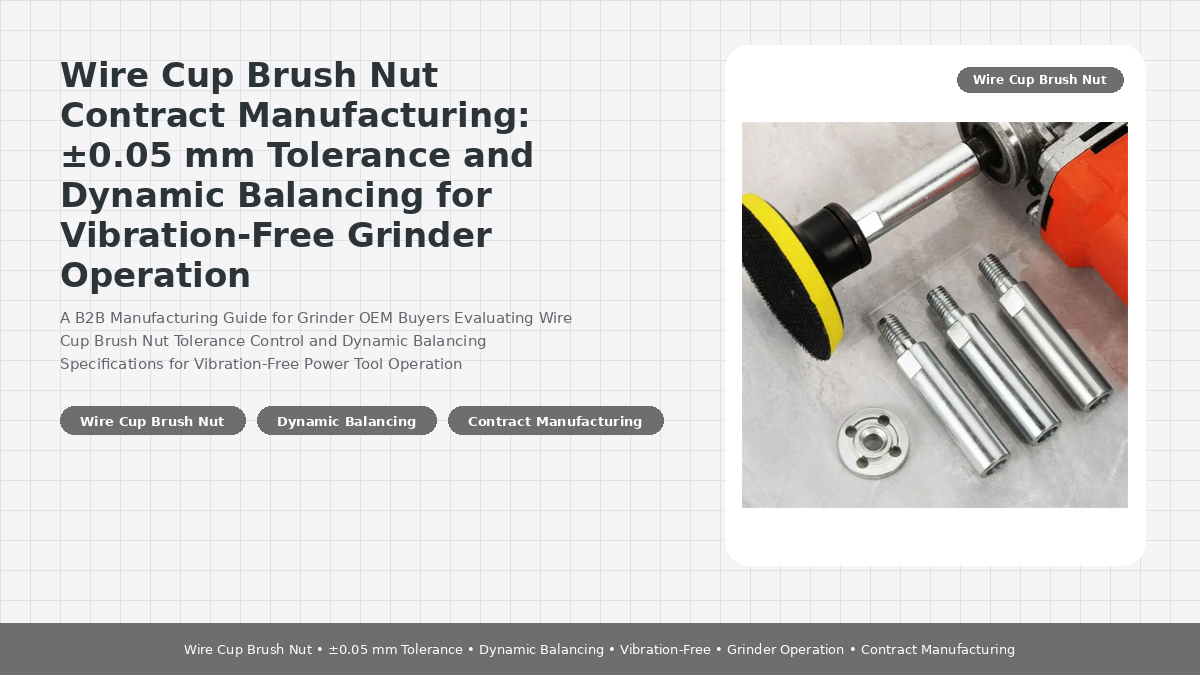
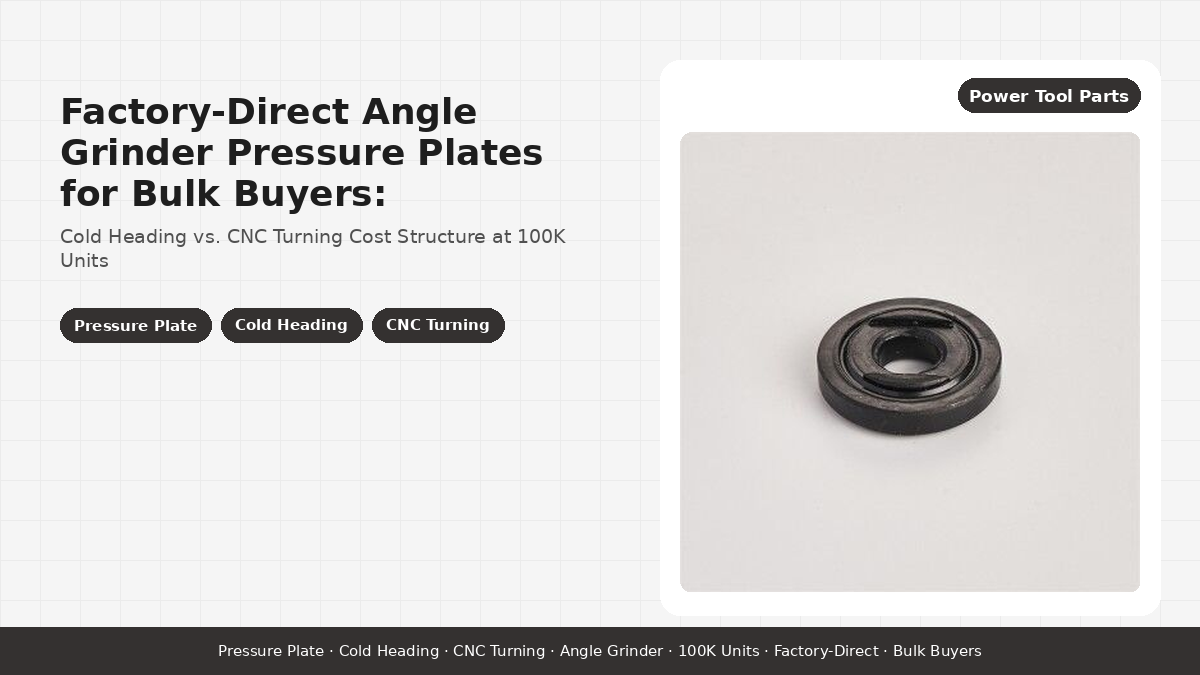
Common carbon steel components in angle grinders primarily include pressure plates (flanges), locking nuts, and spindle gears. These parts secure abrasive discs that routinely operate at extreme speeds, often ranging from 10,000 to 12,000 RPM. A failure at these velocities can result in catastrophic tool damage or severe operator injury, making material integrity a critical safety factor.
Manufacturers typically produce these standardized locking nuts and flanges to strict industry specifications (such as EN 60745 safety standards for hand-held power tools), tailored for 100 mm (4-inch) up to 230 mm grinder models. Standardizing these dimensions ensures universal compatibility across different tool brands while maintaining the structural rigidity required to lock large-diameter cutting wheels firmly in place during heavy industrial use.
Key Properties of 45 Steel and A3 Steel
The power tool industry relies heavily on specific material grades, notably AISI 1045 (roughly corresponding to Chinese 45# steel) and Q235 (formerly designated as A3 steel in China). 1045 steel is a high-quality medium-carbon grade known for reliable mechanical properties. Depending on heat-treatment and part geometry, normalized 1045 achieves a tensile strength ranging from 570 to 700 MPa, making it highly resistant to deformation. When subjected to precise quenching and tempering, its surface hardness typically reaches HRC 40 to 50, providing necessary wear resistance for frequently adjusted locking mechanisms.
In contrast, Q235 is a low-carbon or mild steel offering superior formability. While it does not achieve the same maximum hardness as medium-carbon grades, its high ductility makes it ideal for components requiring complex stamping or cold heading without cracking. Specialized applications may utilize alloy steels when extreme surface hardness is the primary engineering requirement.
How Carbon Steel Parts Compare With Powder Metallurgy Parts
While traditional steel forming dominates the market for high-stress fasteners, powder metallurgy (PM) has emerged as a highly capable alternative manufacturing process for producing complex, net-shape components. It is critical to distinguish that carbon steel is a material category, whereas PM is a manufacturing method that utilizes various metal powders, including steel alloys. The comparison centers on process trade-offs—specifically forged or machined steel versus sintered PM steel. PM involves pressing metal powder into a die and sintering it at high temperatures. When evaluating structural integrity for high-speed grinding equipment, components shaped via traditional forging and machining often serve as the baseline for mechanical reliability. However, PM properties vary widely based on the specific material, density, and secondary processing; advanced PM steel parts can be further densified or heat-treated to match or closely approach the performance of forged steel.
Key Specification Factors to Compare
To understand the trade-offs between these manufacturing techniques, engineers must evaluate density, tensile strength, and production economics. Standard powder metallurgy parts often retain microscopic porosity, typically achieving 85% to 92% of theoretical density. This porosity can act as a stress concentrator, which may compromise impact resistance in standard grades. In contrast, forged carbon steel hardware achieves near-theoretical density (virtually 100%), eliminating internal voids and maximizing fatigue life.
| Specification Metric | Forged Carbon Steel (e.g., 1045) | Standard Powder Metallurgy (PM) |
|---|---|---|
| Material Density | ~100% (Fully Dense) | 85% - 92% (Porous) |
| Tensile Strength | High (570-700 MPa) | Moderate (~400-500 MPa) |
| Impact Resistance | Excellent | Fair to Poor |
| Tooling Cost | Varies significantly by complexity | High upfront, competitive at volume |
| Best Application | High-stress pressure plates | Complex, low-impact gears |
For angle grinder pressure plates that endure sudden shocks and clamping forces, the fully dense structure of forged steel remains highly effective. PM is frequently utilized for intricately shaped internal gears where machining costs would be prohibitive and the material's specific properties can be optimized for the required load.
Effects of Forging, Stamping, Machining, and Heat Treatment
The reliability of traditional steel parts stems from a rigorous production route: forging or stamping, followed by machining, heat treatment, surface treatment, and testing. Facilities equipped with modern multi-station cold heading machines utilize precision forging to align the internal grain structure of the metal with the component's geometry. These machines apply immense pressure to shape the steel at room temperature, significantly increasing its yield strength through work hardening.
Following initial forming, secondary machining achieves exact dimensional accuracy. Fully automatic CNC machining centers allow factories to maintain strict tolerances. For safety-critical classes, these tolerances can be as tight as ±0.01 mm on threading and mating surfaces, though this is an illustrative target rather than a universal requirement for every grinder part. Finally, heat treatment optimizes the hardness-to-toughness ratio. Because carbon steel is highly susceptible to rust, surface treatments like black oxide or zinc plating are mandatory to provide corrosion resistance in harsh, dust-filled construction environments.
How Buyers Can Choose Reliable Suppliers
Selecting a dependable partner for Carbon Steel Hardware Parts requires moving beyond basic internet searches to conduct rigorous technical evaluations. Buyers must assess both the physical infrastructure and the operational standards of potential manufacturing partners to ensure long-term supply chain stability.
Practical Steps to Verify Manufacturing Capability
To ensure a supplier can meet strict industrial demands, buyers should evaluate their production infrastructure through a systematic review:
- Assess Machinery Investment: Reliable manufacturers utilize modern, well-maintained equipment. Look for facilities utilizing advanced cold heading forming models (such as 19B, 24B, or 28B) and high-quality machine forging. A factory operating dozens of fully automatic CNC machine tools and automatic tapping machines demonstrates the capacity for high-volume precision.
- Evaluate the Complete Process Route: Verify that the supplier controls the entire manufacturing cycle. A robust workflow for power tool accessories must include forging or stamping, precision machining, heat treatment, surface treatment, and comprehensive final testing.
- Analyze Material Competency: Confirm the supplier has proven experience working with the necessary material grades. A capable factory should seamlessly handle A3 steel, 45# steel, and high carbon steel, while also offering advanced forming techniques like powder metallurgy.
Decision Criteria for Price, Quality, and Consistency
When comparing quotes for angle grinder accessories, procurement teams must balance upfront costs with long-term reliability.
- Quality Over Lowest Price: Unusually cheap components often bypass essential heat treatments, leading to premature failure and safety risks. Evaluate the supplier's in-house testing instruments and quality control protocols to ensure structural integrity is never compromised.
- Production Consistency: High automation directly correlates with product uniformity. Suppliers heavily invested in automated CNC operations provide stable support for industrial customers who demand strict dimensional consistency across large, recurring batches.
- Specification Readiness: A mature supplier should already have the tooling and expertise for standard industry sizes. For angle grinder pressure plates, this includes immediate manufacturing capability for 100-type, 125-type, 150-type, 180-type, and 230-type specifications.
By applying these technical benchmarks, buyers can secure a supply chain that delivers durable, high-performance power tool accessories while mitigating the risks of production delays or quality defects.
Key Takeaways
- Use carbon steel for high-stress grinder hardware such as locking nuts, flanges, fasteners, and spindle gears where strength and cost efficiency are both critical.
- Select 1045 steel for components needing higher tensile strength, with normalized strength commonly reaching about 570 to 700 MPa.
- Specify heat-treated 1045 steel when wear resistance is required, as quenching and tempering can achieve surface hardness around HRC 40 to 50.
- Choose Q235 steel for stamped or cold-headed parts where ductility, formability, and crack resistance matter more than maximum hardness.
- Apply suitable surface treatments to carbon steel parts to reduce corrosion risk, especially for tools used in humid or abrasive environments.
- Verify that grinder flanges and locking nuts meet relevant standards and fit models from 100 mm to 230 mm to support safe high-speed operation.
Frequently Asked Questions
Which carbon steel parts are commonly used in angle grinders?
Common parts include pressure plates or flanges, locking nuts, spindle gears, and external fasteners. These components help secure discs, transmit torque, and maintain stability during high-speed operation.
Why is carbon steel preferred for grinder hardware components?
Carbon steel offers a strong balance of tensile strength, machinability, wear resistance, and cost efficiency. This makes it practical for high-stress hardware used in power tools such as angle grinders and cutting machines.
What is the difference between 1045 steel and Q235 steel?
1045 steel is a medium-carbon grade valued for strength and heat-treatment response, while Q235 is a mild steel known for ductility and formability. 1045 suits wear-resistant parts; Q235 suits stamped or formed components.
How fast do angle grinder accessories typically operate?
Many grinder discs operate at around 10,000 to 12,000 RPM, depending on tool size and design. At these speeds, locking nuts, flanges, and gears must maintain precise strength and dimensional reliability.
Does carbon steel need surface treatment?
Yes. Carbon steel can rust in humid or corrosive environments, so zinc plating, black oxide, phosphating, or other protective finishes are often used to improve corrosion resistance and service life.