


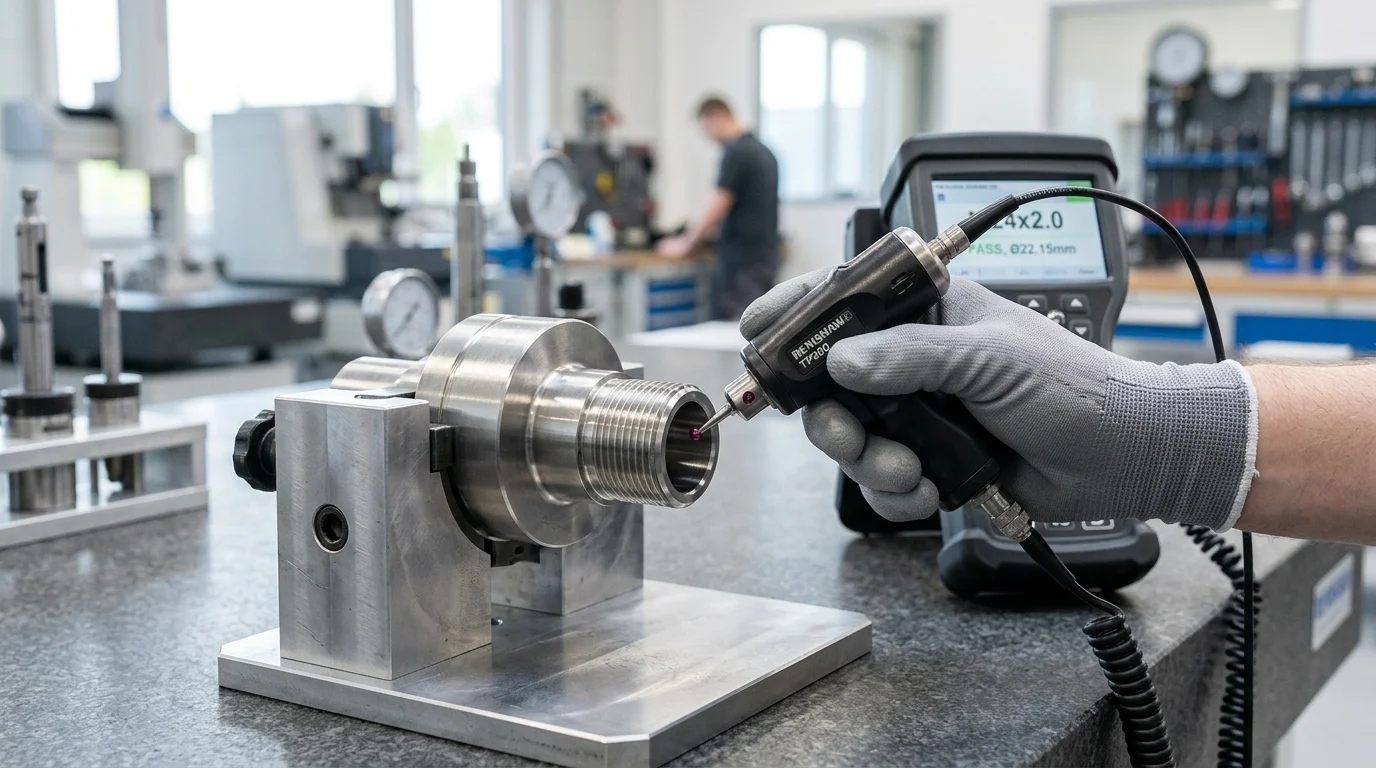
A single bad thread can turn an otherwise finished CNC component into scrap, especially when it is discovered after forging, stamping, turning, and finishing work are already complete. For manufacturers producing thousands of hardware parts per shift, the difference between manual “gauge feel” and measurable thread data can directly affect cost, throughput, and customer confidence. Automated thread inspection brings optics, lasers, and tactile probes into the quality process to capture pitch diameter, flank angle, root radius, and other critical features with repeatable precision. This article explains where automated systems outperform manual gauging, which defects matter most, and how inspection choices influence accuracy in high-volume hardware production.
How Thread Inspection Technology Improves CNC Accuracy
Threading is often one of the final operations performed on a machined blank. If a part is scrapped due to a defective thread at this late stage, all prior forging, stamping, and turning time—and the associated costs—are entirely lost. For facilities producing thousands of hardware pieces per shift, holding tight tolerances on threaded parts is a daily challenge that requires both speed and reliable precision. Integrating automated Thread Inspection technology shifts quality control away from subjective manual gauging and toward quantifiable, actionable data, directly reducing late-stage scrap costs.
What automated thread inspection means
Upgrading to automated inspection means transitioning from traditional Go/No-Go ring and plug gauges—governed by ASME B1.2 or ISO 1502 standards—to high-speed optics, lasers, or tactile probes. While manual gauging typically requires 15 to 20 seconds per part to yield a binary pass or fail, automated systems digitize the entire thread profile in a fraction of the time.
A modern optical system can typically complete a 360-degree scan in approximately 1.5 to 3.0 seconds, depending on part complexity. This technology captures the true geometry of the thread, providing a digital twin of the machined cut. By removing the physical friction of manual gauging, facilities eliminate wear on inspection tools, helping baseline measurements remain consistent over thousands of cycles.
Which thread defects matter most
Not all threading errors are created equal. When machining Precision Parts from tough materials like AISI 1045 (medium-carbon steel), ASTM A36 structural steel, or other high-carbon alloys, tool wear occurs aggressively. The defects that require the most monitoring are pitch diameter variations, root radii anomalies, and flank angle errors.
For example, a pitch diameter deviation as small as 0.025 mm might pass unnoticed on a manual gauge depending on operator torque, yet it can cause uneven load distribution and premature failure in the final assembly. Automated systems identify these micro-deviations consistently. They map the exact root radius to ensure there are no stress concentrators that could lead to metal fatigue, identifying issues before tool wear results in non-conforming parts.
Where Automated Inspection Outperforms Manual Gauging
Quality managers recognize that human variability impacts manufacturing consistency. "Gauge feel" varies among personnel and throughout a shift, meaning a part that passes inspection in the morning might fail later if a different operator applies more torque to the plug gauge. Automated inspection eliminates this subjectivity, providing a highly repeatable alternative to manual checks.
Vision systems vs contact measurement
When evaluating automated options, the primary choices are vision systems and contact measurement. Vision and laser systems are well-suited for high-volume external threads, whereas tactile contact probes are generally required for inspecting deep internal threads where cameras lack a clear line of sight. Optical systems face specific limitations: they can struggle with very fine thread pitches, high depth-to-diameter ratios, highly reflective surface finishes, or excessively oily parts. These conditions often dictate whether non-contact inspection is feasible, sometimes requiring dedicated part-cleaning stations prior to inspection.
| Inspection Method | Speed Per Part | Data Output | Best Application |
|---|---|---|---|
| Vision/Optical Systems | 1.5–3.0 seconds | Full 3D geometric profile | High-volume external threads |
| Contact (Tactile) Probes | 15.0–25.0 seconds | Specific coordinate data | Deep internal threads, complex geometries |
| Manual (Go/No-Go) | 10.0–30.0 seconds* | Pass/Fail binary only | Low-volume spot checks |
*Note: Manual gauging speeds vary widely; simple external threads may take 10 seconds, while complex or deep internal threads can take up to 30 seconds.
For most Hardware Components produced at scale, non-contact optical systems are preferred due to their high throughput. They bypass gauge wear, maintaining consistent accuracy across batches. However, manual ring and plug gauges remain necessary for certain industry-standard compliance checks or low-volume spot testing.
Process data to track across CNC machining
The primary advantage of this technology is realized when connecting high-speed inspection data back to CNC Machining centers. Manual gauging provides a binary pass or fail, which acts as a lagging indicator; by the time a part fails, the machine has likely already produced several non-conforming parts.
Automated systems feed continuous Statistical Process Control (SPC) data directly to the network. Facilities can track their Process Capability Index (Cpk) in real-time, generally aiming to keep it above 1.33 for critical thread dimensions. As an illustrative example, if the pitch diameter shows a hypothetical upward trend of 0.005 mm per batch due to insert wear, the software flags it. While achieving real-time SPC feedback and automatic tool offsets requires significant integration effort—including MTConnect or OPC-UA connectivity, validated macros, and programmer oversight—this infrastructure allows the CNC controller to correct drift before parts fall out of specification.
How to Choose and Implement Thread Inspection Technology
Transitioning from theoretical benefits to practical application requires careful planning to avoid disrupting existing production flow. Successful implementation requires operator buy-in, a clear understanding of the specific manufacturing environment, and an acknowledgment of capital expenses, floor-space constraints, and ongoing calibration requirements.
Facilities cannot simply install a vision system next to a lathe and expect immediate Tolerance control. Shop floors are oily, vibrating, and subject to temperature swings and shifting ambient light. These factors can interfere with delicate optics, causing false rejects due to coolant residue on parts or calibration drift from machine vibrations if the deployment is not planned correctly.
Steps for integrating automated thread inspection
The first step in integration is assessing production volume and deciding between an inline or offline setup. For high-speed runs on standard cold heading machines, facilities often prefer near-line automated stations. Using multi-part fixtures or parallel scanning stations, operators can drop a sample batch into a tray, allowing the system to inspect up to 50 parts in under a minute.
Next, facilities must establish a strict calibration routine using certified master gauges to ensure the automated system maintains its accuracy over time and mitigates calibration drift.
Key Takeaways
- Use automated thread inspection to reduce late-stage scrap because threading is often performed after forging, stamping, and turning costs are already committed.
- Replace subjective Go/No-Go gauge checks with digital optical, laser, or tactile measurement when high-volume CNC hardware requires repeatable thread data.
- Consider optical inspection for fast external-thread checks, since modern systems can scan a full 360-degree profile in roughly 1.5 to 3.0 seconds.
- Monitor pitch diameter, root radius, and flank angle closely because small errors can affect load distribution, fatigue resistance, and final assembly reliability.
- Account for part condition before choosing vision inspection, since fine pitches, reflective finishes, oily surfaces, and deep internal threads can limit non-contact measurement.
Frequently Asked Questions
What is automated thread inspection?
Automated thread inspection uses optical, laser, or tactile systems to measure thread geometry digitally instead of relying only on manual Go/No-Go gauges.
Why is thread inspection critical for CNC hardware components?
Threading is often one of the final machining steps, so a defective thread can scrap a part after forging, stamping, turning, and other costs are already invested.
How fast is automated thread inspection compared with manual gauging?
Manual gauging often takes 15 to 20 seconds per part, while modern optical systems can complete a 360-degree scan in about 1.5 to 3.0 seconds.
Which thread defects should manufacturers monitor most closely?
Key defects include pitch diameter variation, root radius anomalies, and flank angle errors, especially when machining tough steels or high-carbon alloys.
Can automated systems detect defects manual gauges may miss?
Yes. For example, a pitch diameter deviation as small as 0.025 mm may be affected by operator gauge feel, while automated systems measure it consistently.