


In our twelve years of manufacturing conversion joints and thread adapters, I have watched the same mistake cost buyers thousands of dollars in returned shipments and lost production time. The mistake is always the same: a procurement order placed for the wrong spindle thread standard. Because M14 and 5/8-11 differ by only 1.875mm in diameter but use entirely different thread geometry (metric coarse versus unified national coarse), the parts look interchangeable until installation. That is the moment the buyer learns they purchased accessories that physically cannot attach to their grinders.
At Guling Hardware we ship approximately 12 million conversion joints and thread adapters per year through our 40-machine facility in Yuyao. Because we see the failure mode from both sides (the buyer who ordered wrong and the operator who tried to force the fit), we built our entire specification service around the same decision chart this article presents. I will walk you through the three dominant thread standards, the ANSI and ISO specifications that govern them, the regional distribution patterns that drive inventory decisions, and the selection matrix I use with our OEM partners when they specify a new program.
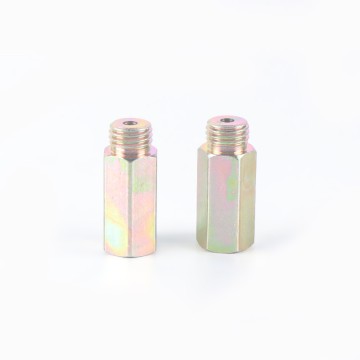
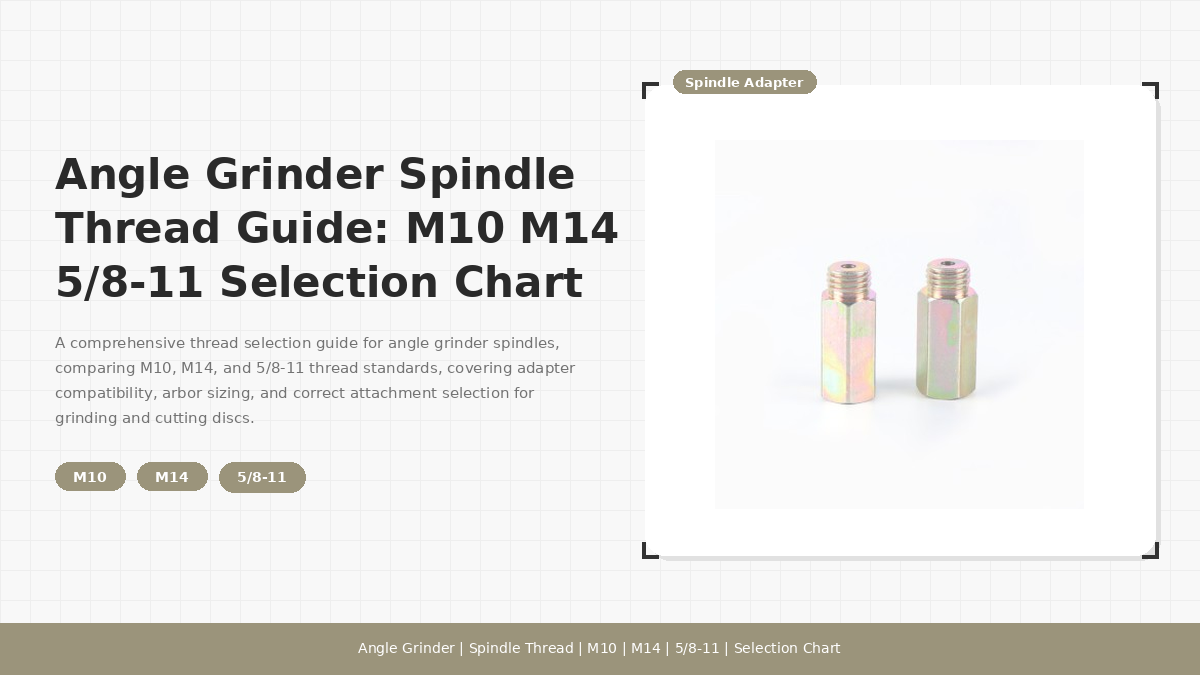
Guling Hardware conversion joints in production. Because we ship millions of these annually, we see the full cross-section of thread compatibility questions from buyers in 60+ countries. (Image: Guling Hardware)
The Five Numbers Every Procurement Manager Should Memorize
| Thread Standard | Major Diameter | Pitch | Primary Region | Approximate Market Share |
|---|---|---|---|---|
| M10 x 1.25 | 10.000mm (0.394") | 1.25mm | Europe, East Asia, China domestic | ~15% (compact grinders only) |
| M14 x 2.0 | 14.000mm (0.551") | 2.000mm | Europe, Asia, International | ~85% (global default) |
| 5/8"-11 UNC | 15.875mm (0.625") | 2.309mm (11 TPI) | North America | ~70% of NA market |
These numbers come directly from our shipping records at Guling Hardware: 85% of our conversion joints now use the M14 thread, because most of our European and Asian OEM partners standardize on M14 for the accessory ecosystem. Because the M14 standard is the most widely accepted globally, we recommend it as the default thread specification for any new product development unless the target market dictates otherwise.
The Three Thread Standards: Geometry, Standards, and Field Performance
M14 x 2.0 (ISO Metric Coarse, ISO 261)
The M14 thread is the international default for medium-to-large grinder spindles. We hold our M14 adapters to ISO 965-2 tolerance class 6g/6H, the standard specified by ISO 261. Our adapters mate correctly with components from any compliant manufacturer worldwide, including Bosch, Makita, Metabo, DeWalt, and Milwaukee.
Why M14 dominates the global market: Because the ISO metric thread standard is harmonized across more than 100 countries per the ISO 261 official standard reference, M14 adapters manufactured under ISO 261 specifications are interchangeable worldwide. Because the M14 coarse pitch provides adequate thread engagement for torque loads up to 73 N-m (compared to 25 N-m for M10), it handles the 900W to 2500W grinder range that represents the majority of industrial and professional applications. Because accessory manufacturers worldwide prioritize M14 as the default thread, the M14 ecosystem is the deepest in the industry.
M14 Technical Profile
- Nominal diameter: 14.000mm (0.551")
- Pitch: 2.000mm (ISO 261 coarse)
- Thread class: ISO 965-2 6g/6H
- Typical power range: 900W to 2500W
- Common disc bore: 22.23mm (7/8")
M10 x 1.25 (ISO Metric Fine Pitch, ISO 261)
The M10 thread appears on compact grinders in the 500W to 850W range. Because the 1.25mm fine pitch provides smoother engagement, M10 is preferred for frequent disc changes but is mechanically weaker under high torque loads. We have seen premature failures where M10 spindles stripped under loads that M14 would have handled comfortably.
M10 Technical Profile
- Nominal diameter: 10.000mm (0.394")
- Pitch: 1.250mm
- Thread class: ISO 965-2 6g/6H
- Load limit: 25 N-m
5/8"-11 UNC (ANSI B1.1 Unified National Coarse)
The 5/8"-11 thread is the North American standard per ANSI B1.1 (UNC). Because the US, Canada, and Mexico share the ANSI B1.1 standard, 5/8"-11 is the default on every major US grinder brand.
Because 5/8"-11 uses imperial thread geometry (11 threads per inch rather than metric pitch), the spindle is fundamentally incompatible with metric M14 or M10 accessories.
5/8"-11 Technical Profile
- Nominal diameter: 15.875mm (0.625")
- Pitch: 2.309mm (11 TPI)
- Thread class: ASME B1.1 2A/2B
- Common disc bore: 7/8" (22.23mm)
Regional Distribution: Where Each Standard Dominates
In twelve years of exporting to 60+ countries, I have observed consistent regional patterns.
| Region | Primary Thread | Secondary Thread | Market Character |
|---|---|---|---|
| China (domestic) | M10 (small), M14 (large) | None | Domestic industrial and export |
| Western Europe | M14 | 5/8"-11 (imported US equipment) | ISO standard, CE marking |
| Eastern Europe | M14 | M10 (smaller models) | ISO standard, industrial |
| United States | 5/8"-11 | M14 (European equipment) | ANSI/Imperial standard |
| Canada/Mexico | 5/8"-11 | M14 (imported equipment) | ANSI/Imperial standard, USMCA |
| Japan/Korea | M10 (small), M14 (large) | None | JIS/ISO hybrid standard |
| Southeast Asia | M14 | 5/8"-11 (US equipment) | ISO standard, import-dependent |
| Australia/NZ | M14 | 5/8"-11 (US equipment) | ISO standard, mixed market |
| Middle East | M14 | 5/8"-11 (imported US equipment) | ISO standard, import-dependent |
| South America | M14 | 5/8"-11 (US equipment) | ISO standard, mixed market |
| Africa (Sub-Saharan) | M14 | 5/8"-11 (mining sector) | ISO standard, import-dependent |
Because the regional distribution skews heavily toward M14 globally, I recommend distributors maintain M14 as primary inventory. M14 covers more than 80% of the global market.
For multi-region distributors, I recommend M14 as 70% stock and 5/8"-11 as 30%.
Selection Matrix: Thread to Grinder Compatibility
Matching a spindle thread to a grinder class is a binary decision, but matching the right thread to the right application involves additional variables. Because the consequences of getting this wrong include disc ejection at speed (which destroys equipment and risks operator injury), I always walk OEM partners through the same selection matrix below.
| Grinder Class | Disc Diameter | Power Range | Standard Thread | Typical RPM |
|---|---|---|---|---|
| Compact | 100mm to 115mm (4") | 500W to 850W | M10 x 1.25 | 11,000 |
| Standard | 115mm to 125mm (4.5" to 5") | 800W to 1200W | M14 x 2.0 | 11,000 to 12,000 |
| Mid-range | 150mm (6") | 1200W to 1500W | M14 x 2.0 | 10,000 |
| Large | 180mm to 230mm (7" to 9") | 1500W to 3000W+ | M14 x 2.0 or 5/8"-11 | 6,500 to 8,000 |
Thread Selection Decision Tree
Because this decision tree covers more than 95% of our specification requests, it is the standard reference for our OEM team. I recommend verifying the specific grinder model number before placing the production order.
Thread Geometry: The Engineering Details That Matter
Because procurement teams often focus on diameter and overlook pitch, the thread geometry table below is the first reference I provide to OEM engineering teams.
| Parameter | M10 x 1.25 | M14 x 2.0 | 5/8"-11 UNC |
|---|---|---|---|
| Major diameter | 10.000mm | 14.000mm | 15.875mm |
| Pitch | 1.250mm | 2.000mm | 2.309mm (11 TPI) |
| Thread height (theoretical) | 0.677mm | 1.083mm | 1.207mm |
| Tensile stress area | 64.5 mm2 | 115 mm2 | 156 mm2 |
| Standard torque (grade 8.8) | 25 N-m | 73 N-m | 120 N-m |
| Thread engagement (recommended) | 10mm to 12mm | 12mm to 15mm | 15mm to 18mm |
| Thread class reference | ISO 965-2 6H/6g | ISO 965-2 6H/6g | ASME B1.1 2A/2B |
Because thread engagement is underestimated, I require 1.5x the minimum. Insufficient engagement causes thread stripping under load (documented in the 5/8-11 UNC thread dimension standard).
Adapter Solutions: When Thread Conversion Becomes Necessary
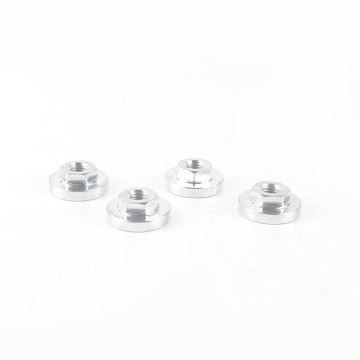
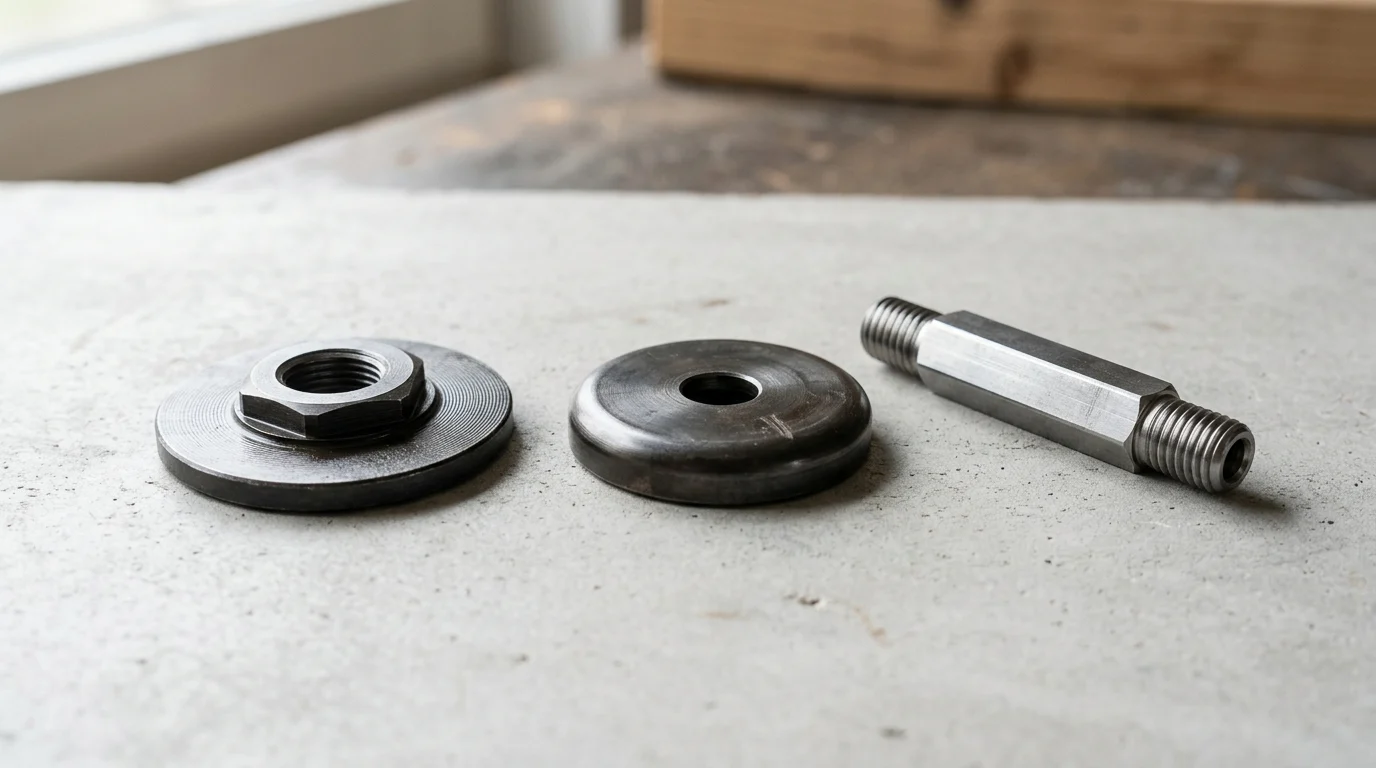
Hexagonal pressure plates with M10 and M14 thread variants from Guling Hardware. Because these plates interface directly with the spindle thread, the thread specification must match the grinder exactly. (Image: Guling Hardware)
Because thread adapters enable cross-standard compatibility, they are the practical solution for operations that run mixed grinder fleets. Because we ship more than 12 million adapters per year at Guling Hardware, I have learned that adapter selection involves more variables than diameter matching.
Engineering insight: Because thread adapters reduce effective torque capacity by 15% to 25% (the additional joint in the load path absorbs energy and concentrates stress), we recommend limiting adapter use to applications below 800W continuous duty. For continuous high-torque operation above 1000W, the correct approach is to standardize the fleet on a single thread rather than relying on adapters in every station.
Common Adapter Configurations
| Adapter Type | From Thread | To Thread | Typical Application |
|---|---|---|---|
| M14 to 5/8"-11 | 14mm x 2.0mm | 5/8"-11 UNC | European grinder using US accessories |
| 5/8"-11 to M14 | 5/8"-11 UNC | 14mm x 2.0mm | US grinder using European accessories |
| M10 to M14 | 10mm x 1.25mm | 14mm x 2.0mm | Compact grinder using standard accessories |
| M14 to M10 | 14mm x 2.0mm | 10mm x 1.25mm | Standard grinder using compact accessories |
Guling Hardware Thread Adapter Product Range
At Guling Hardware, we manufacture four primary adapter configurations in our 40-machine facility in Yuyao. Because we run both cold-heading presses and CNC turning machines, we can produce thread adapters in volume from M3 to M24 metric and from 4-40 UNC to 3/4-10 imperial.
| Product | Adapter Type | Material | Heat Treatment |
|---|---|---|---|
| M14 to 5/8"-11 Adapter | Imperial conversion | 45# Steel | Quenched and tempered |
| 5/8"-11 to M14 Adapter | Metric conversion | 45# Steel | Quenched and tempered |
| M10 to M14 Adapter | Upsize conversion | 40Cr Steel | Quenched only |
| M14 to M10 Adapter | Downsize conversion | 45# Steel | Quenched and tempered |
All adapter threads are manufactured to ISO 965-2 6H/6g. Our 100% thread gauge inspection ensures every adapter meets ISO 261. Browse our complete angle grinder accessories catalog for the full range.
Selection Guide: Thread to Application
| Application | Recommended Thread | Field Rationale |
|---|---|---|
| Metal fabrication / welding | M14 x 2.0 | Widest accessory ecosystem |
| Stone/concrete cutting | M14 or 5/8"-11 | Depends on grinder origin |
| Precision / compact grinding | M10 x 1.25 | Fine pitch reduces vibration |
| Cut-off operations | M14 x 2.0 | Standard for industrial discs |
| Field repair / North America | 5/8"-11 | NA accessory availability |
| International export | M14 x 2.0 | Global default |
Safety Standards and Regulatory Compliance
Because angle grinder spindle threads are governed by multiple safety standards depending on the target market, procurement teams need to verify compliance against the standards applicable to their region. Because I have run enough CE and UL audits, I have listed the primary standards below.
| Standard | Scope |
|---|---|
| ISO 261:1998 | ISO general purpose metric screw threads |
| ISO 965-2:1998 | ISO metric screw thread tolerance limits |
| ANSI B1.1-2019 | Unified Inch Screw Threads (UNC, UNF) |
| IEC 62841-3-1:2024 | Safety of hand-held electric tools (grinders) |
| EN 62841-3-1:2010+A1:2015 | European safety standard for grinders |
Regional Compliance
| Market | Primary Standard | Thread Requirement |
|---|---|---|
| EU | EN 62841-3-1 | M14 or M10 |
| USA | UL 62841-3-1 | 5/8"-11 |
| China | GB 3883.3-2016 | M10/M14 |
| Japan | JIS C 7401-1-4 | M10/M14 |
| AU/NZ | AS/NZS 62841-3-1 | M14 or 5/8"-11 |
Cost Analysis: Thread Standard Impact on Procurement
Because thread standard selection affects BOM cost through the entire product lifecycle, I have included the cost factors below from our own production economics. Because these costs are based on actual production data at our 40-machine facility, they reflect the real-world cost structure rather than a theoretical comparison.
| Cost Factor | M10 x 1.25 | M14 x 2.0 | 5/8"-11 UNC |
|---|---|---|---|
| Raw material cost (relative) | Lowest | Medium | Highest |
| Thread cutting complexity | High (fine pitch) | Medium | Medium |
| Accessory availability (global) | Limited (compact only) | Excellent | Excellent (NA only) |
| Supply chain risk | Low (domestic) | Low (global) | Medium (regional) |
Strategy
- Domestic China: Default to M14. Use M10 only for compact grinders below 850W.
- International export: Default to M14 unless the customer specifies 5/8"-11 for North America.
- North America: Default to 5/8"-11 and provide M14 adapters as optional accessories.
- Multi-region distributors: Maintain M14 (70%) and 5/8"-11 (30%) inventory, adjusted for regional mix.
- OEM/ODM projects: Confirm thread specification at RFQ and verify against the actual production grinder before tooling release.
Conclusion: Thread Selection as a Strategic Decision
Because the angle grinder spindle thread determines accessory compatibility, regulatory compliance, and total cost of ownership, I encourage procurement teams to treat thread specification as a strategic decision rather than a procurement detail. Because we ship more than 12 million conversion joints and adapters per year at Guling Hardware, I have seen the full range of outcomes: well-specified projects that scale smoothly, and poorly-specified projects that consume engineering time on adapter workarounds.
The practical takeaway from our twelve years of manufacturing data: Because M14 is the global default for industrial and professional applications, because M14 is the cheapest to source at scale, and because M14 adapters carry the smallest quality risk in international shipping, I recommend M14 as the default thread for any new product development unless the target market dictates otherwise.
For procurement teams ready to expand an angle grinder program, our engineering team is available for thread selection and custom manufacturing consultation. Because we manufacture in volume from M3 to M24 metric and from 4-40 UNC to 3/4-10 imperial, we can support most OEM specifications without tooling changeover. Submit your specification for engineering review or browse our adapter catalog.
FAQs
A: No. M14 and 5/8"-11 are incompatible threads because M14 measures 14mm diameter with 2.0mm metric coarse pitch per ISO 261, while 5/8"-11 measures 15.875mm diameter with 11 threads per inch per ANSI B1.1. Because the diameter difference is only 1.875mm and the thread geometry is metric versus imperial, forced cross-threading will strip both the spindle and the accessory threads. We always recommend a properly rated adapter rather than any field-modification attempt.
A: M14 is the dominant standard across European grinder models, representing approximately 85% of EU market grinders based on our shipping data. M10 appears only on compact models at 115mm or less disc diameter, approximately 15% of the market. Because most operators standardize on one thread, M14 inventory dominates our production lines.
A: M14 x 2.0 is the standard coarse pitch defined in ISO 261 and used on virtually all angle grinder spindles. M14 x 1.5 is a fine pitch variant that appears only on specialized equipment such as some medical or laboratory devices. Because the 0.5mm pitch difference makes cross-threading inevitable, we have seen damaged spindles returned from operators who assumed any M14 would fit.
A: Three methods work reliably. Check the nameplate, use a pitch gauge, or measure with calipers. We recommend the pitch gauge or calipers because nameplates can be worn or painted over.
A: Thread adapters reduce torque capacity by 15% to 25%. Limit use to below 800W.
A: The thread standard does not determine maximum RPM. Always verify the disc rated RPM independently.
A: Yes. Our 40-machine facility runs cold-heading and CNC turning for thread sizes from M3 to M24 metric and from 4-40 UNC to 3/4-10 imperial. For OEM projects we typically need a 2D drawing and projected annual volume. We ship engineering samples within 7 working days.
A: We manufacture to ISO 965-2 6H/6g and ASME B1.1 2A/2B, the standard tolerance classes.